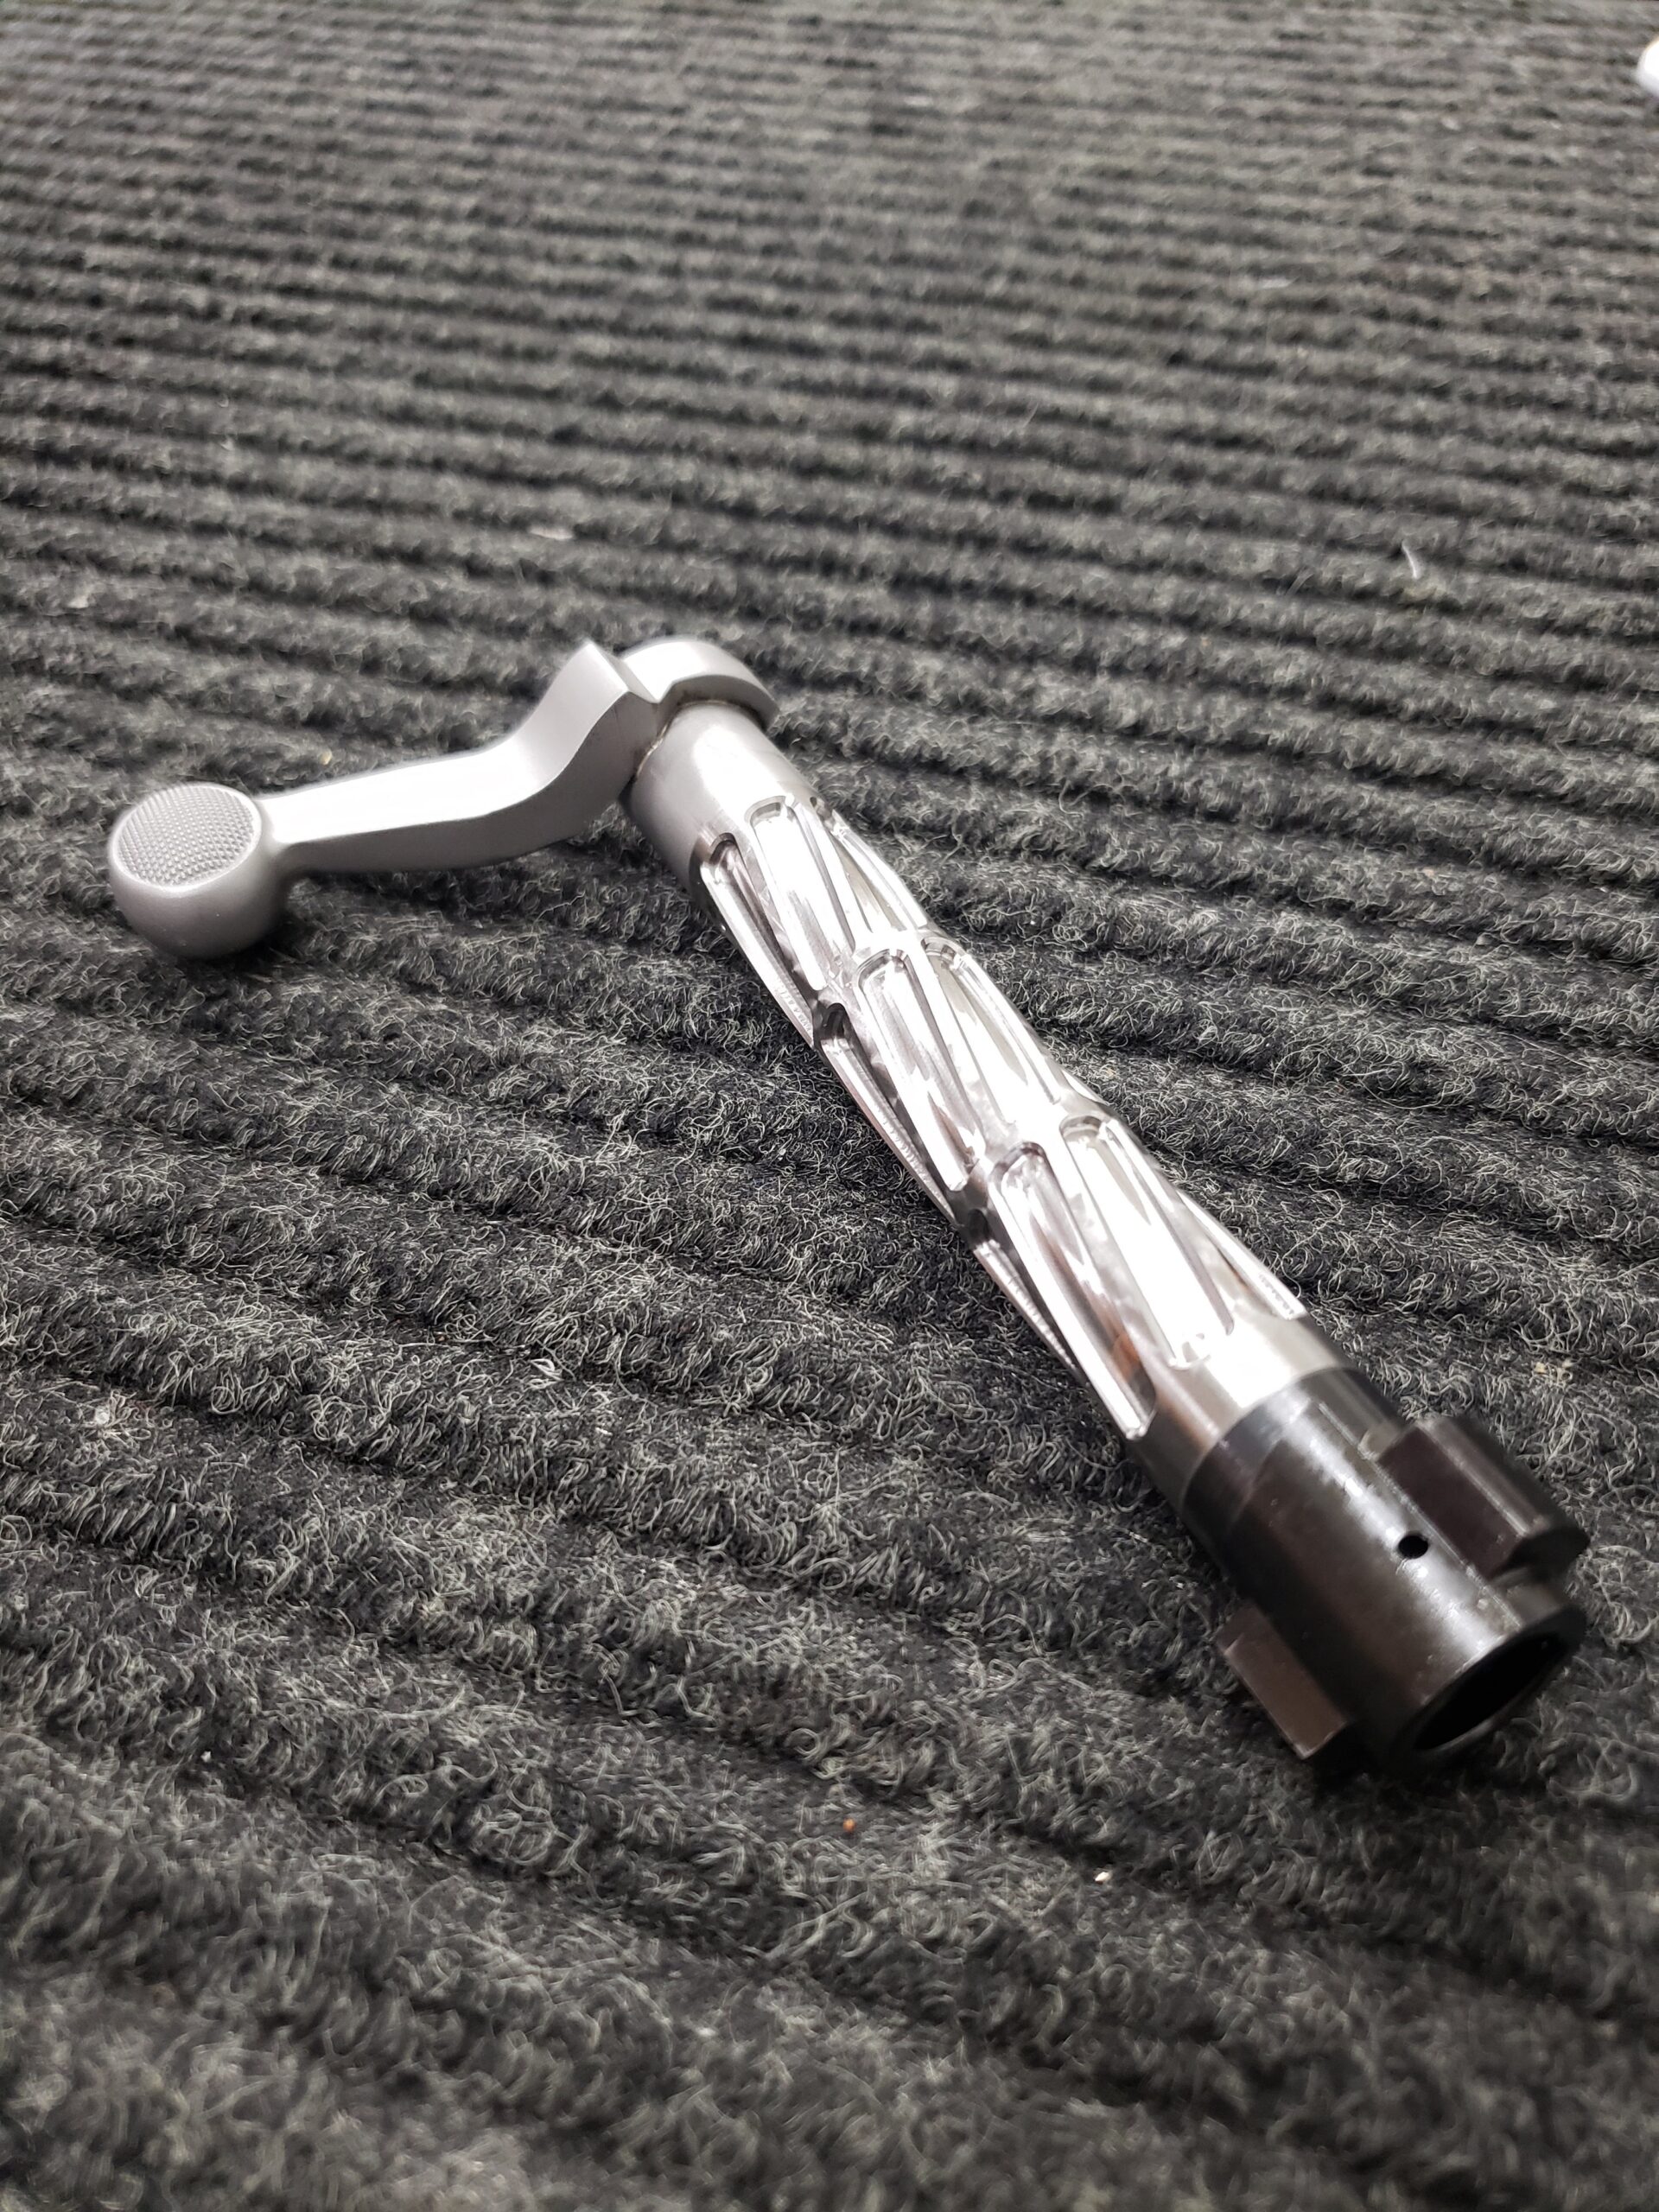
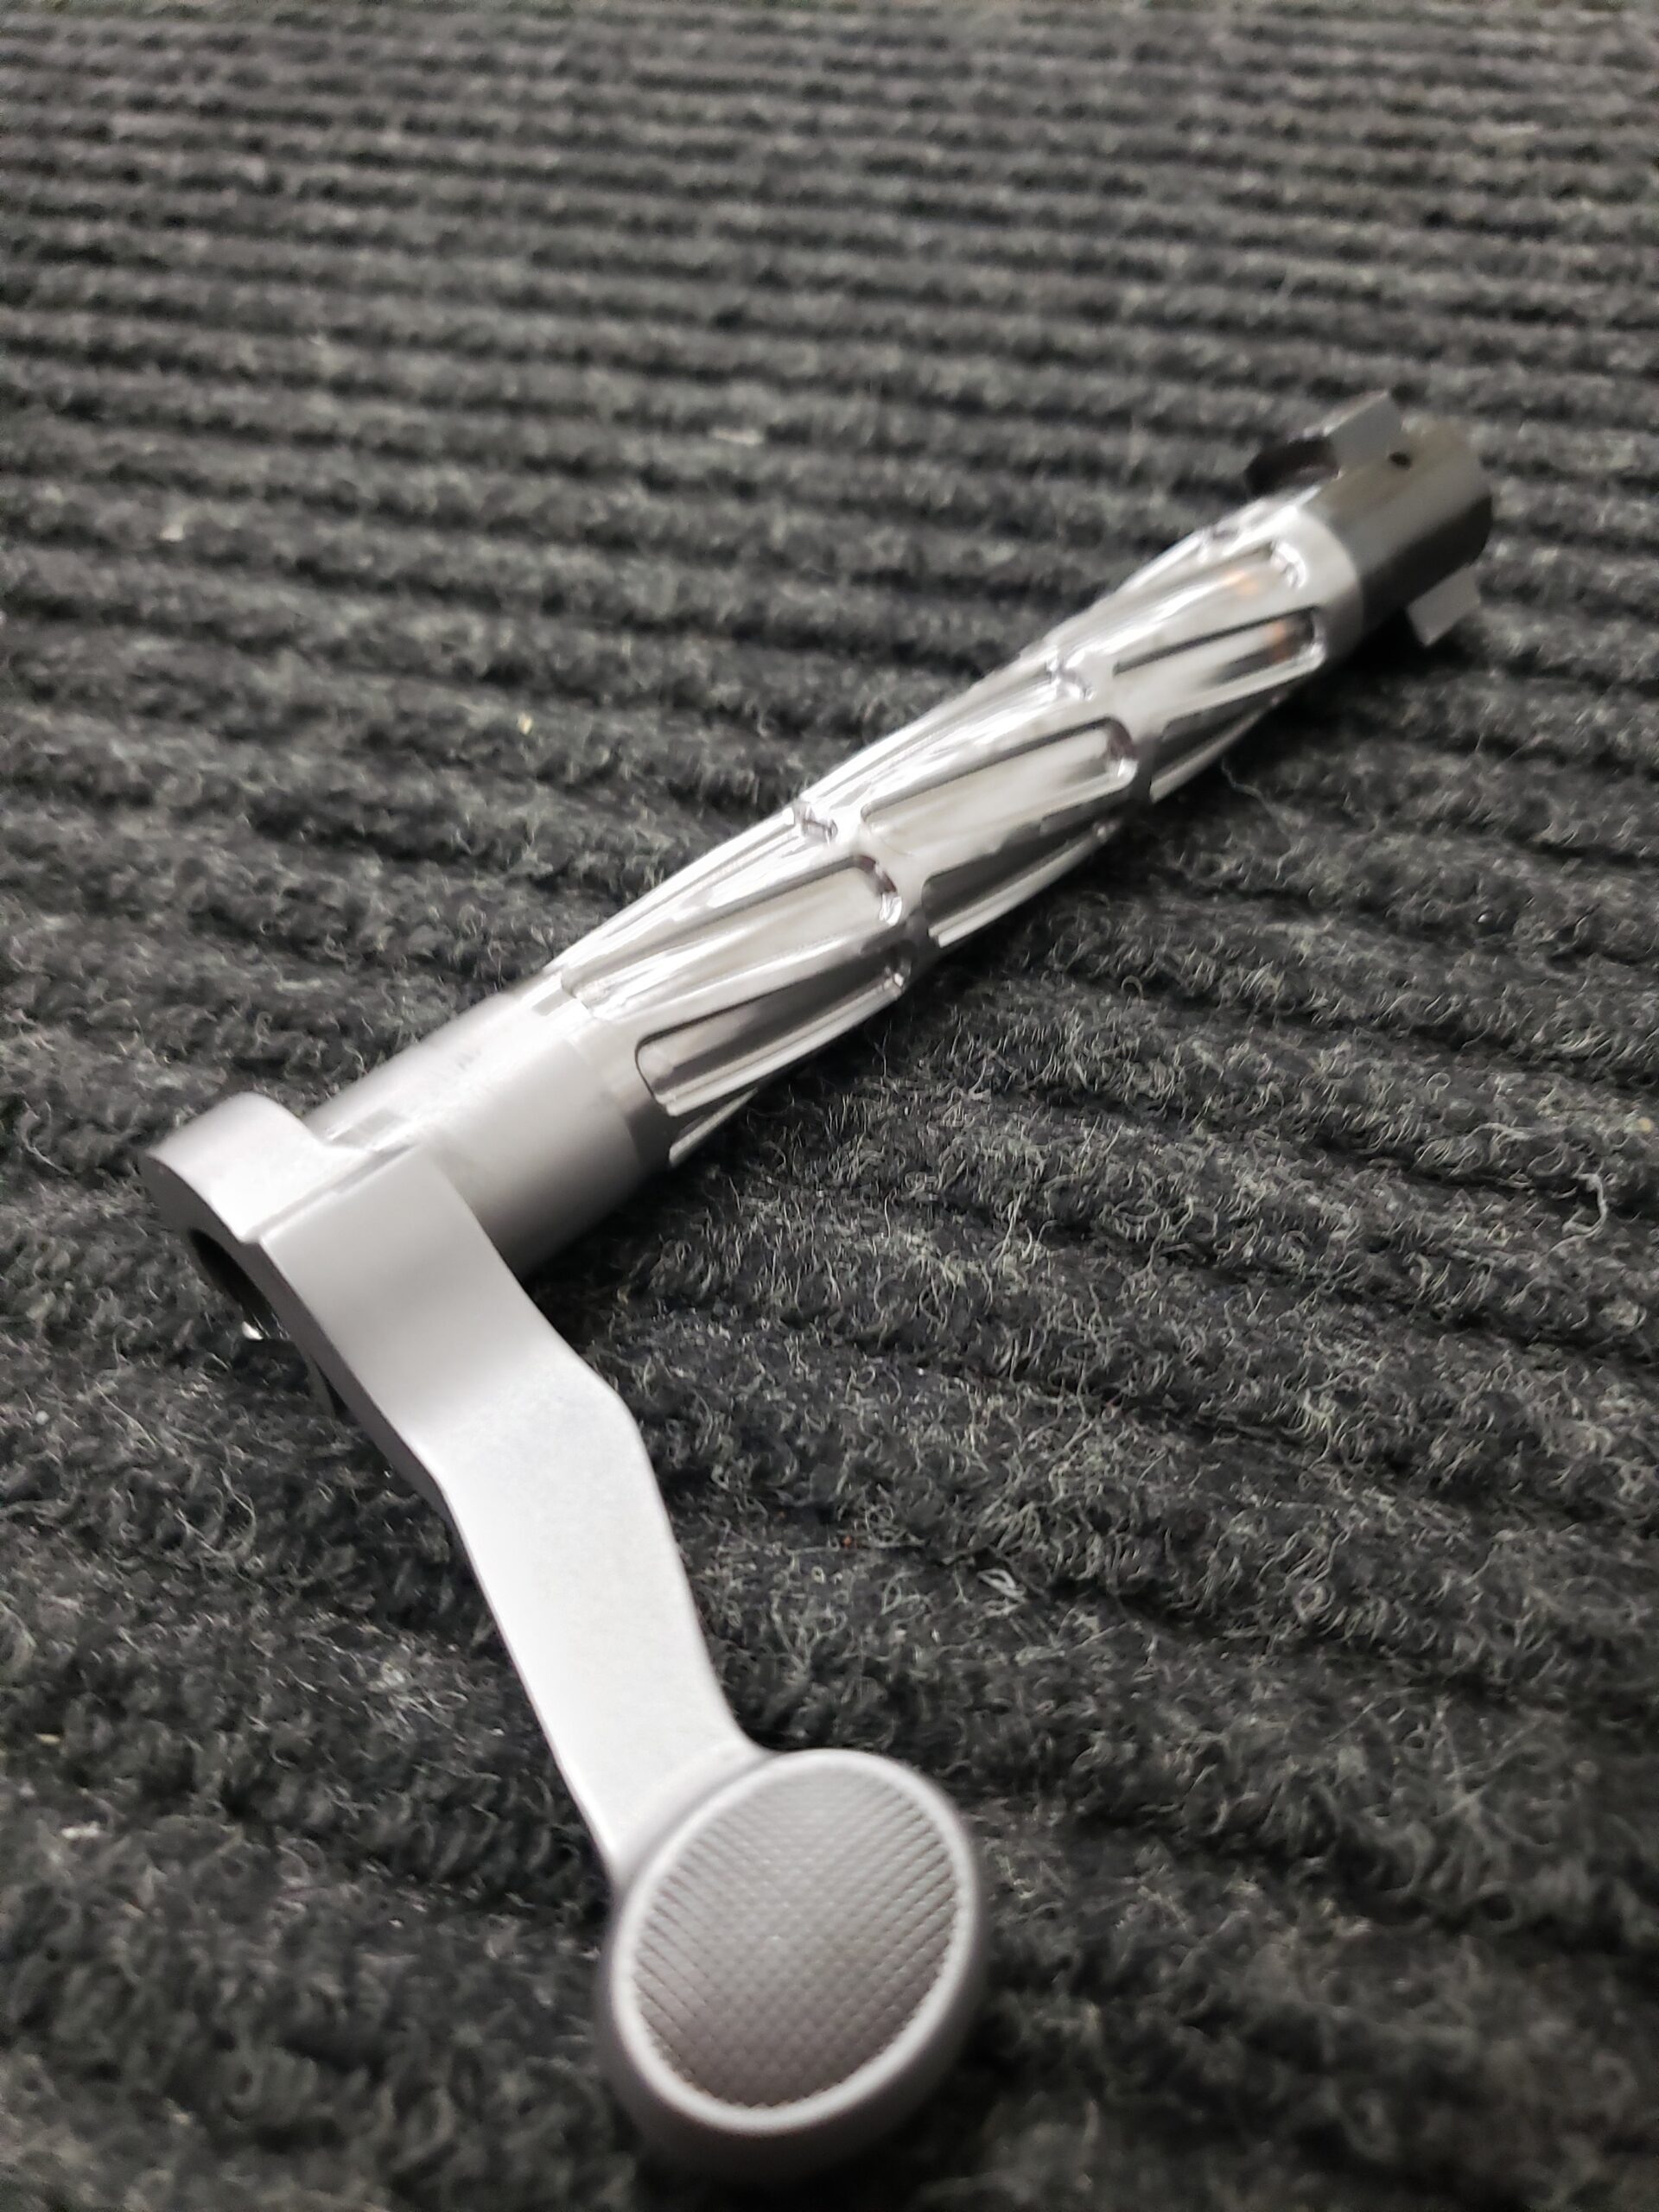
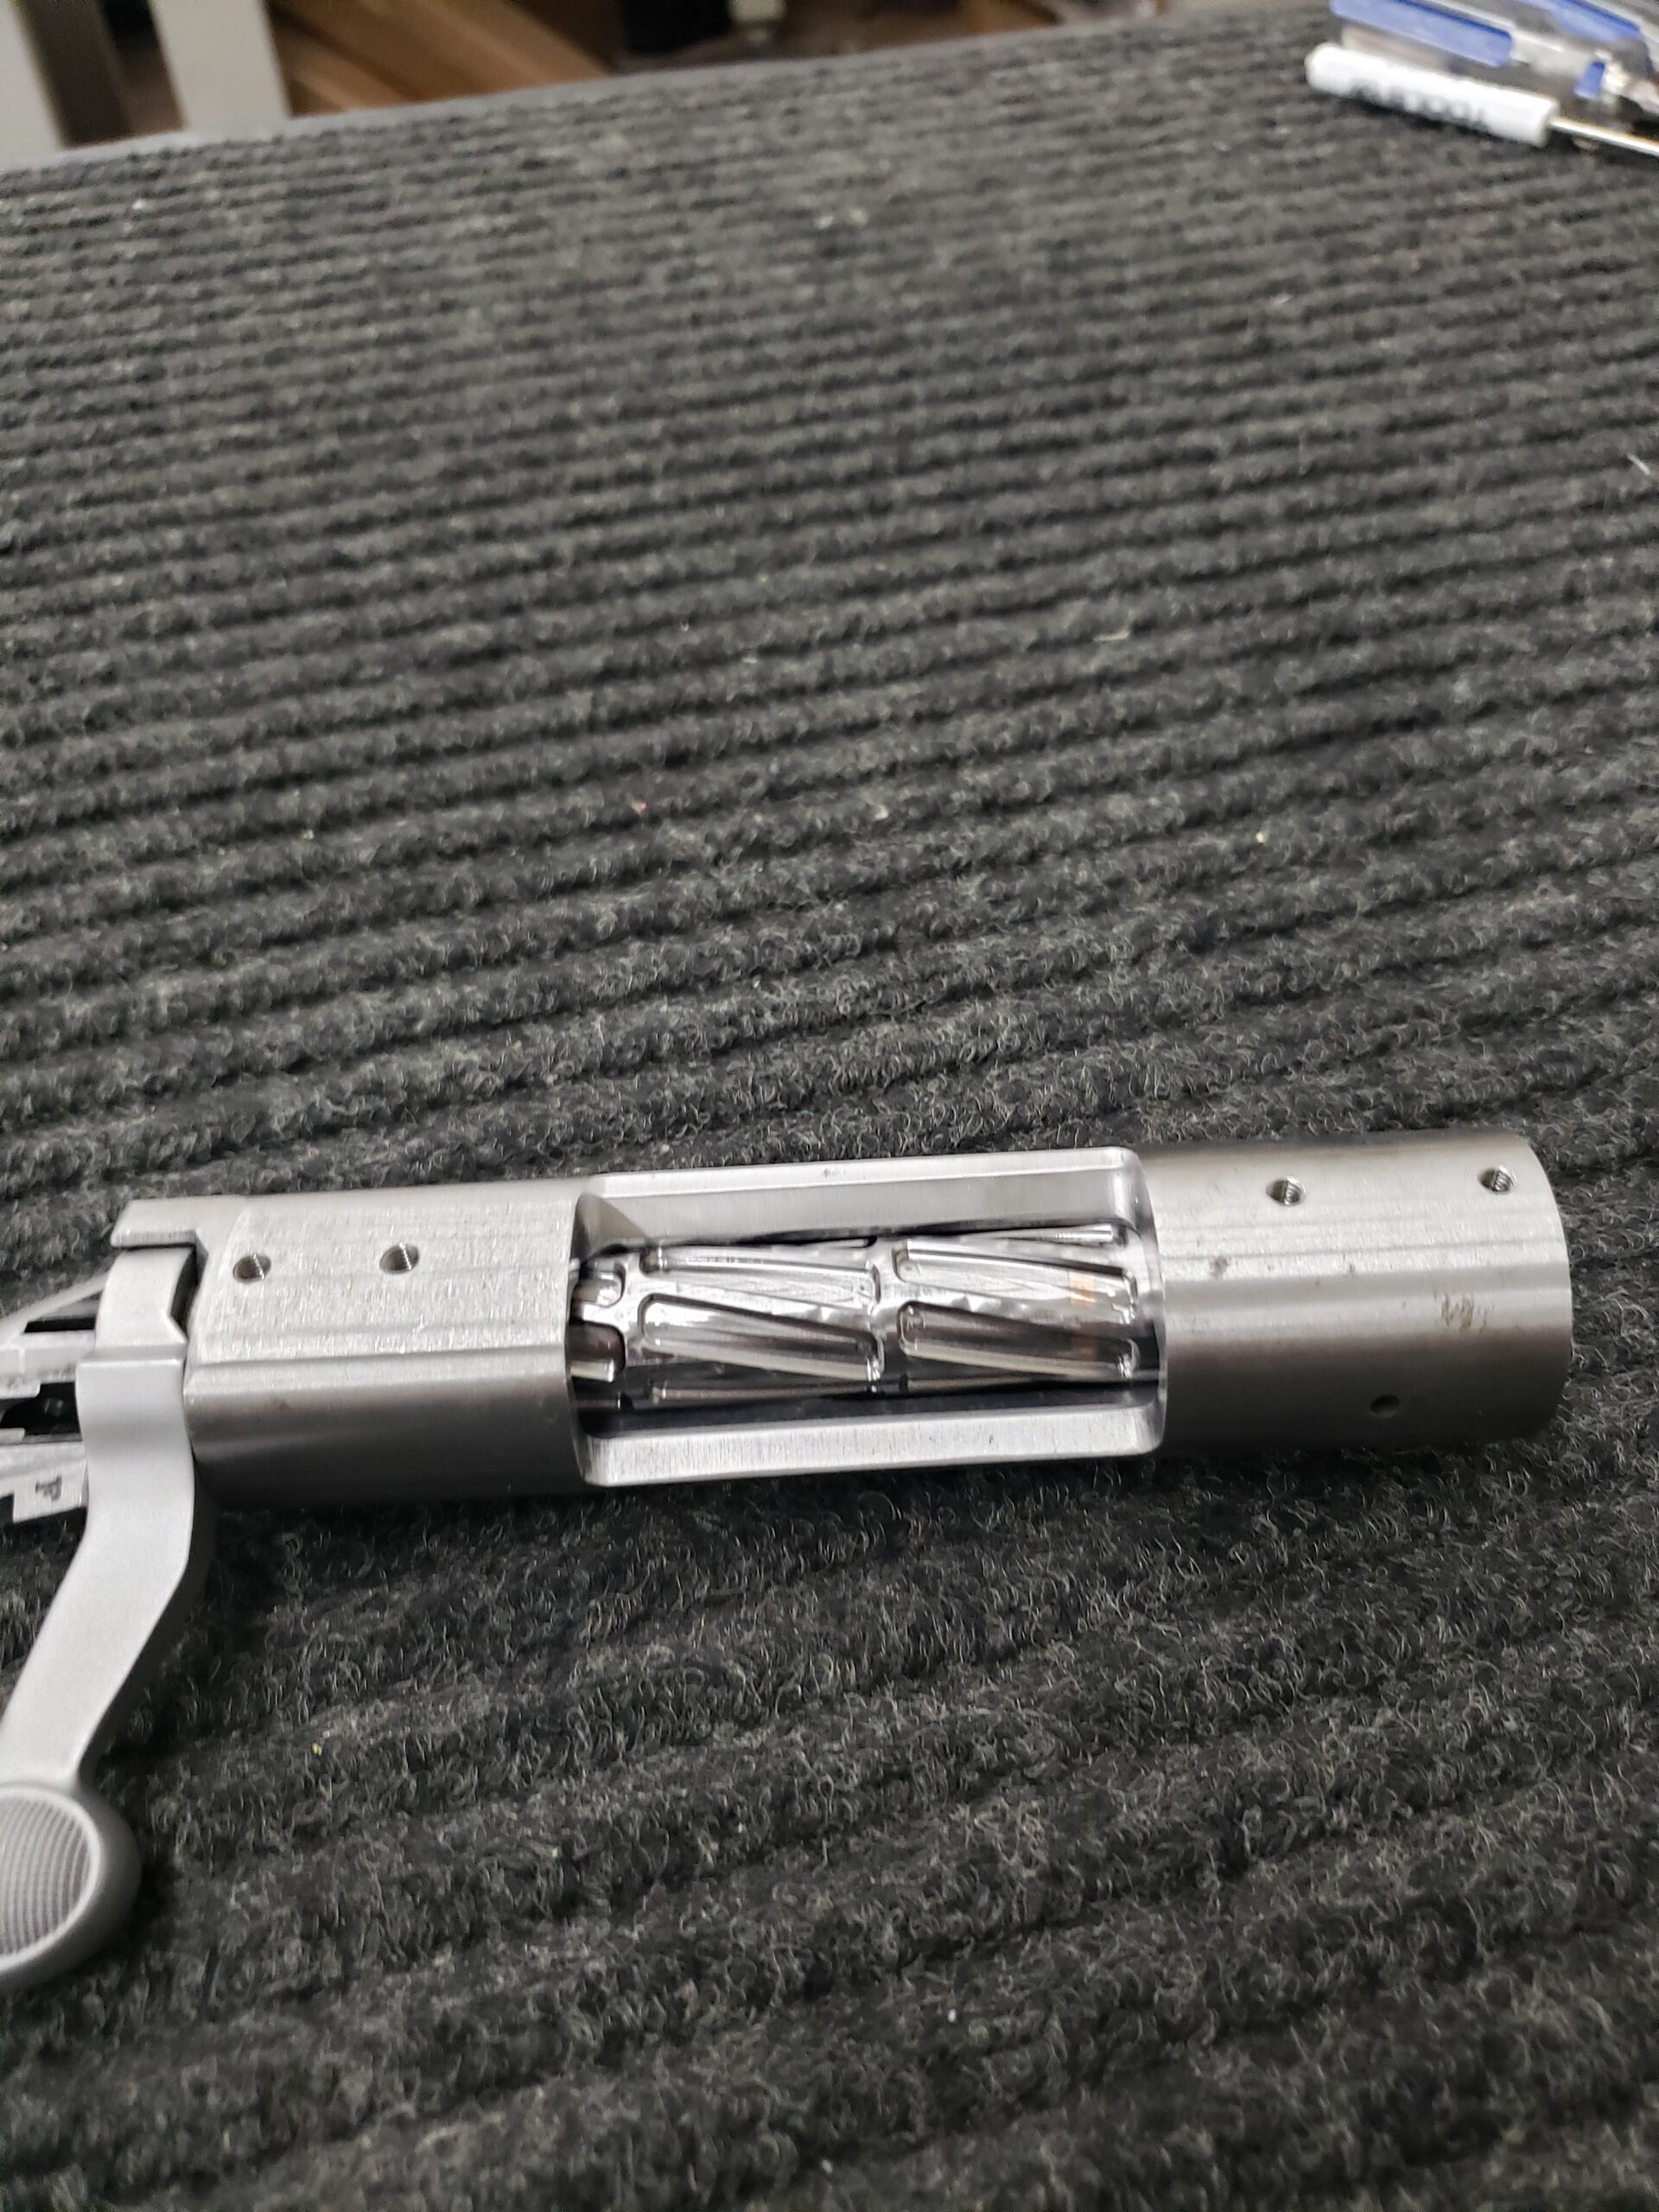
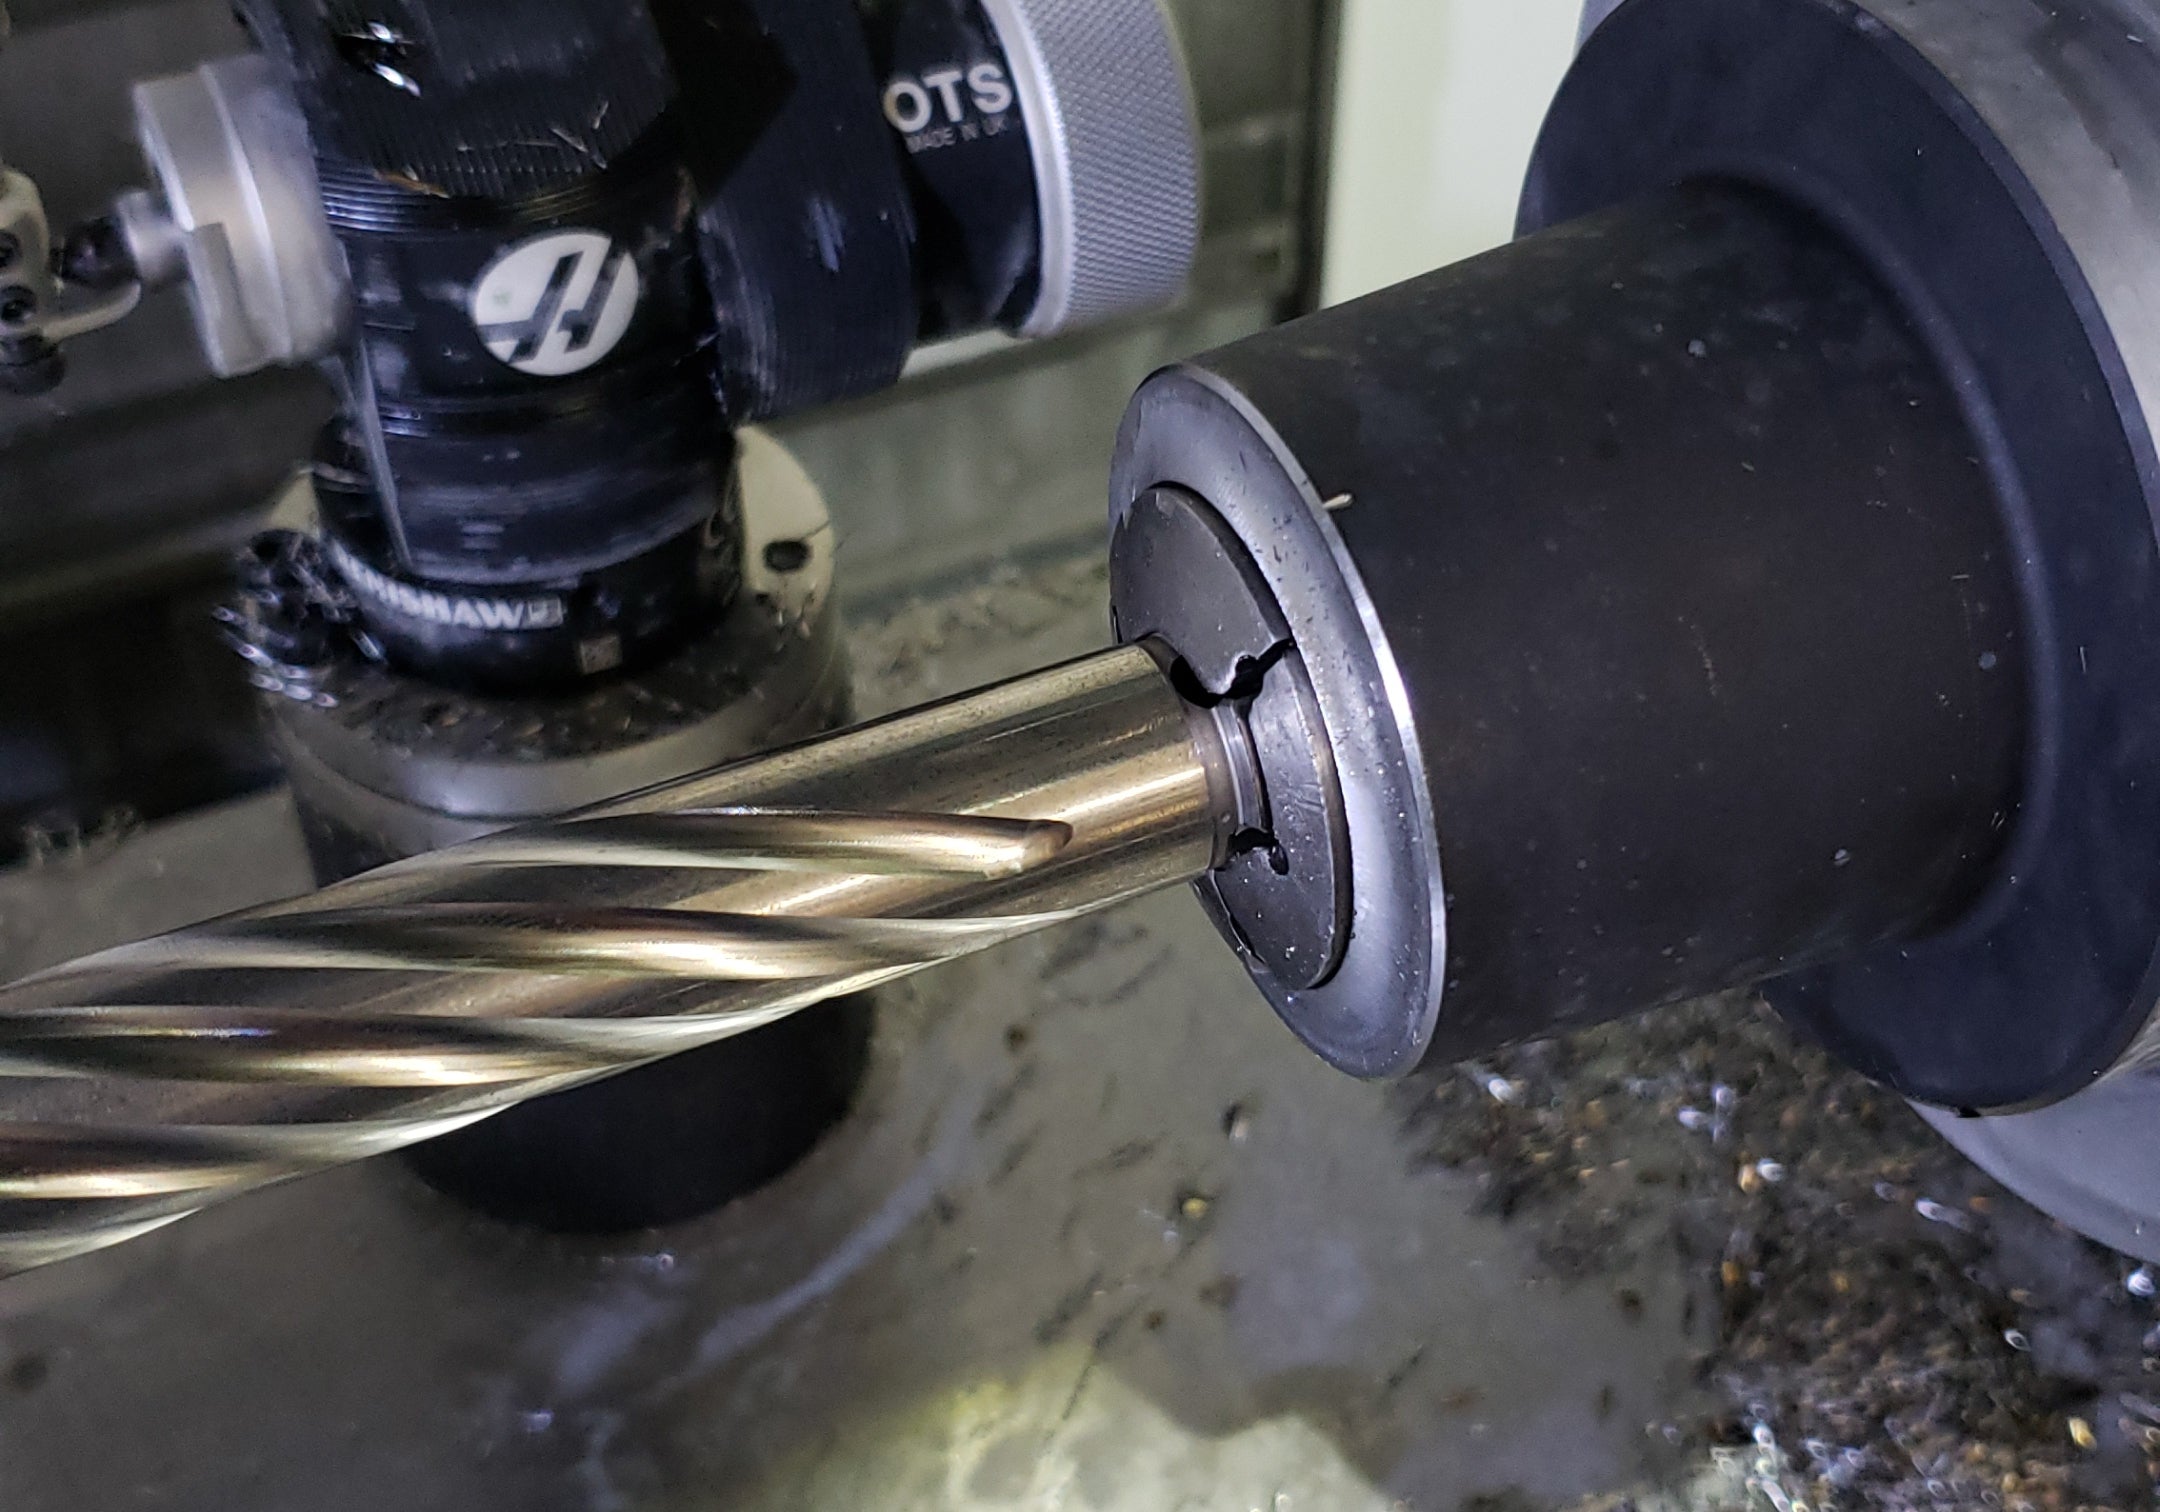
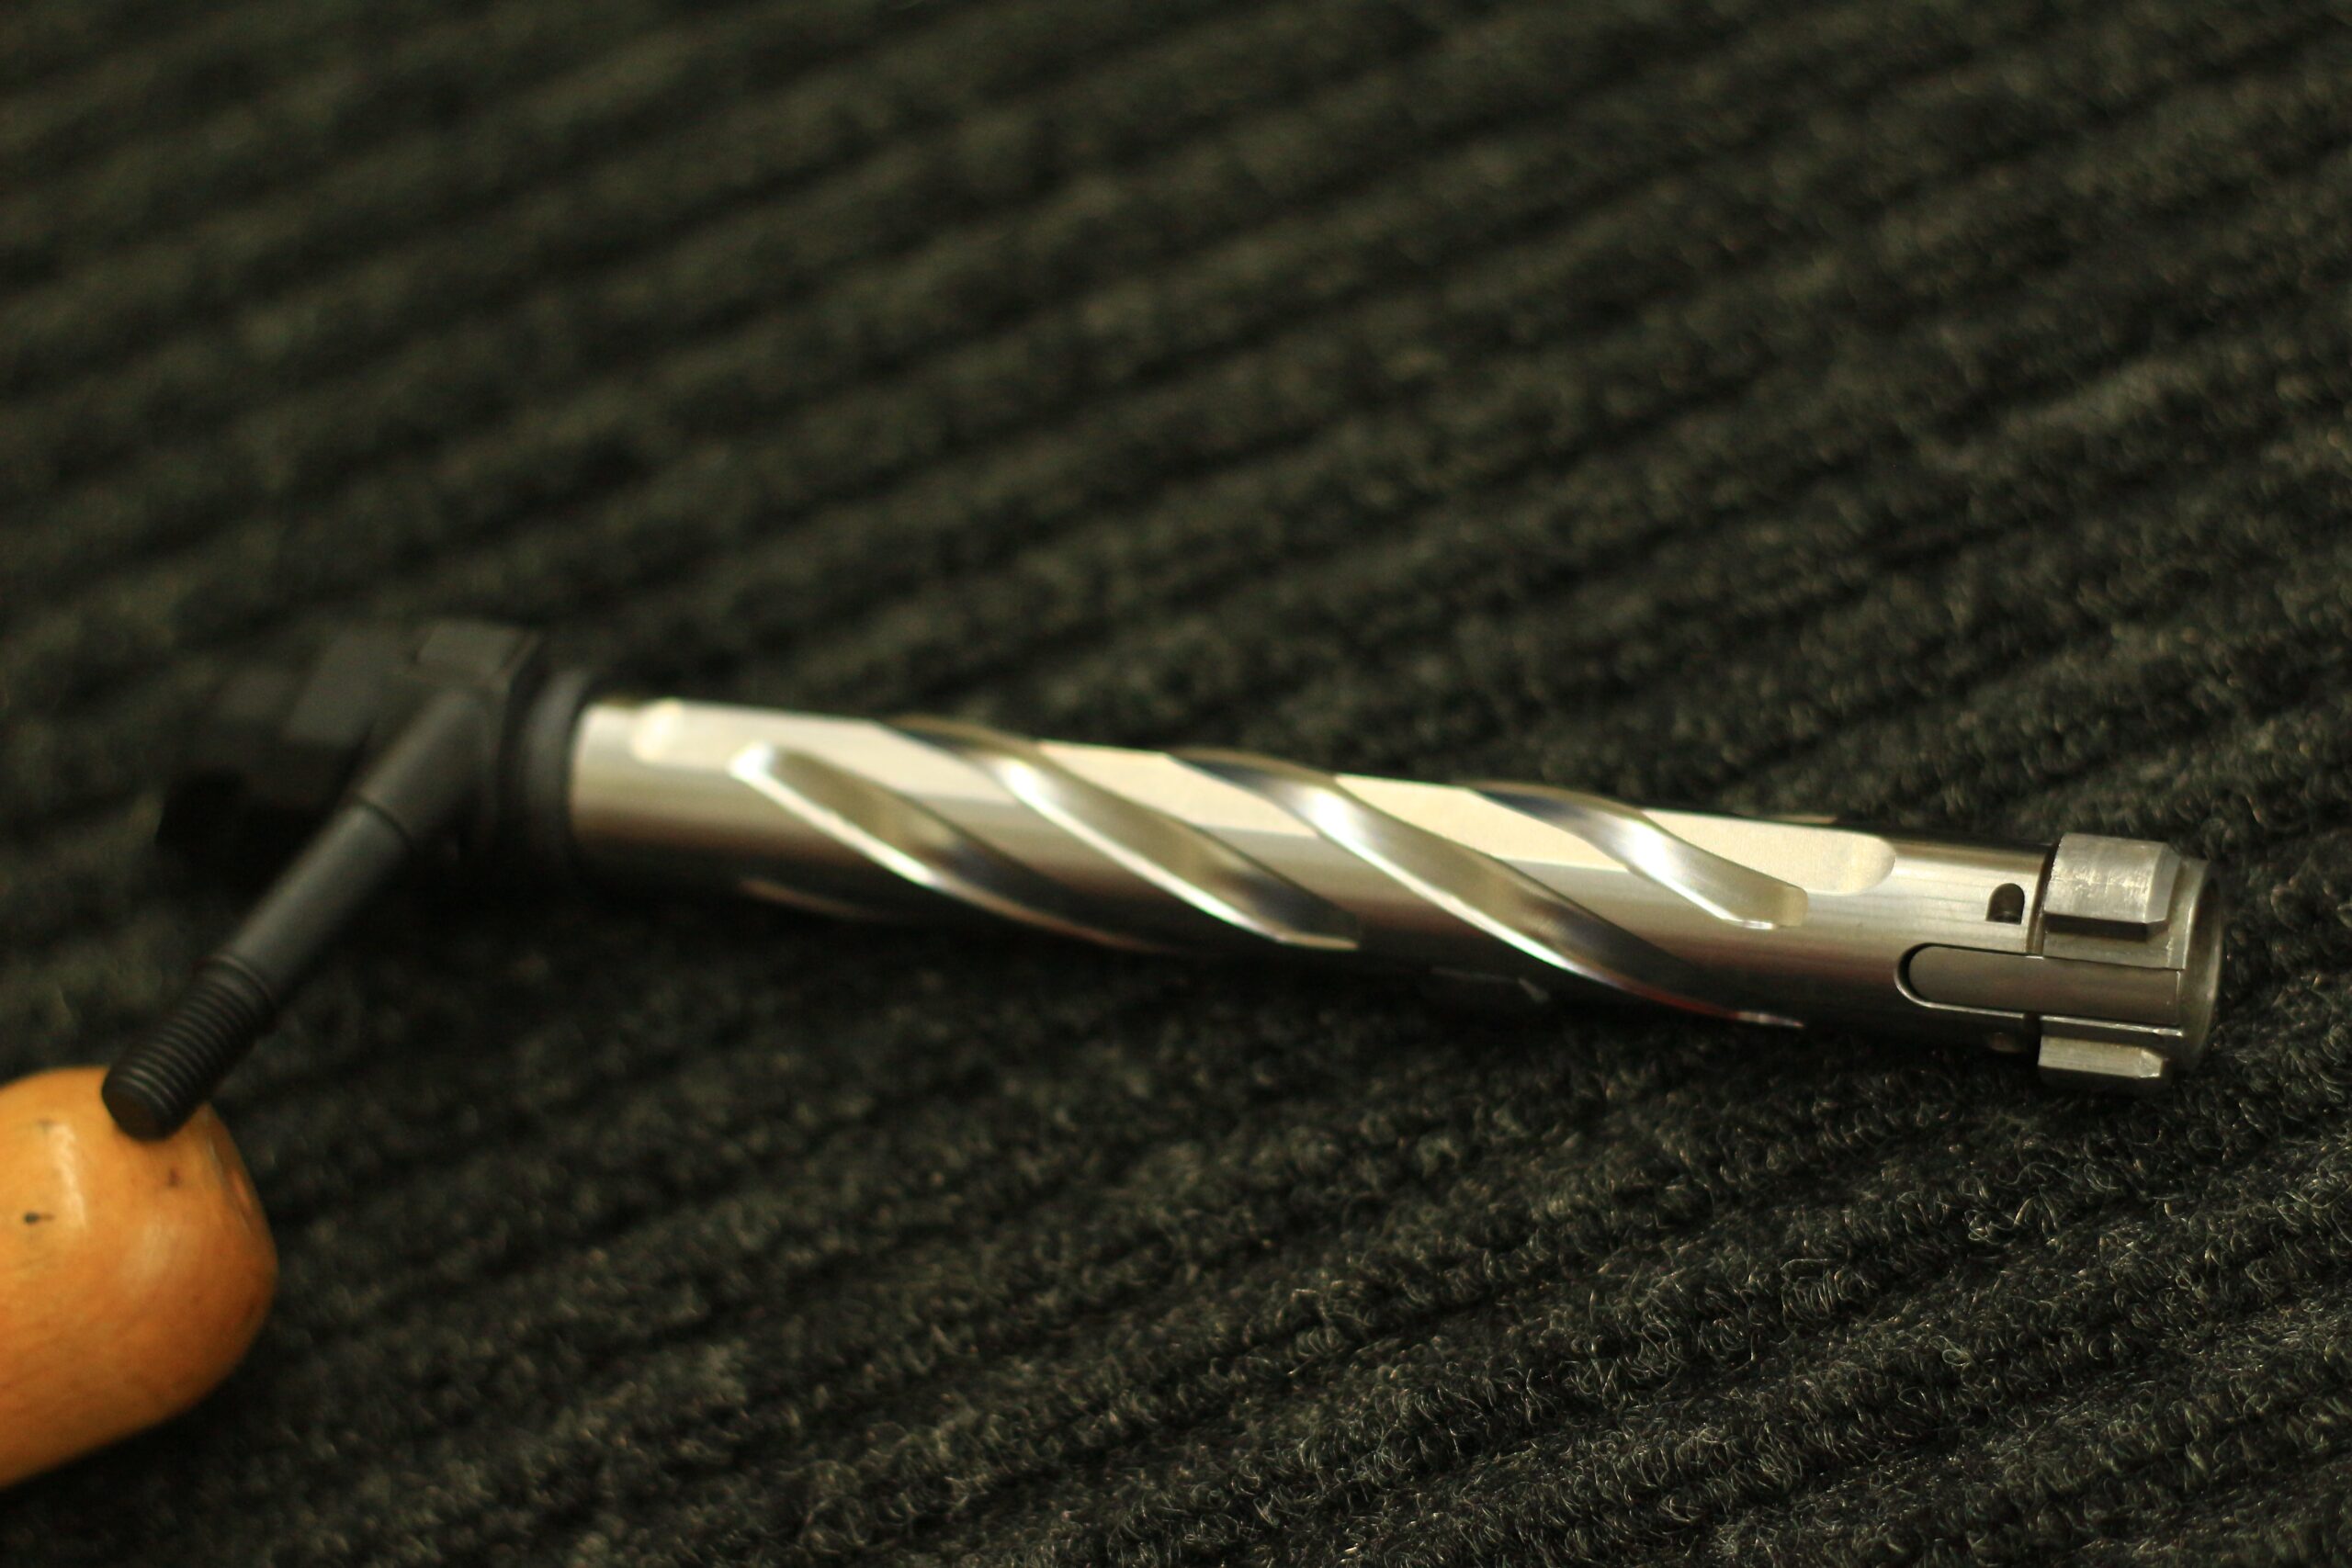
GUNSMITHING SERVICES: Bolt fluting
Price range: $65.00 through $300.00
Description
In 2010 LRI launched a Group Buy on the Sniper’s Hide Web forum that set a new bar for what is possible. With only two of us here, we processed over 600 bolts in a 5-week period! Since that time, we’ve fluted literally thousands of bolts and expanded our library to include a number of other manufacturers.
What is bolt fluting and why do it?
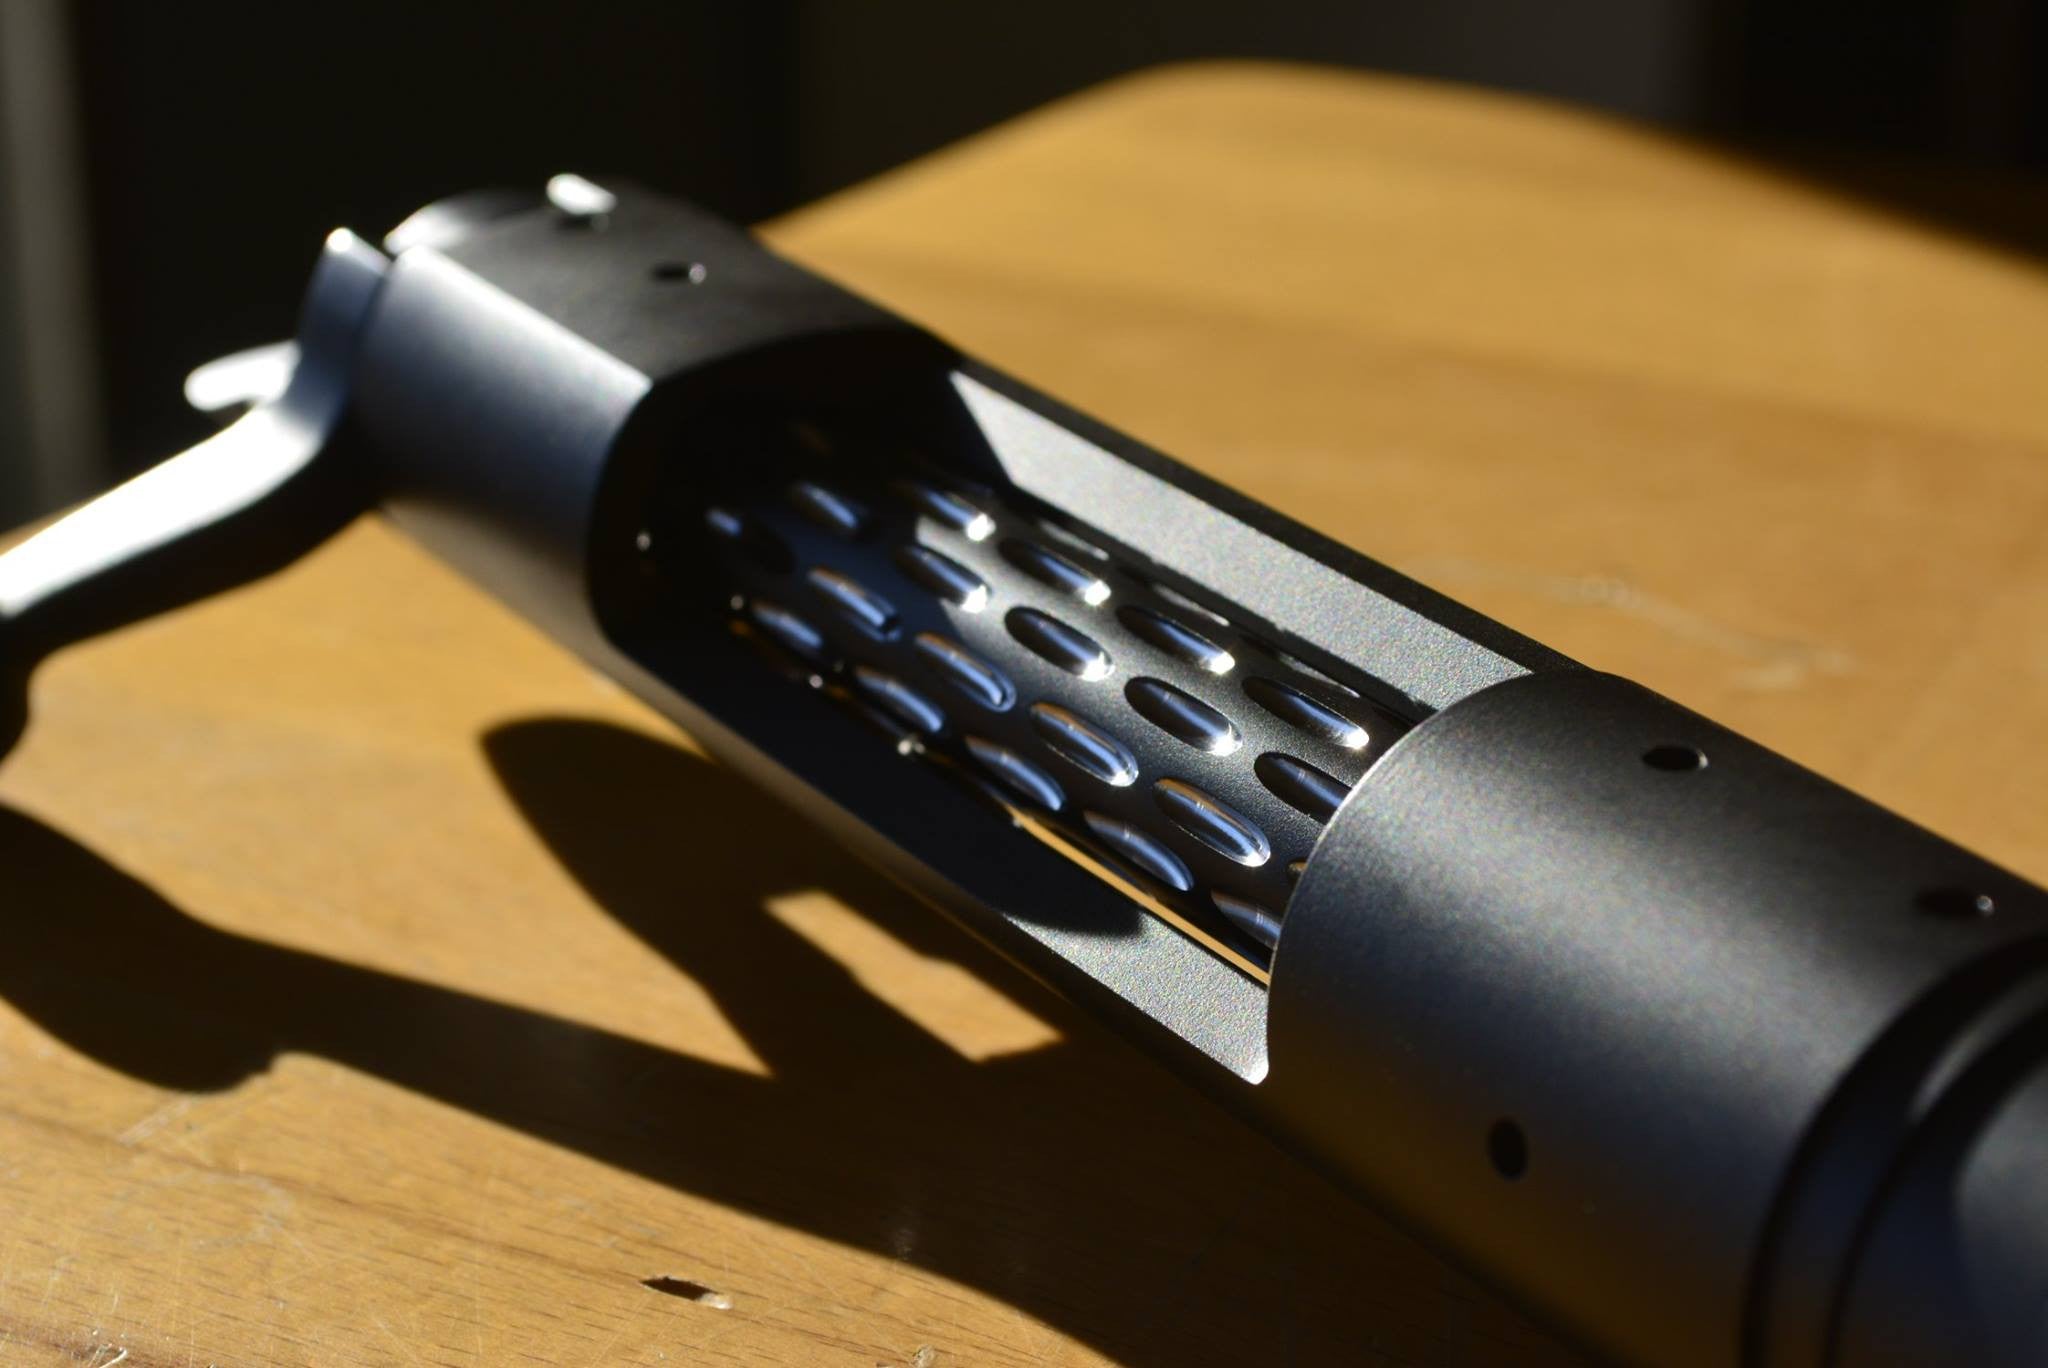
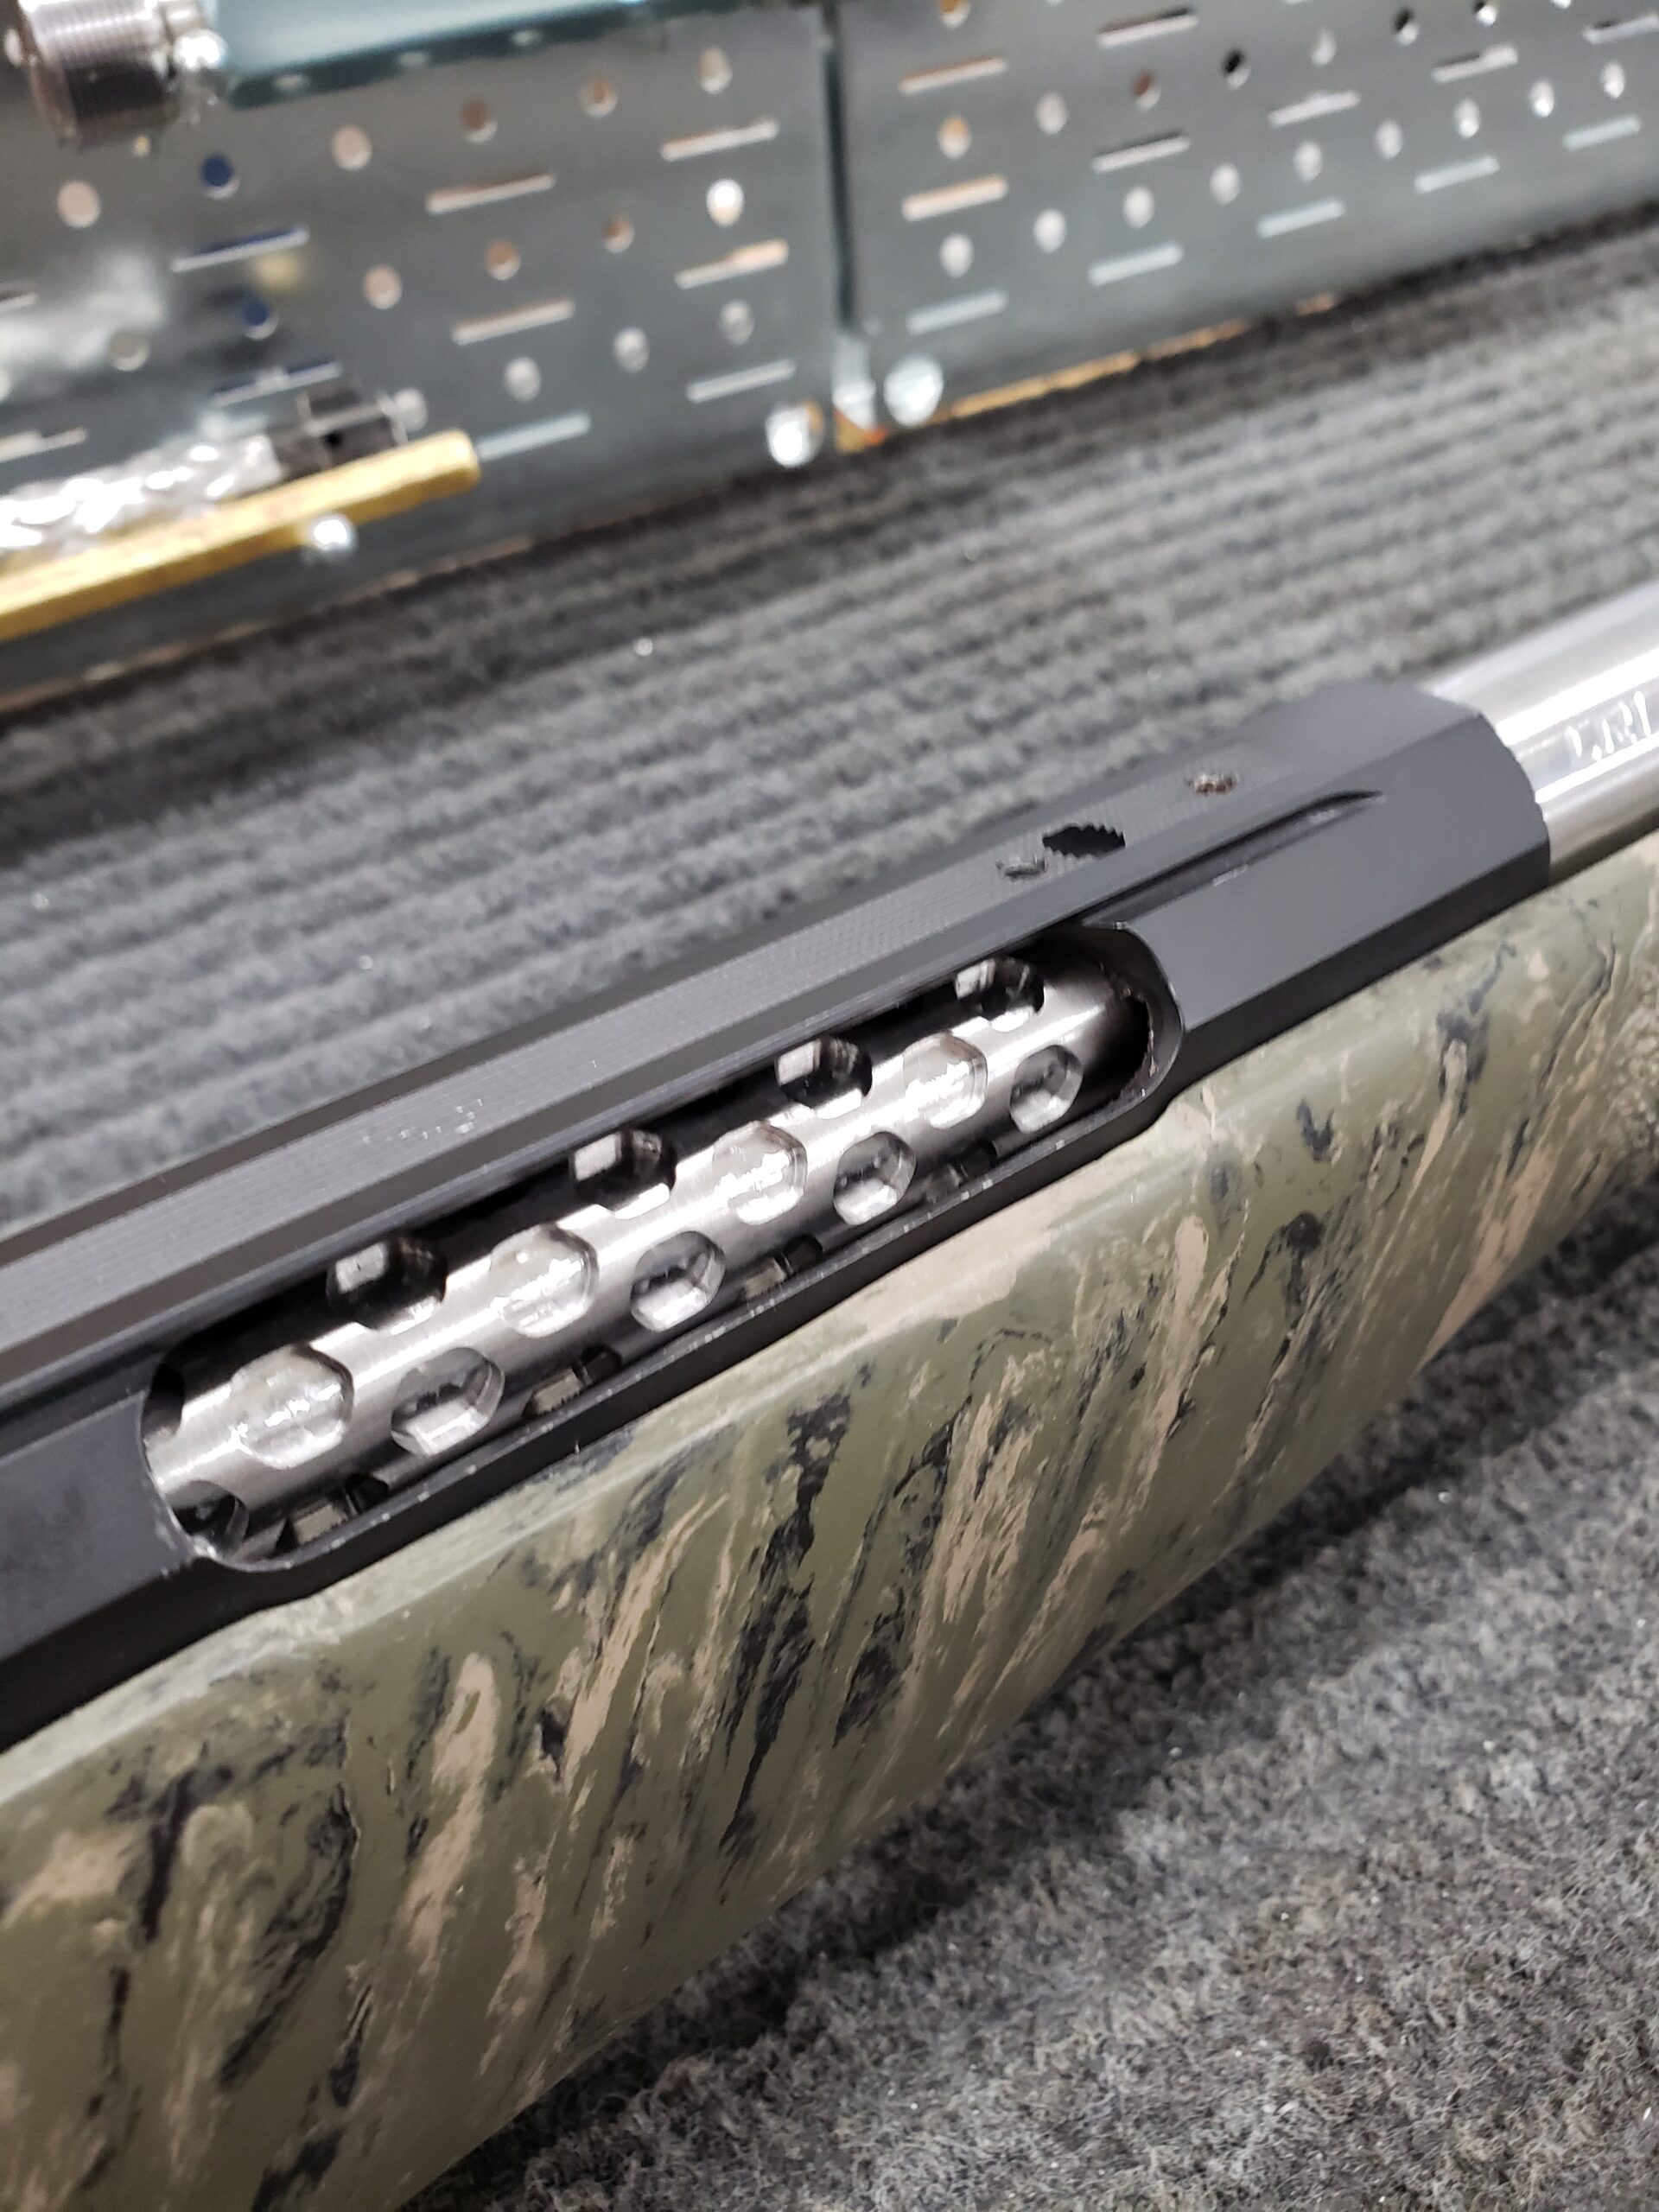
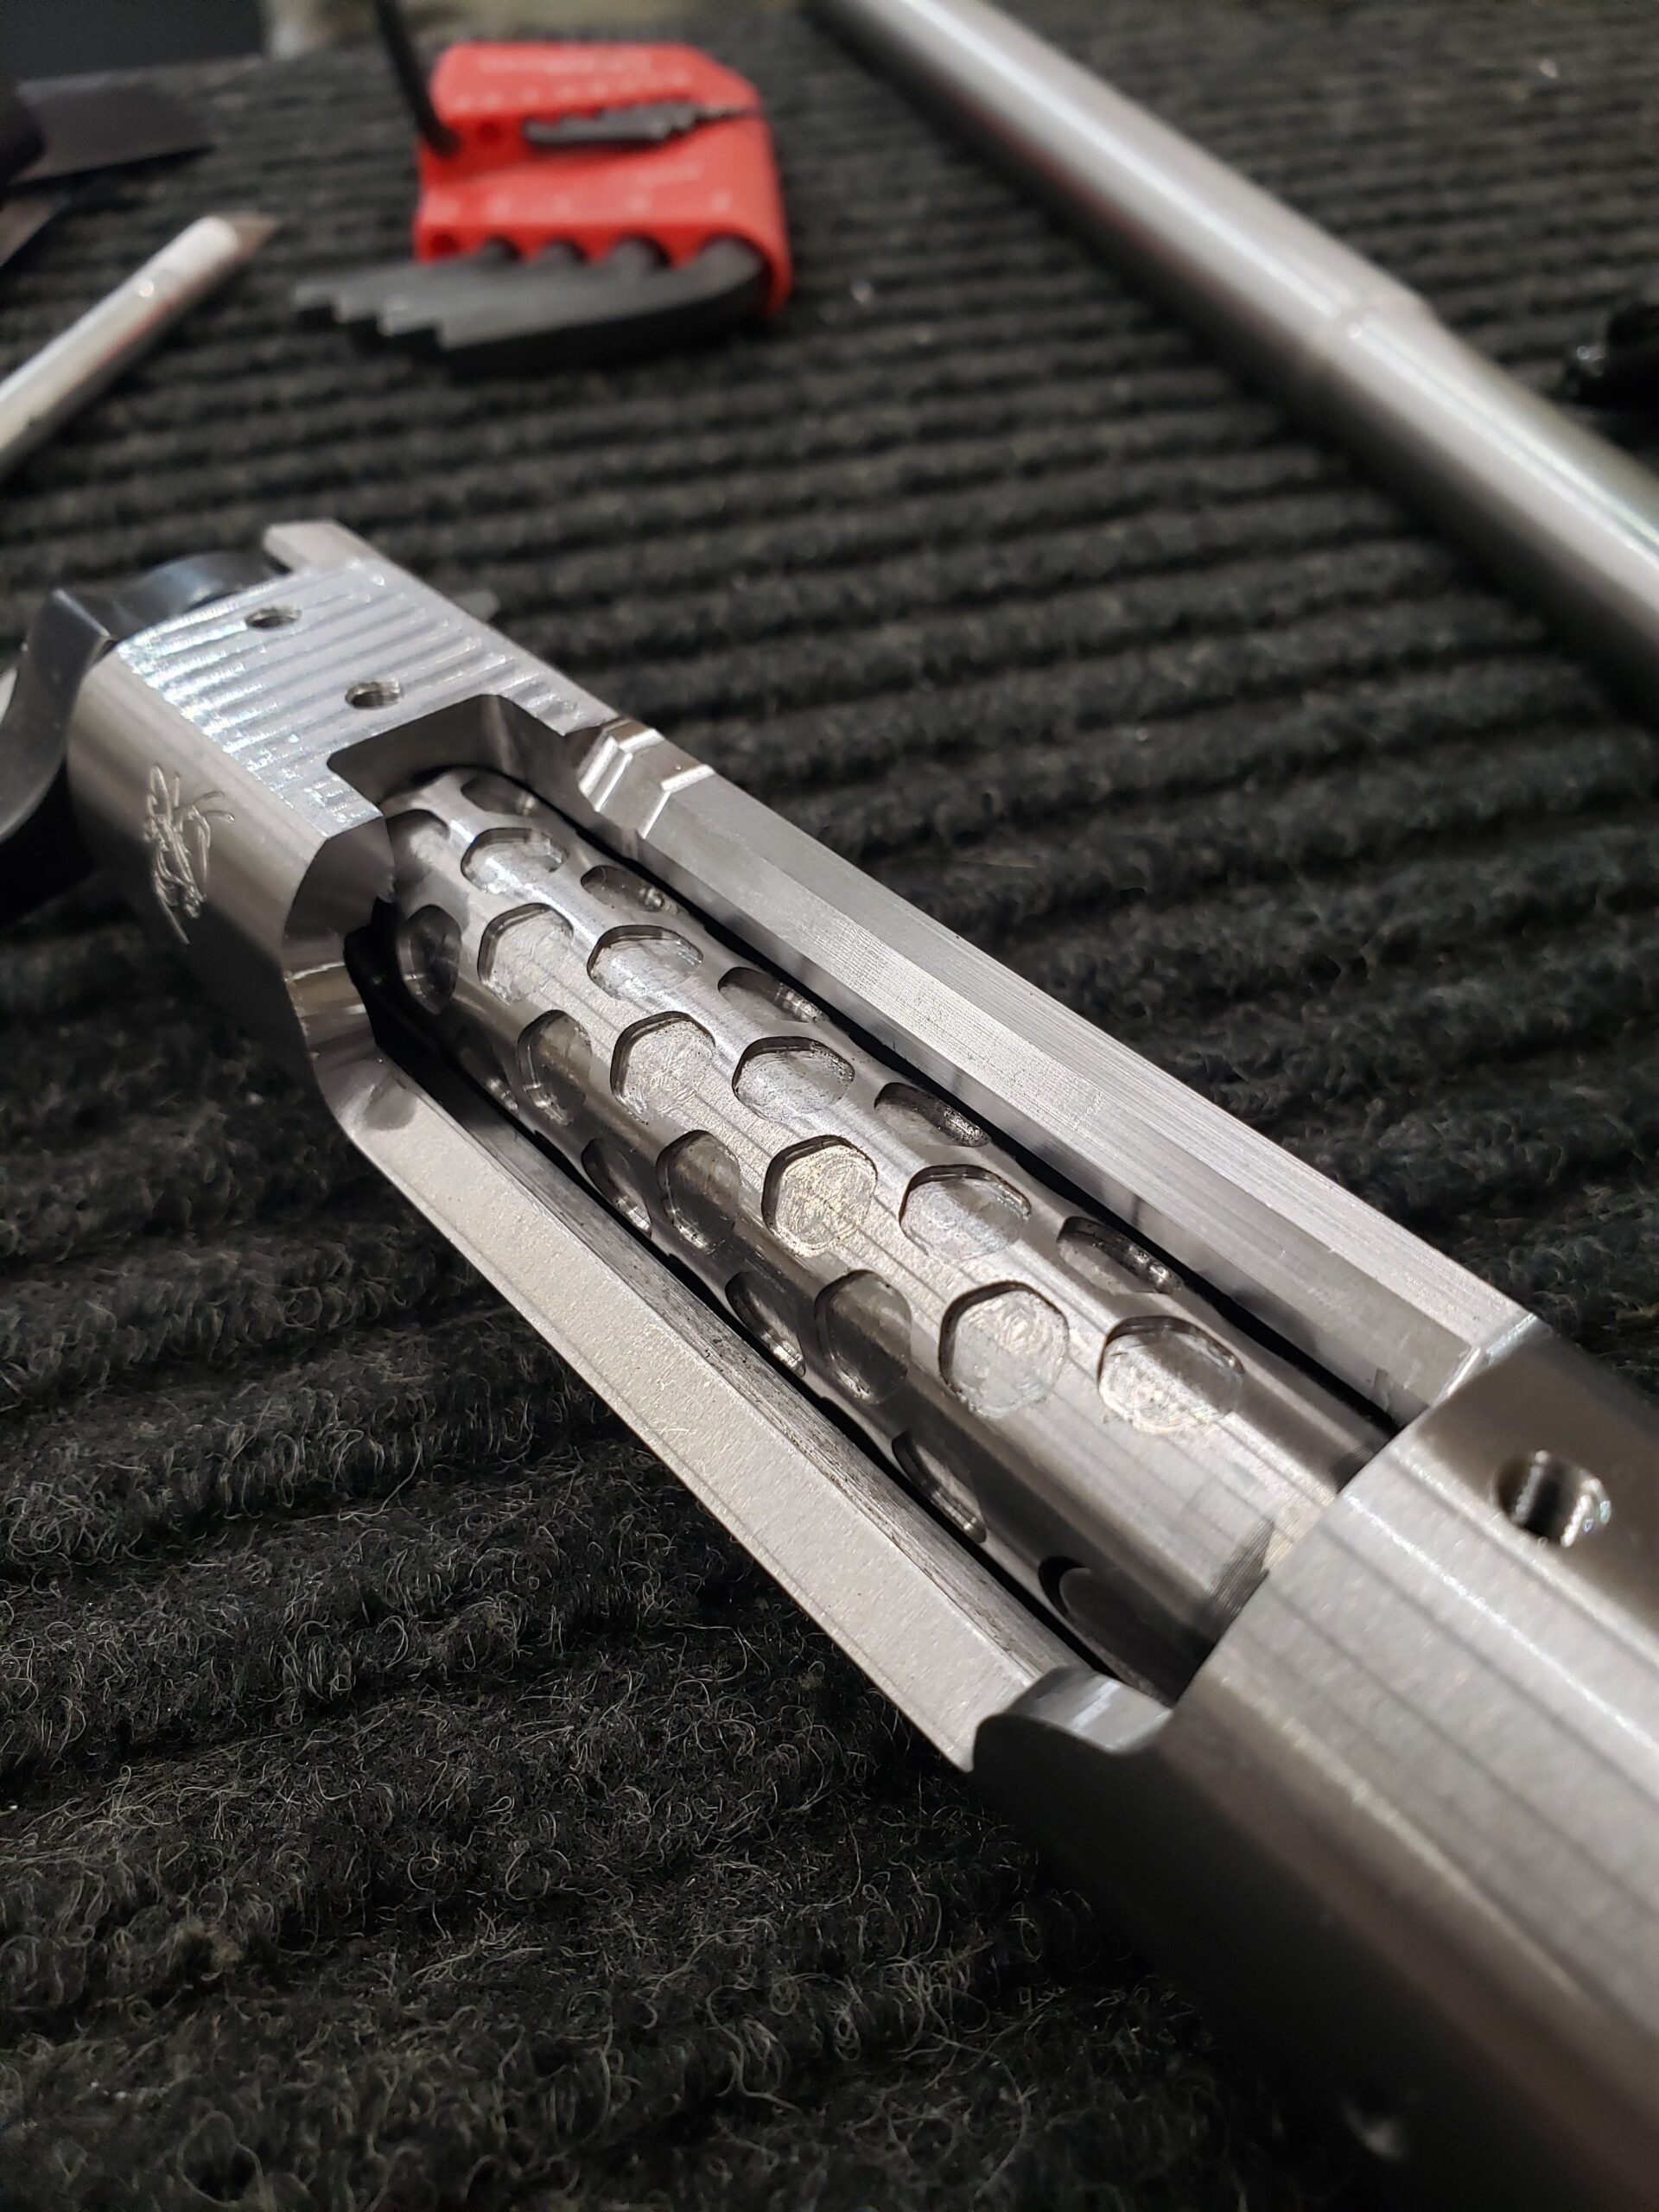
Bolt fluting is purely cosmetic. There has been a long-standing debate about its ability to “scrub” the raceways of foreign material. Its a discussion we don’t involve ourselves with. It does offer some degree of weight reduction, although the gains are trivial at best. We treat it as a cosmetic alteration to add a little personality to your rifle. Nothing more.
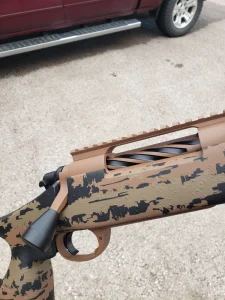
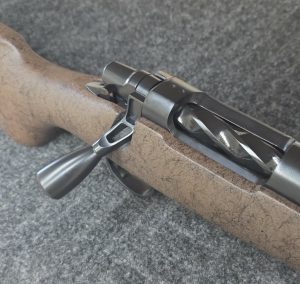
Elective Services and Finishing:
We have a broad menu of additional services that pair well with bolt fluting. These are listed in the Gunsmithing Services Menu.
- Striker Pin Bushing Install
- Faceted Bolt Shroud (M700 only)
- Extended, “Tactical” Knob Install
- Cerakote
- Polishing
- Glass bead (For stainless steel bolts only)
- Manganese Phosphate Parkerizing (Carbon steel bolts only)
- Hot Tank Bluing (Carbon steel bolts only)
Custom fluting:
We welcome clients with special requests, and offer this on a case-by-case basis. Jobs like these are quoted as “Time and Material” with a shop rate of $150.00/hr. We are happy to help.
LIMITATIONS:
This service is offered for PUSH FEED actions only, with only a few exceptions. If you own a Control Round Feed Pre 64 type Winchester model 70 action, with a non-rotating, Mauser-style claw extractor, we will not perform this service. This is because of the anti bind “lump” present on the outside of the bolt body and the “wedding band” style extractor retaining ring.
Historically, we have avoided fluting any bolt featuring a fixed/blade type ejector. With this design, the ejector blade will fall into the flute during normal operation creating a very annoying, “ratchet-like” feel. Some bolts become completely ruined as the flute prevents the bolt from rotating into battery due to it locking up in much the same way a mechanic’s ratchet works. We have resolved this avoiding the bolt body contour along the ejector path. By giving the ejector a “line of sight” path to the rear portion of the bolt body full functionality is preserved.
Patterns:
We offer several distinct patterns available in 2 primary cutter geometries.
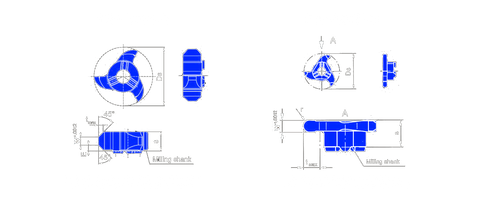
Pattern “A” Pattern “B”
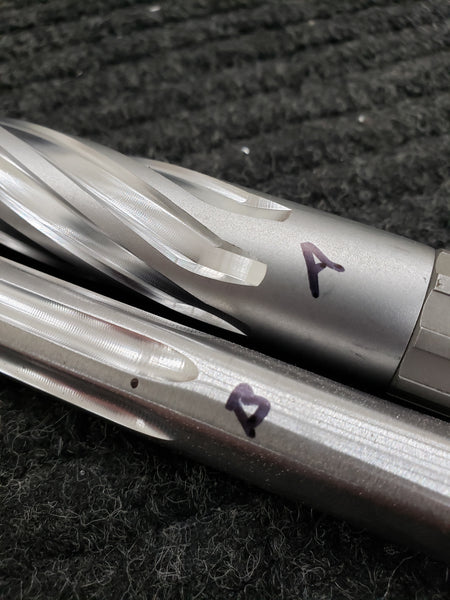
The difference between the two patterns is purely a personal preference. We have never seen one out perform the other.
Standard menu:
- High Helix (Pattern A or B)
- Standard Helix (Pattern A or B)
- Straight (Pattern A or B)
- Interrupted (Pattern A or B)
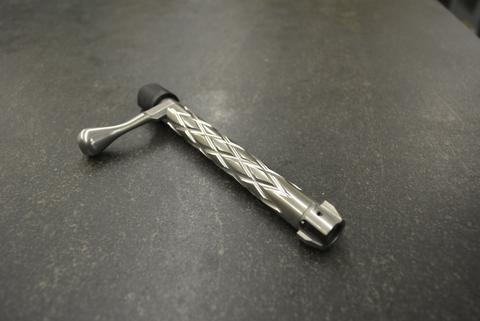
- Diamond (Pattern A or B)
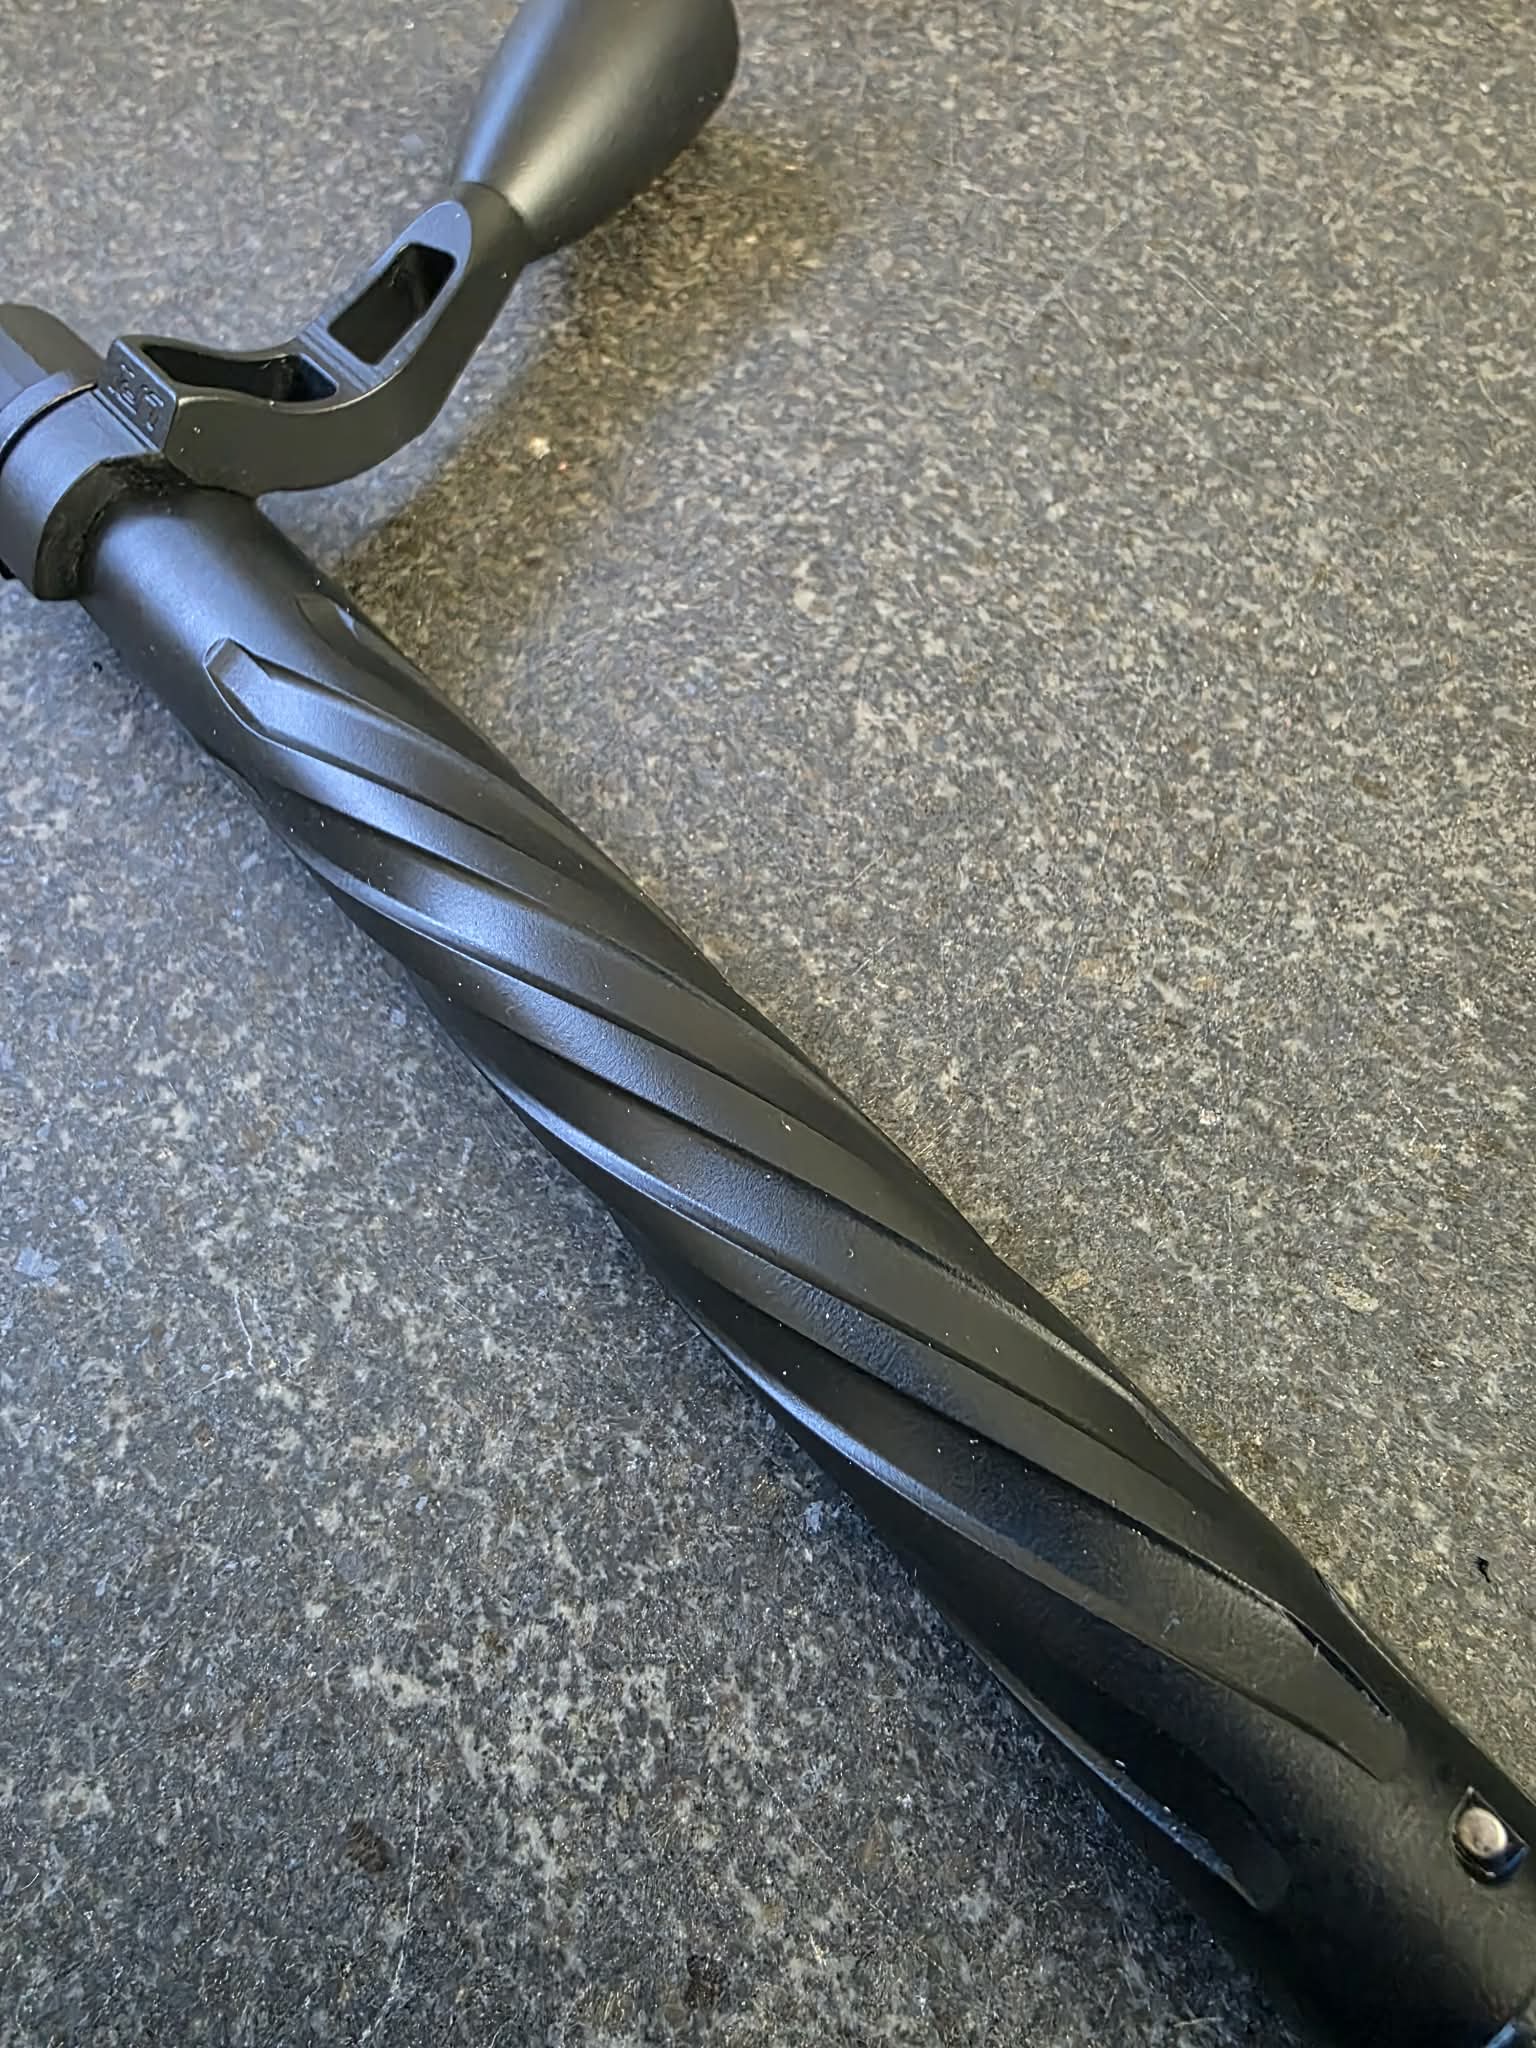
- Wrought Iron
- Murder Hornet
- Pattern X
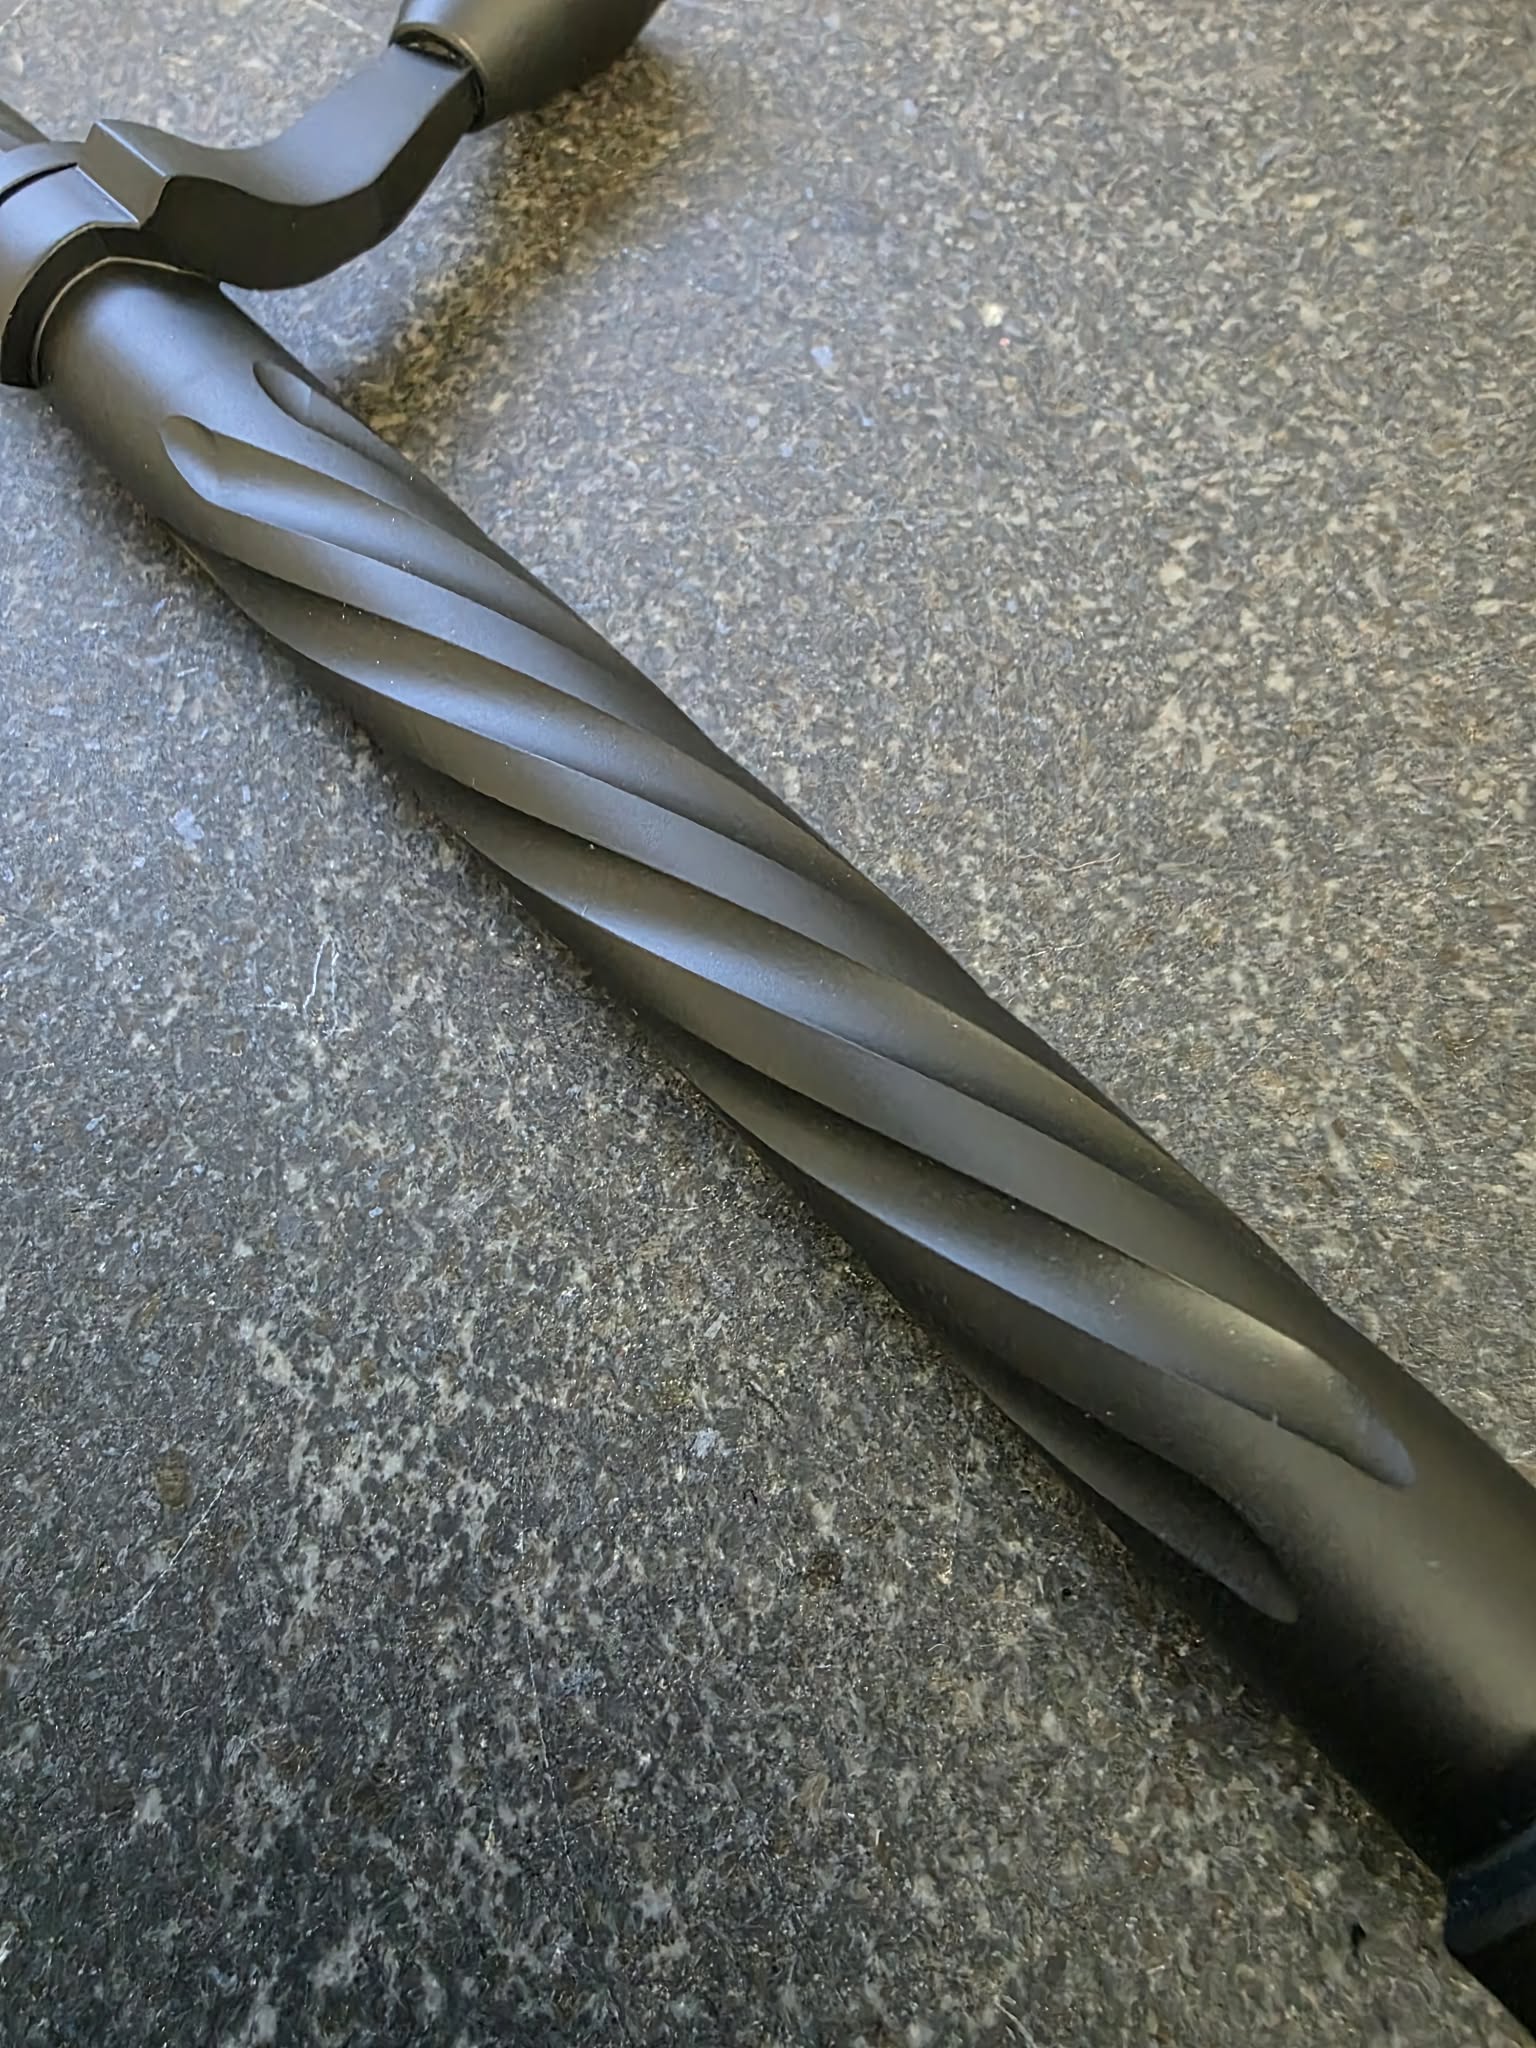
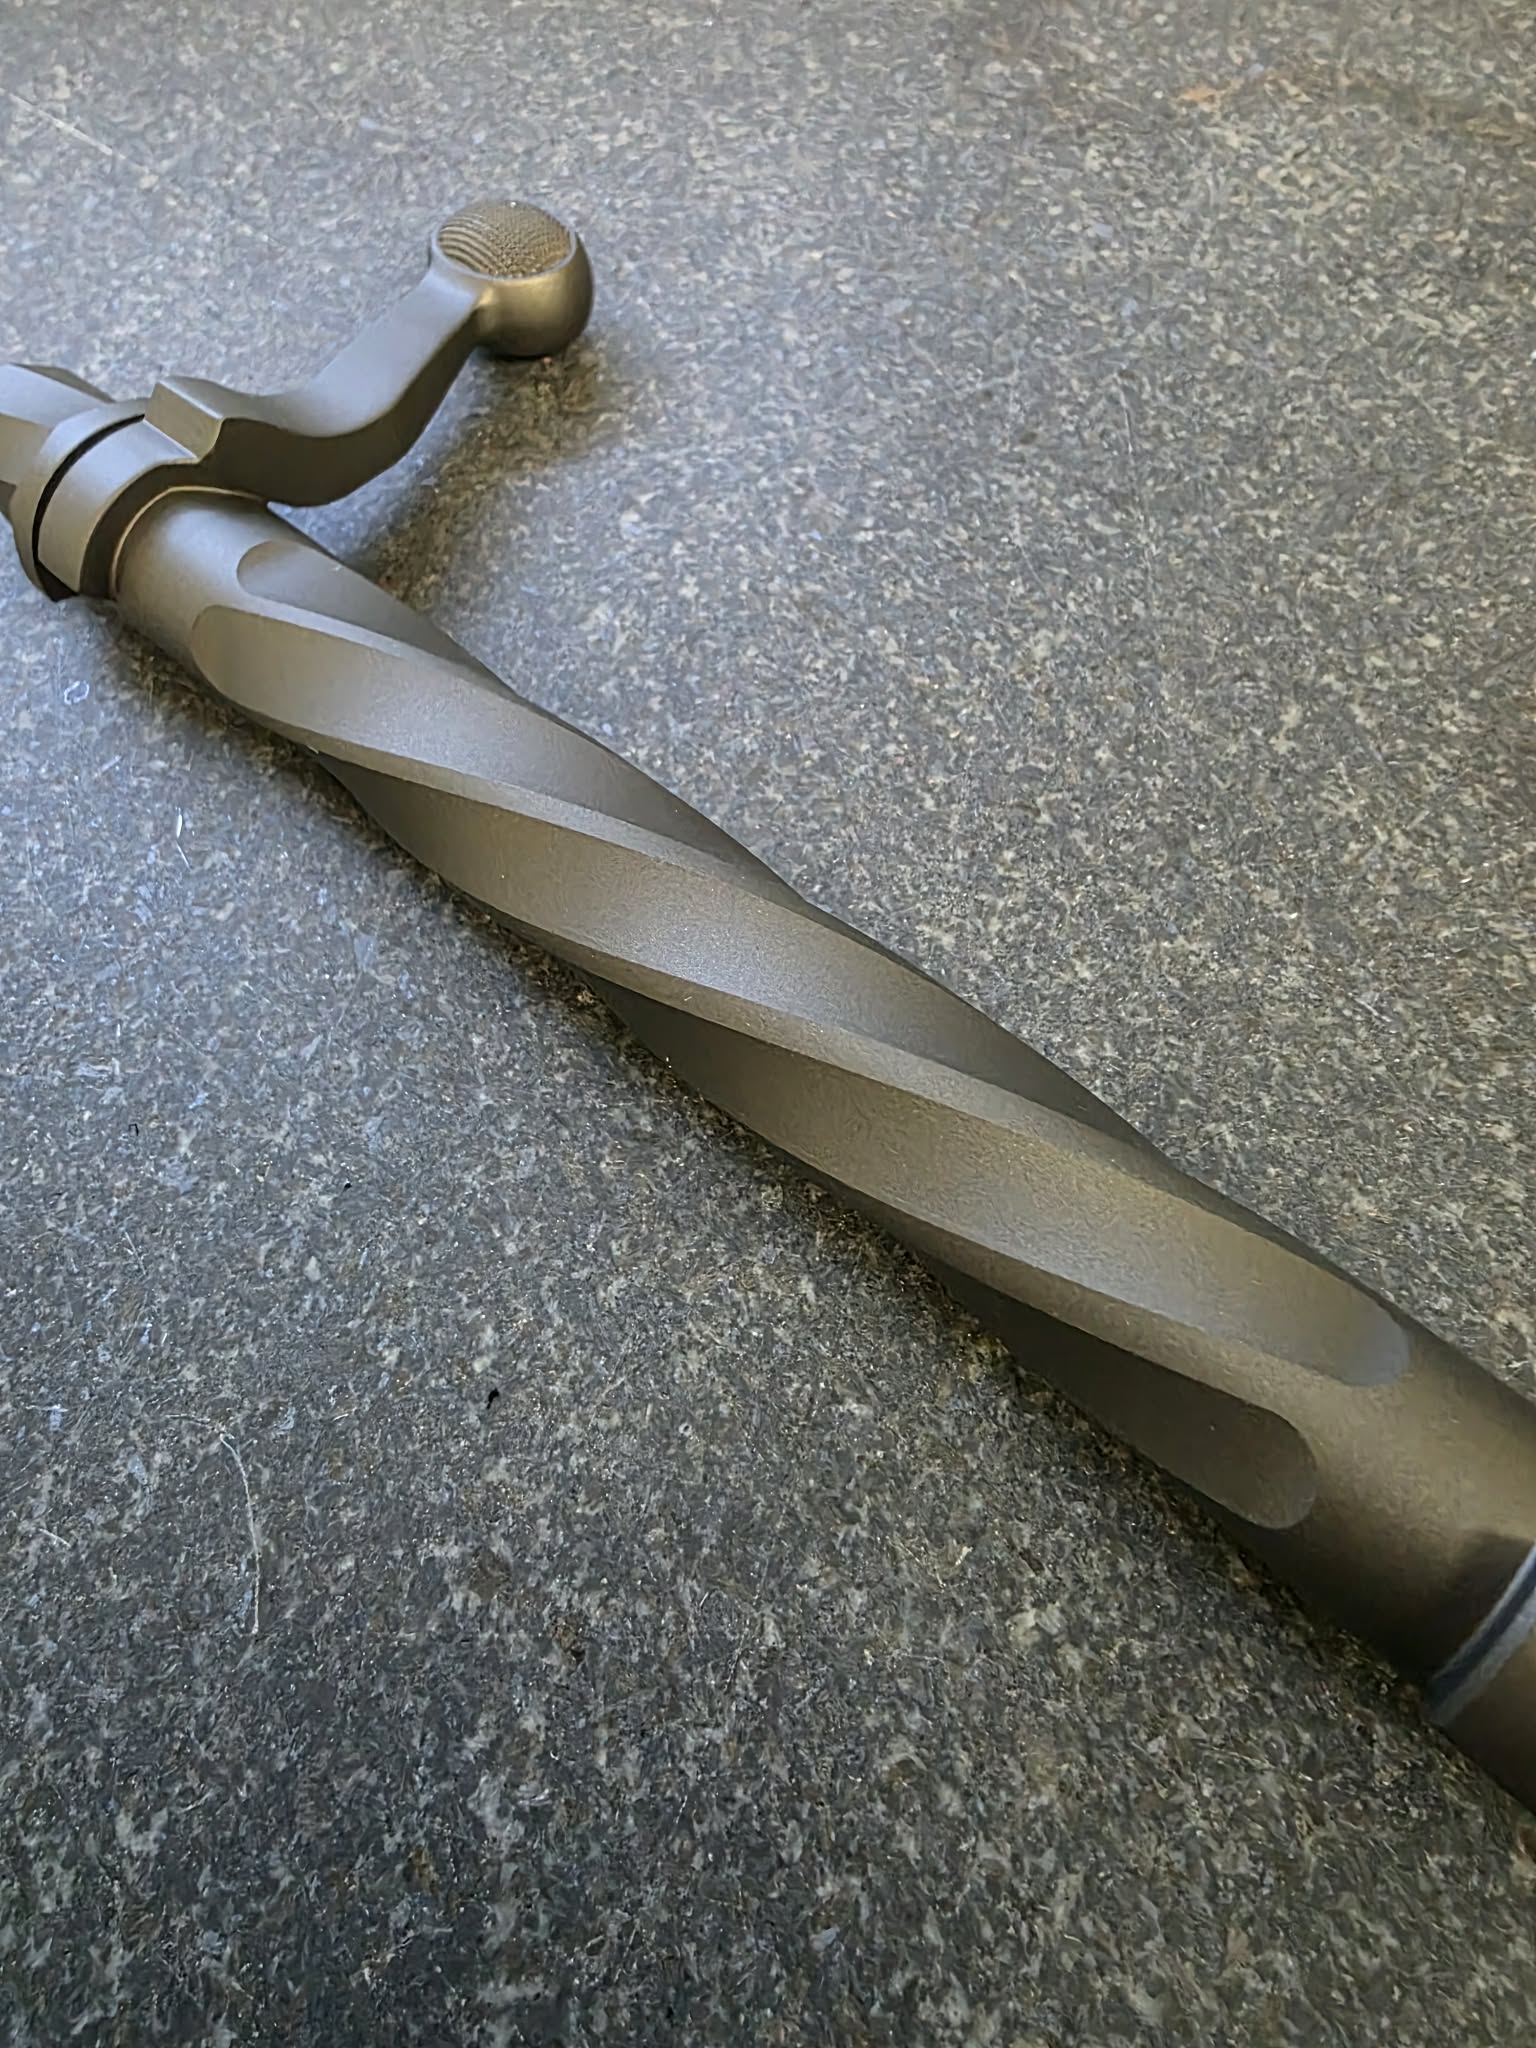
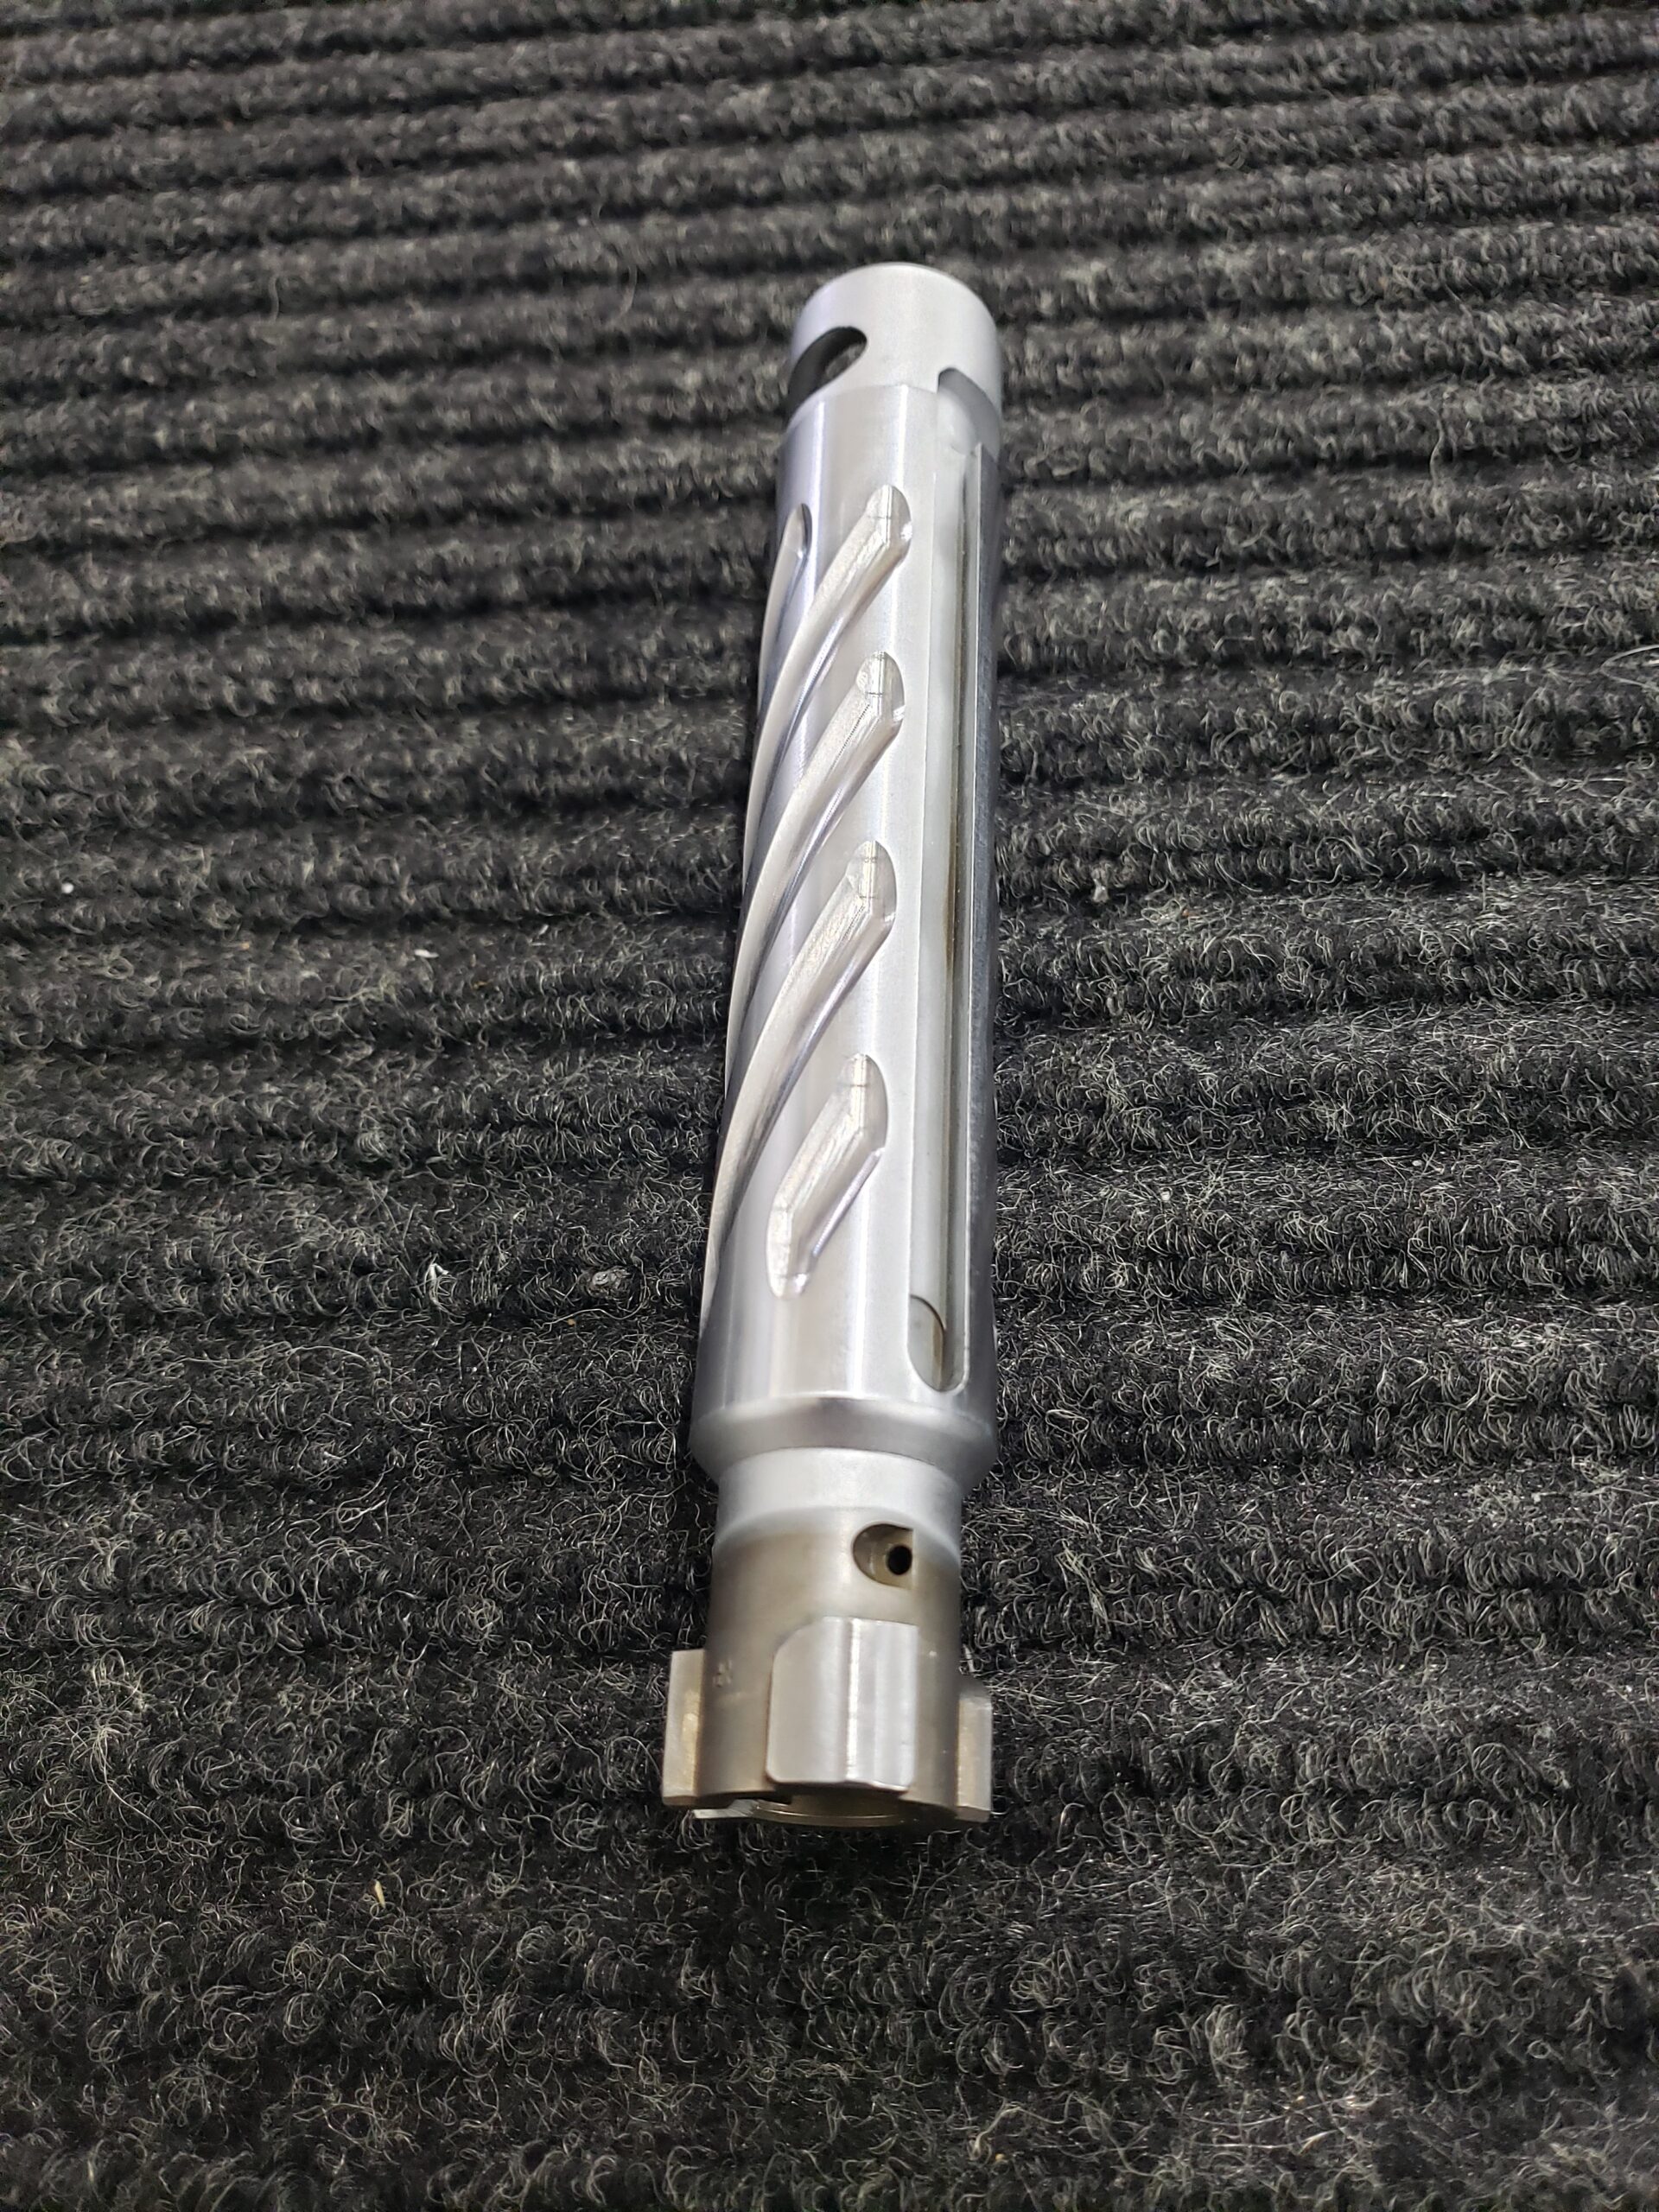
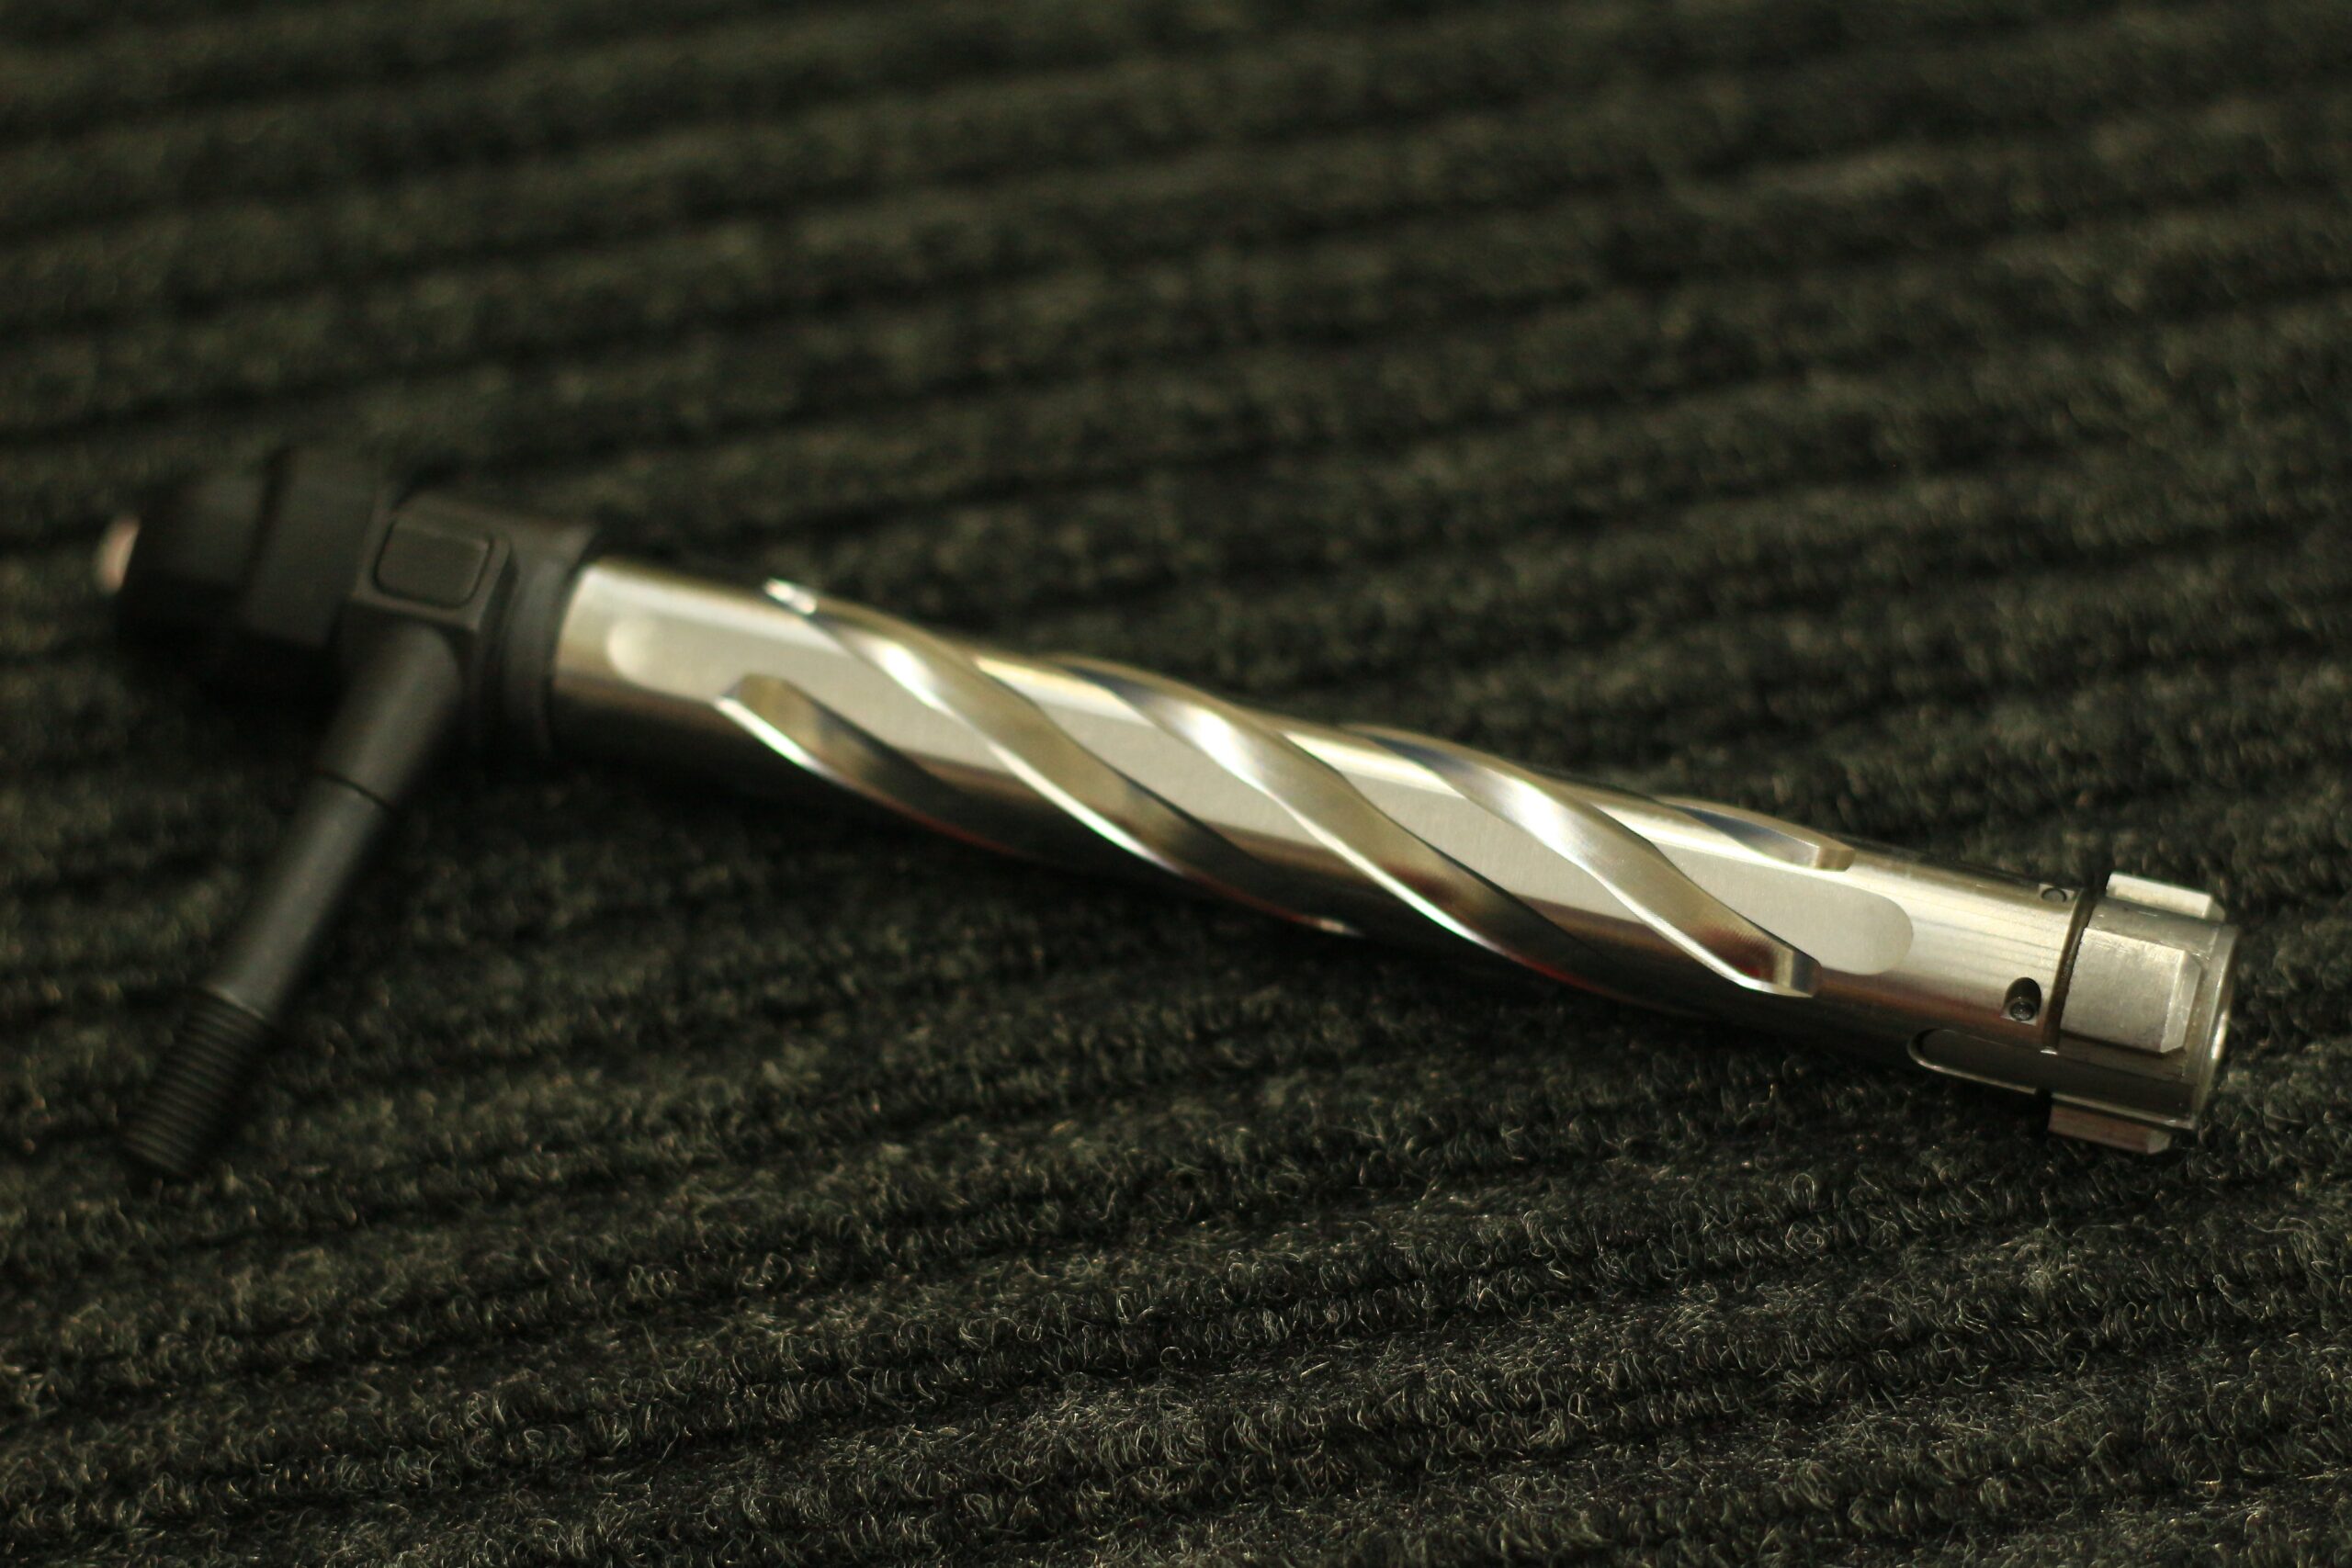
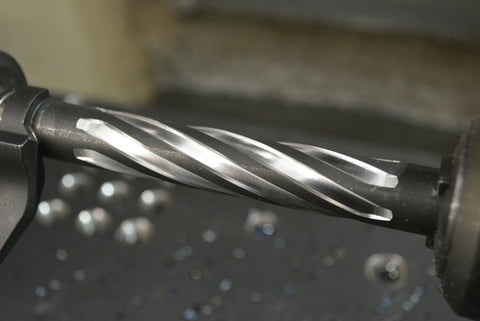
Pattern A High Helix:
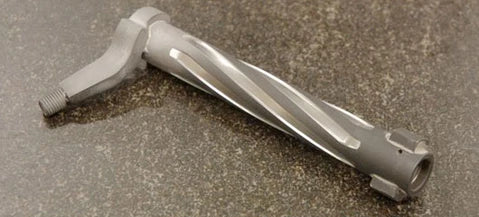
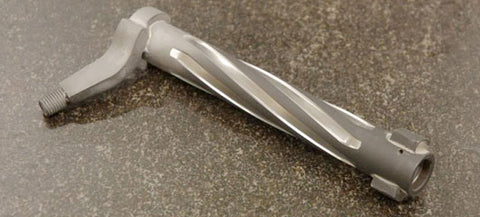
Pattern A Standard Helix:
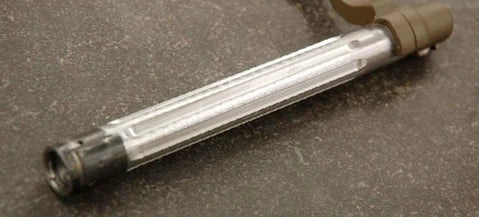
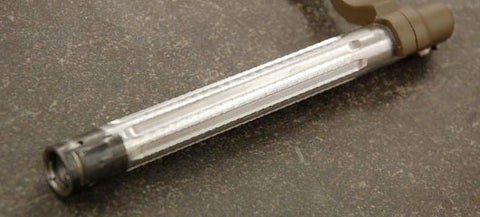
Pattern A Straight:
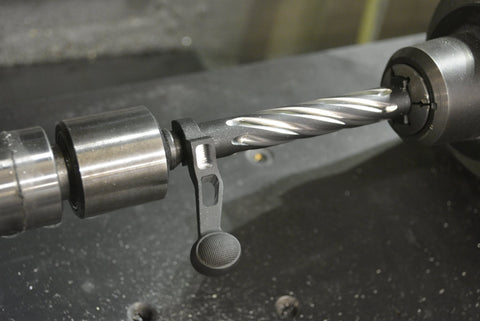
Pattern B High Helix:
Pattern B Standard Helix: (Shown here on a Tikka T3 brand bolt body)
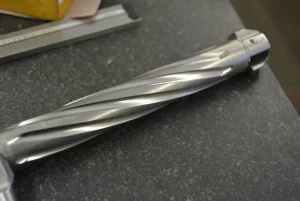
Skip fluting in Pattern B done with a thinner tool cross section:
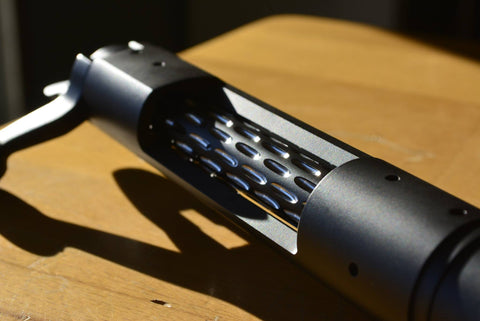
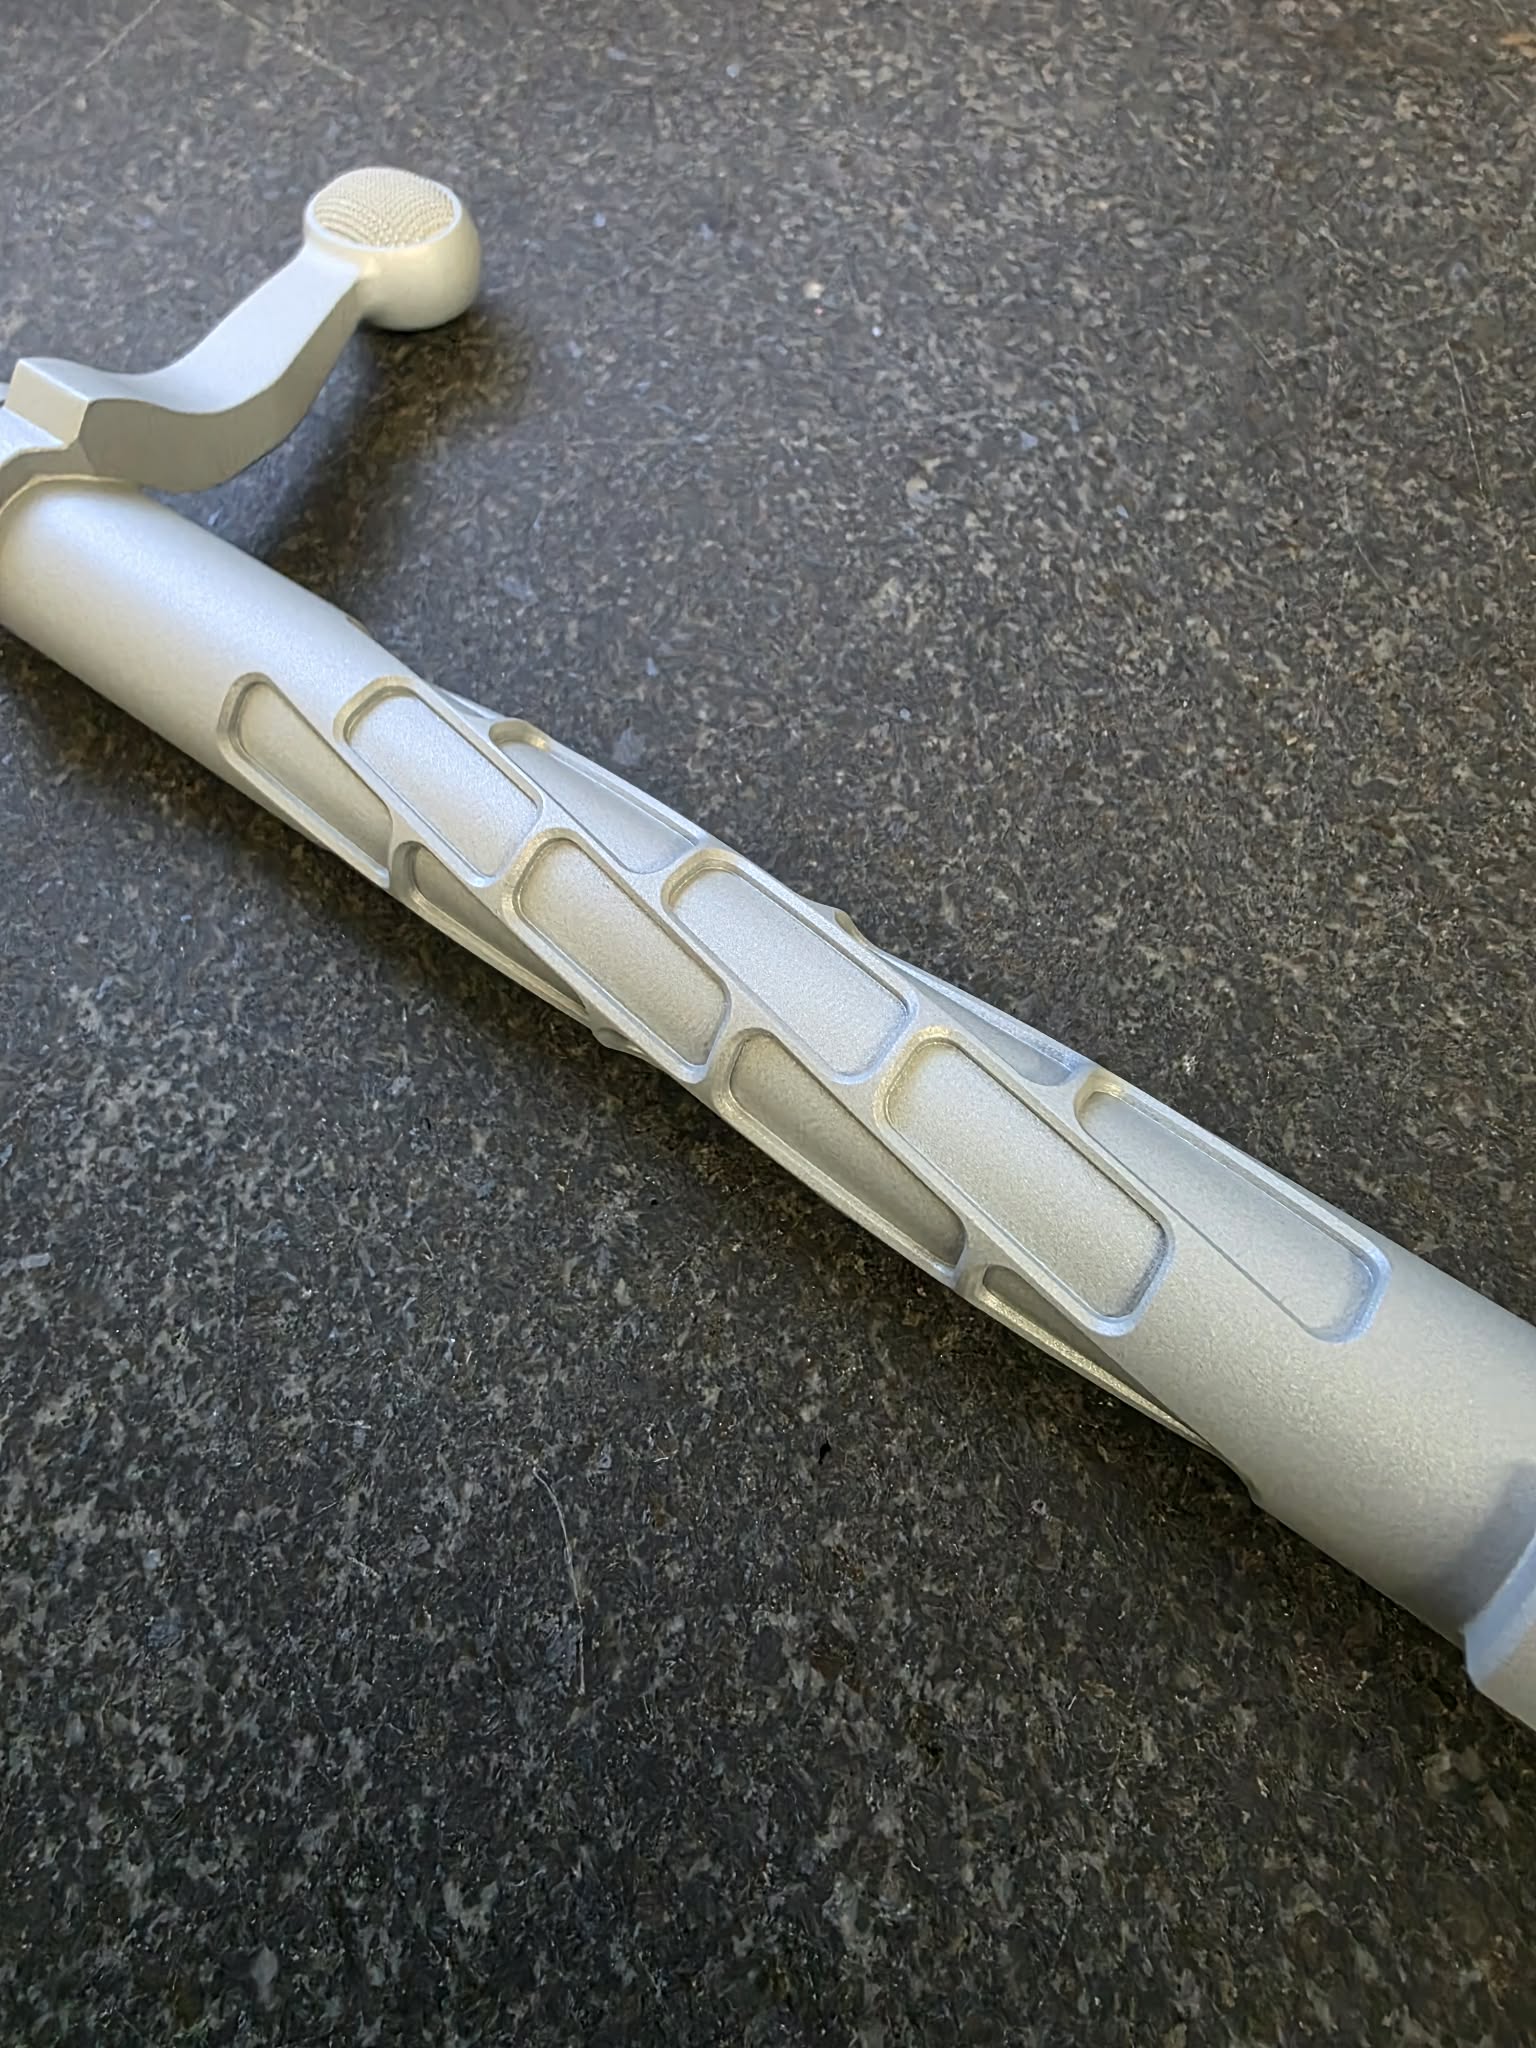
Diamond Pattern B:
This fluting option is only available with the “B” tool geometry.
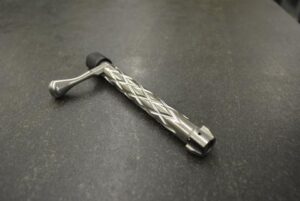
Wrought Iron:
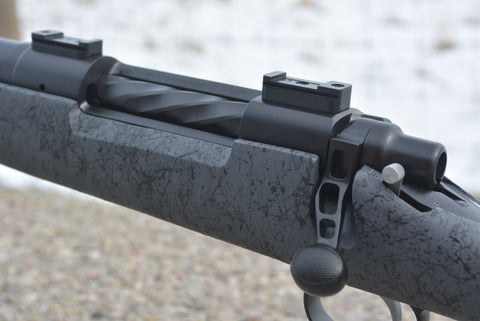
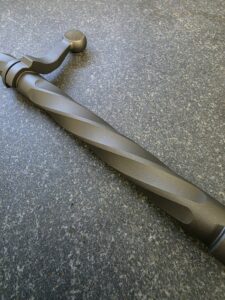
Murder Hornet:
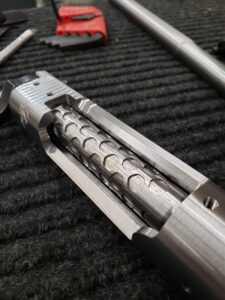
Pattern X:
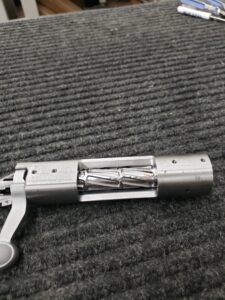
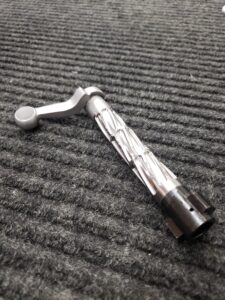
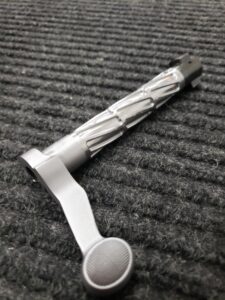
Make and Model specific:
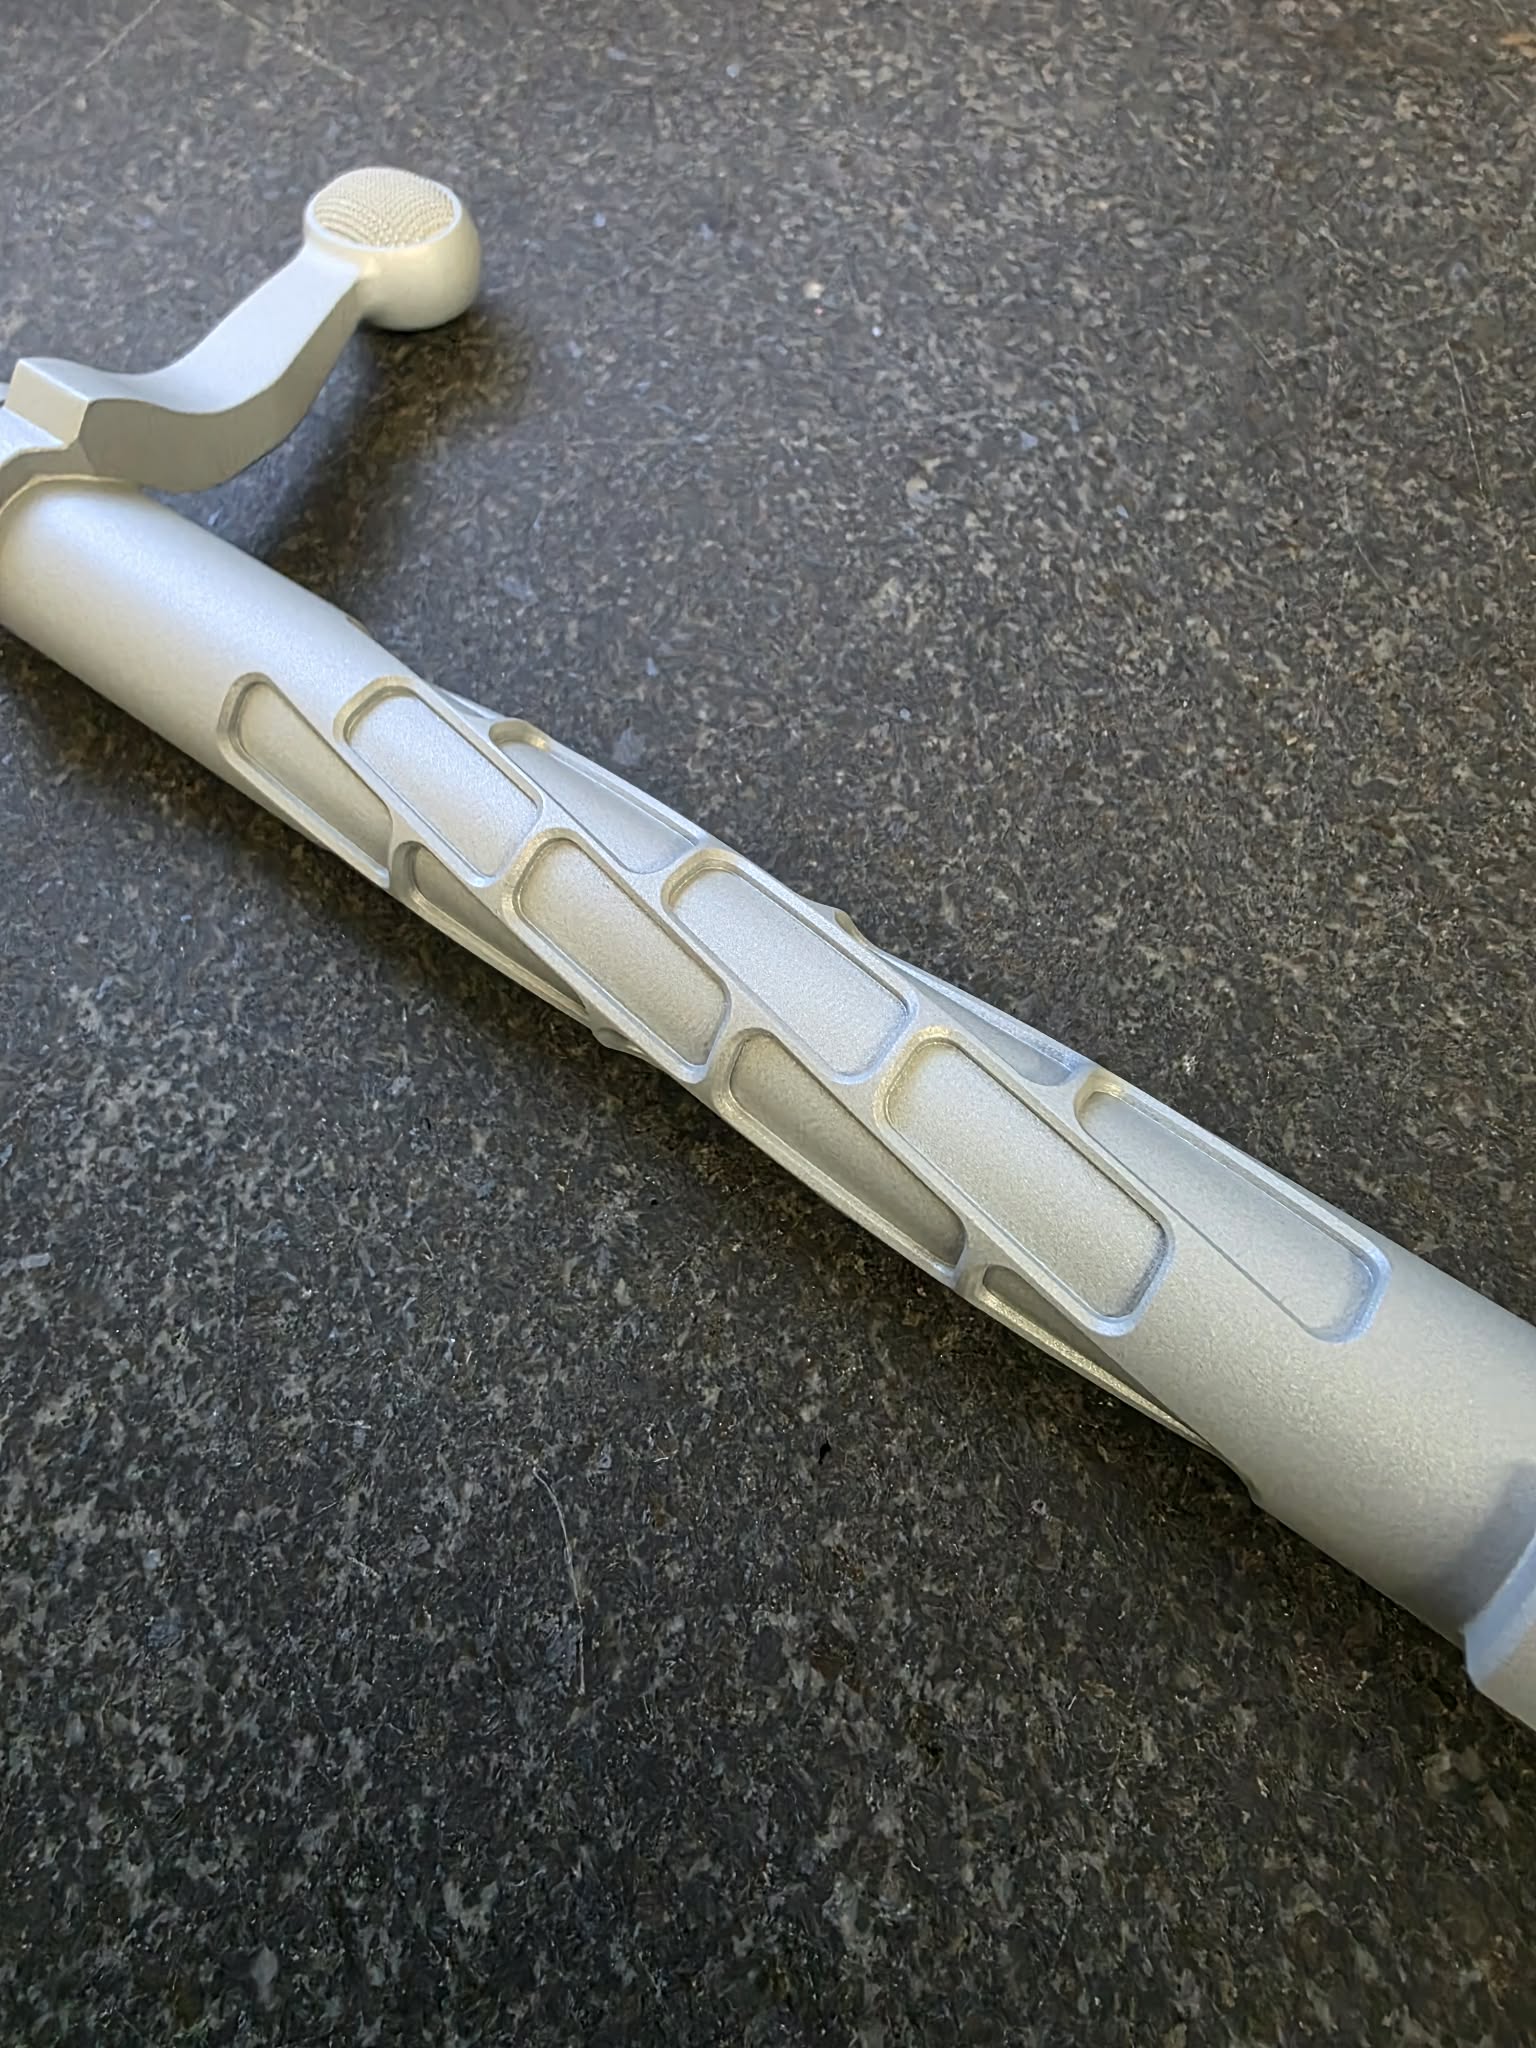
Over the years we have expanded our menu to offer fluting on bolts requiring very specific programming. Because of design constraints, these are limited to what you see here.
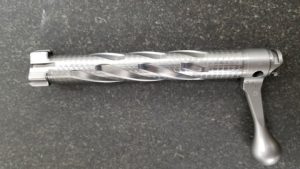
Sako 75 and 85 Control Round Feed with fixed blade ejector fluting, Pattern A:
(Flutes do not invade the path the ejector blade runs on otherwise the action won’t function)
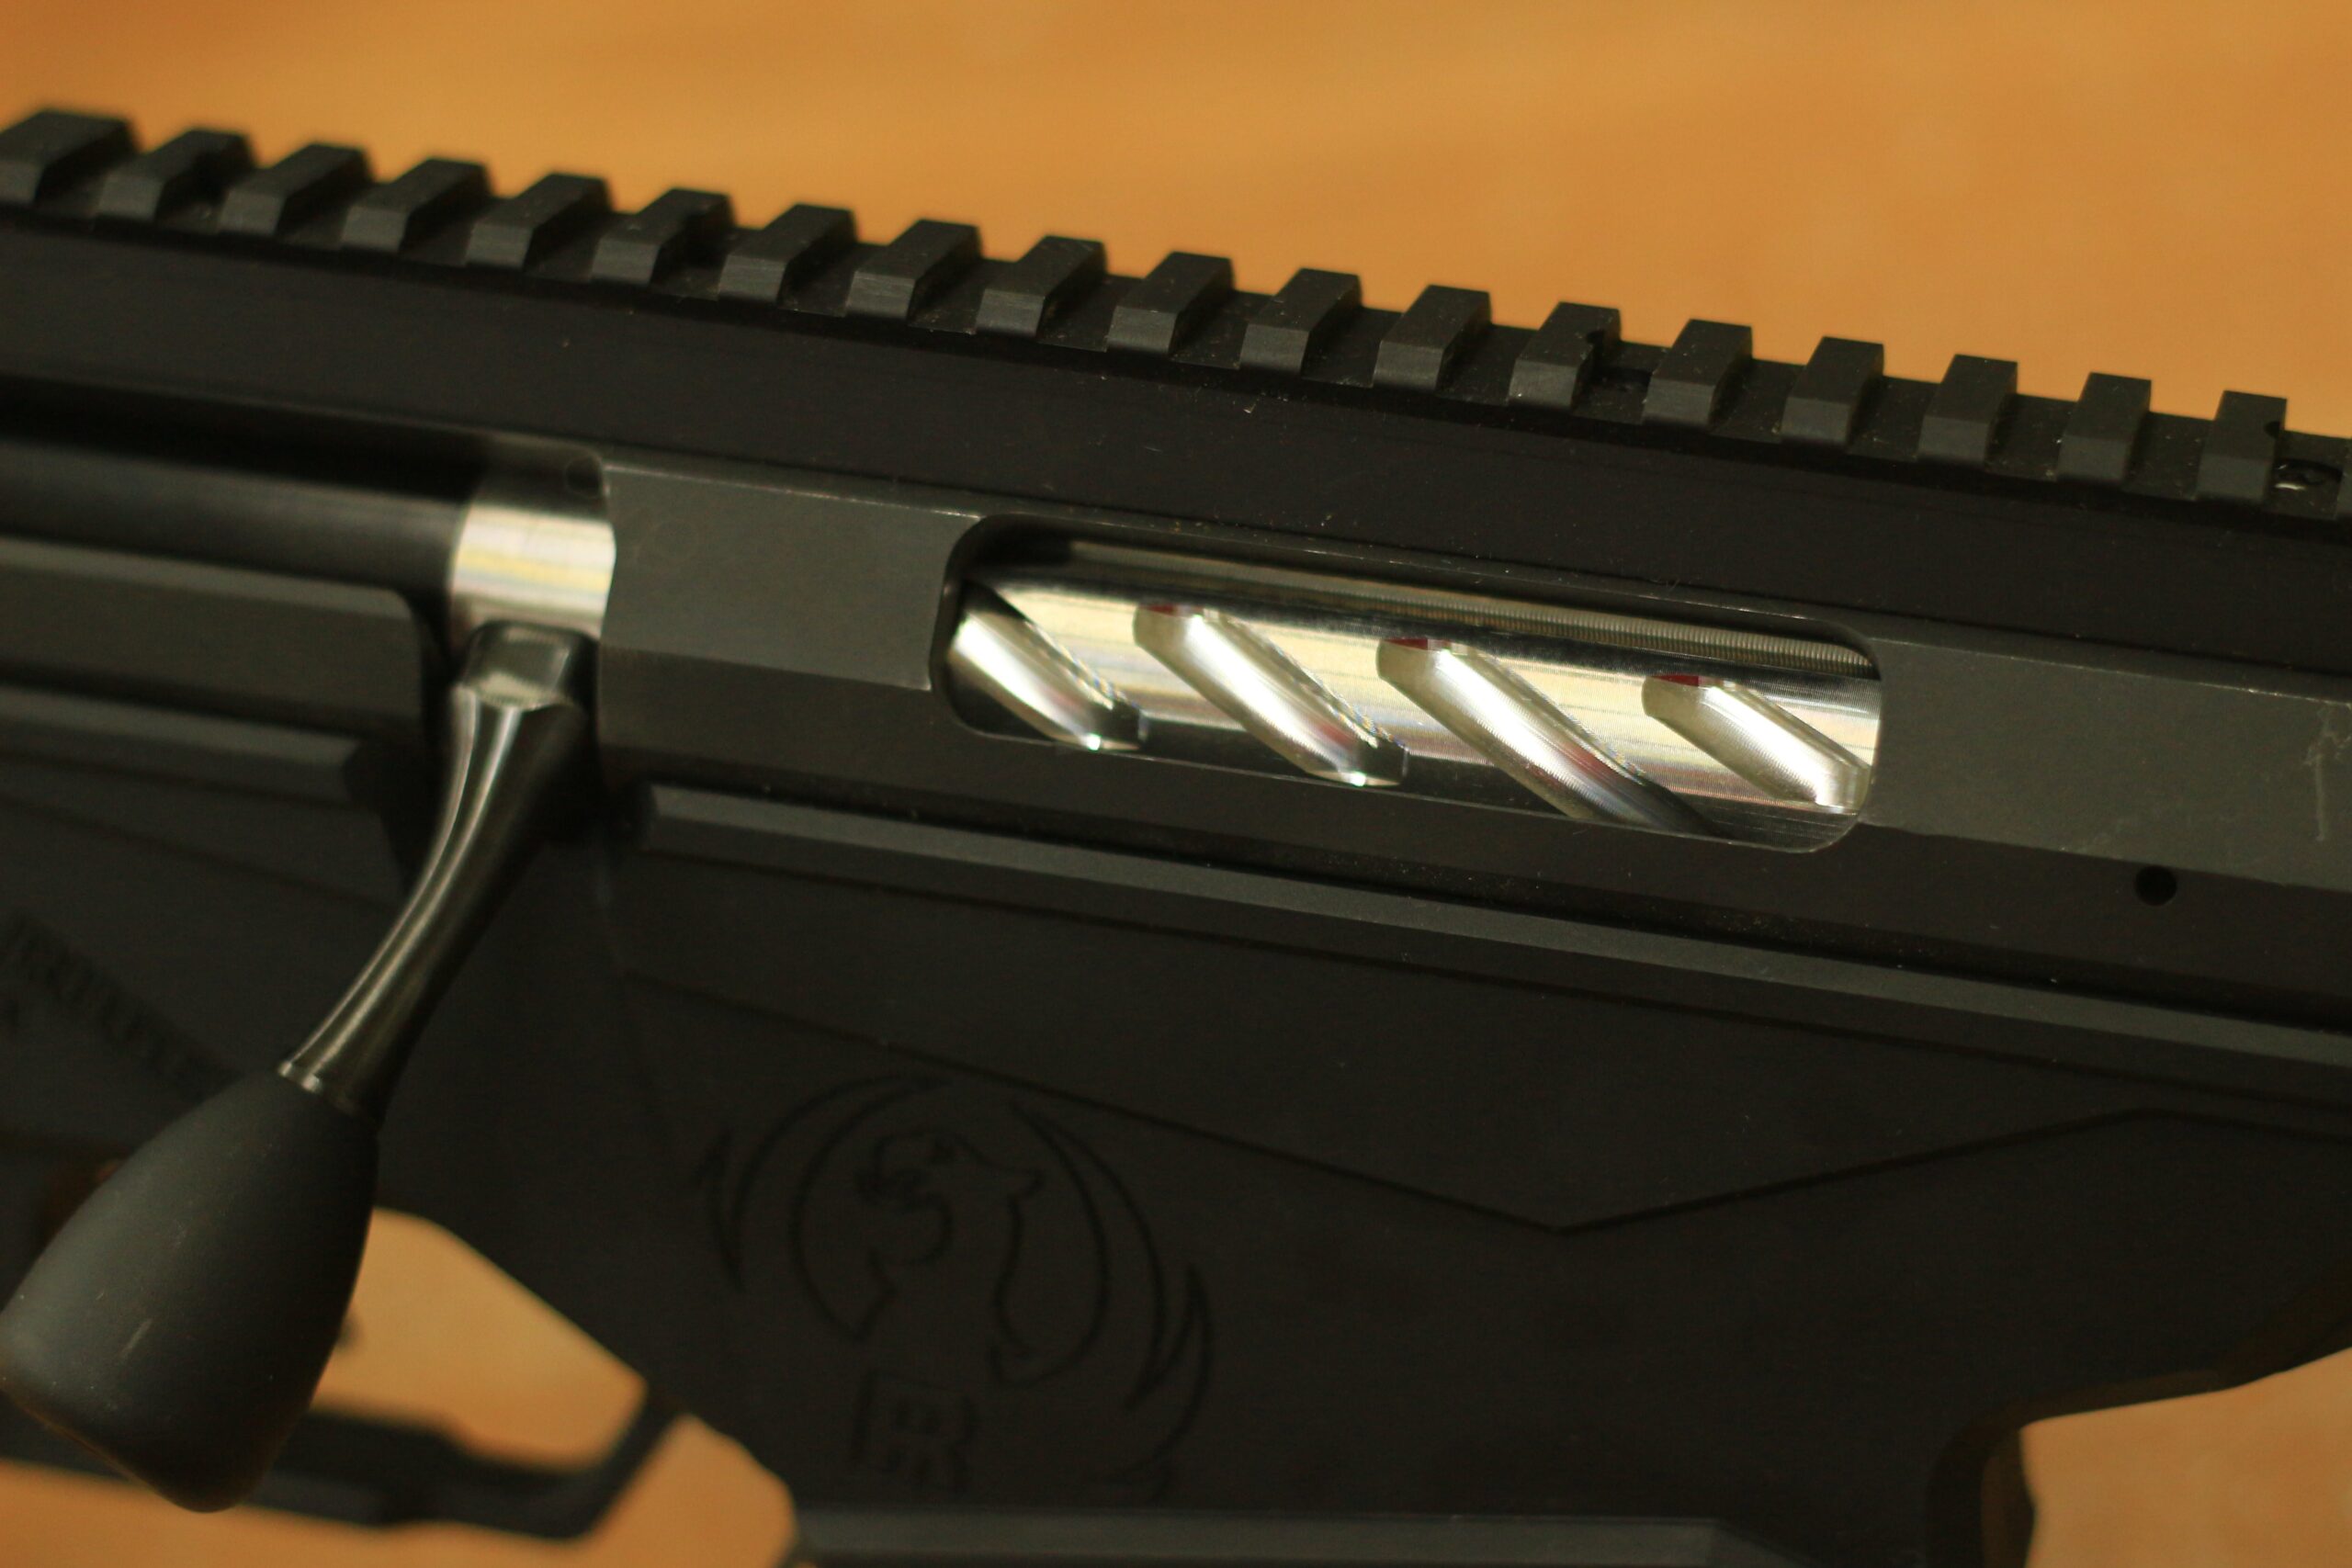
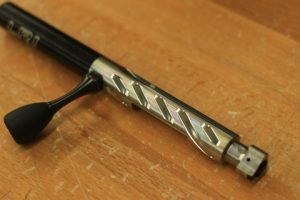
Ruger RPR Short Action (Pattern A):
(Flutes do not invade the axial slot on the bolt body or the magazine feeding/clearance features on the bottom)
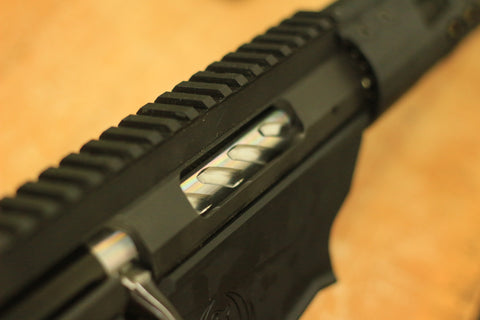
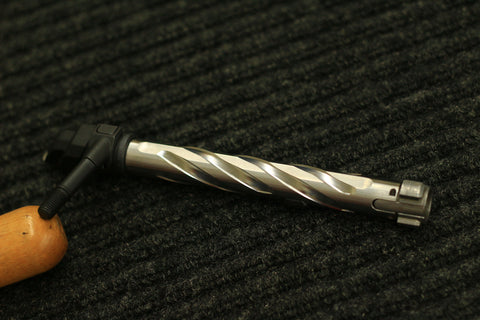
Browning X-Bolt Long Action, Pattern A – High Helix:
Additional information
| Action | REMINGTON M700, REMINGTON M7, REMINGTON M783, WINCHESTER M70 (PF), TIKKA, BERGARA, HOWA 1500, SAKO A7, SAKO 75/85/85M/85FL, COLT LIGHT RIFLE, RUGER AMERICAN, BROWNING X-BOLT, RUGER PRECISION RIFLE, SAVAGE 10/11/12/14/16, SAVAGE 110/111/112/114/116 |
|---|---|
| Pattern | Pattern A – High Helix, Pattern A – Standard Helix, Pattern A – Straight, Pattern B – High Helix, Pattern B – Standard Helix, Pattern B – Straight, Pattern B – Interrupted, Pattern B – Diamond, Wrought Iron, Pattern X, Murder Hornet, RA-RPR, Sako 75 and 85 |
Related products
-
GUNSMITHING SERVICES: AIAW magazine well modification to Rem M700 receiver
$150.00 Add to cart -
GUNSMITHING SERVICES: Striker pin bushing install for bolt action rifle bolts
Price range: $150.00 through $200.00 Select options This product has multiple variants. The options may be chosen on the product page -
GUNSMITHING SERVICES: Tactical bolt knob installation
From $65.00 Configure -
GUNSMITHING SERVICES: Barrel fluting
From $325.00 Configure