GUNSMITHING SERVICES: 8-40 base hole receiver threading
$100.00
Out of stock
Description
An unfortunate consequence of mass-produced guns is a screw hole being machined out of position. Our 8-40 optic base hole upgrade resolves this issue, additionally, we can also add base holes to receivers that were never made for optics. (1903 Spgfld, Mauser, etc…) Many a Springfield and Mauser have suffered a premature expiration date at the hands of a well-intentioned gunsmith discovering the “hard way” just how challenging drilling/tapping case hardened steel can be.
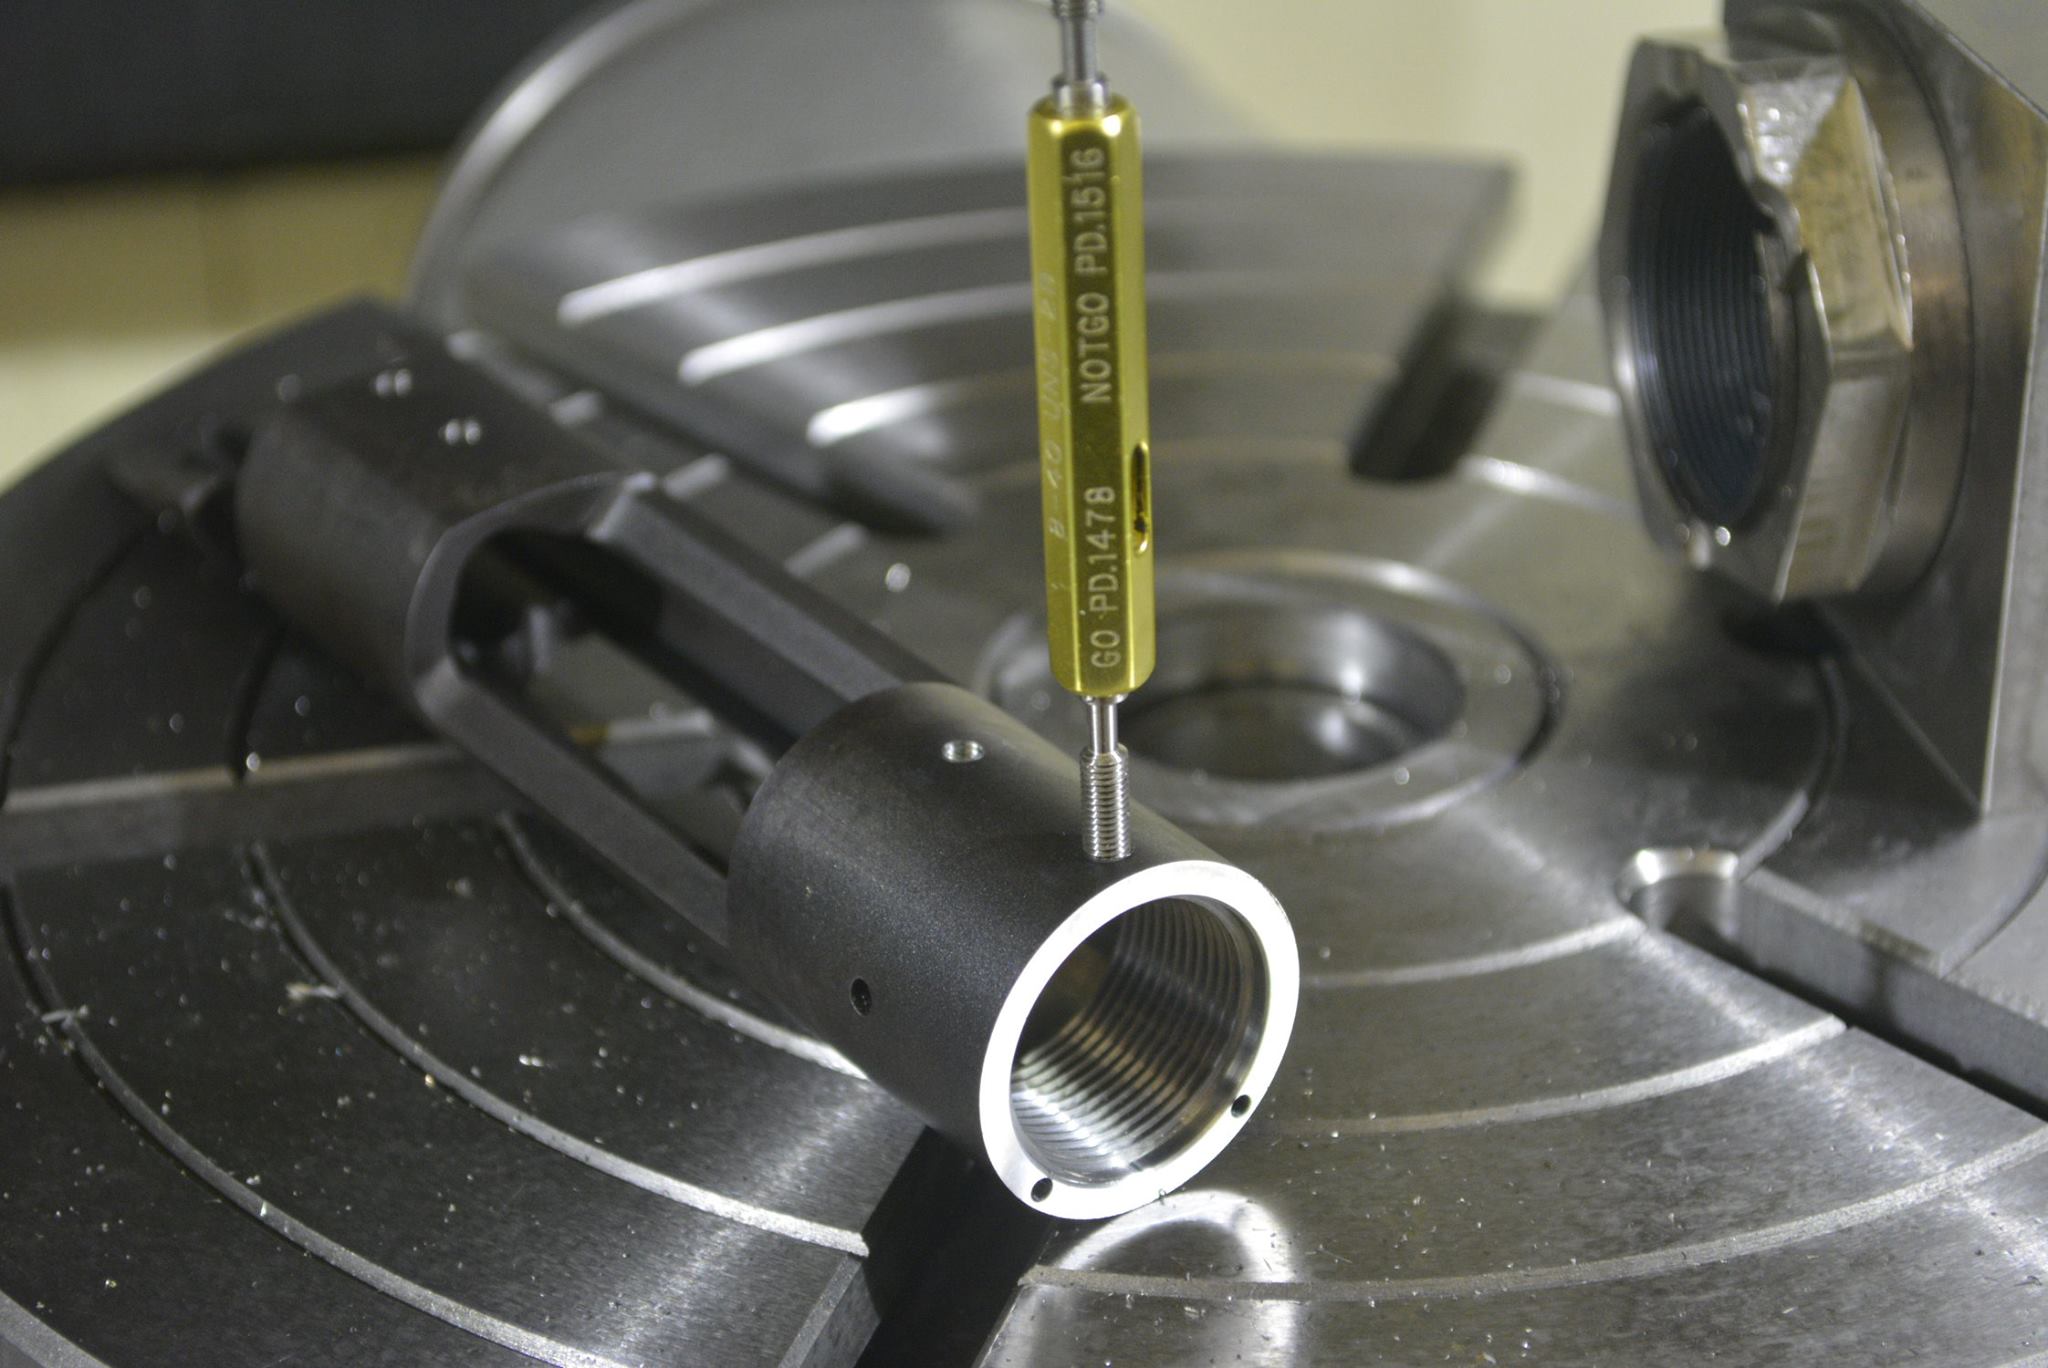
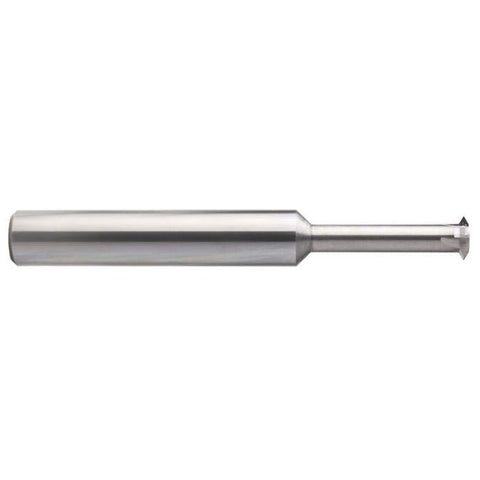
We solve that by getting rid of the drill and tap. Our process uses a more modern approach. Bores are interpolated with a spiral toolpath, mitigating heat and the risk of a tool wandering off location. Threads are created by similar process called “Thread Milling.” The advantage here is the risk of tool breakage and seizure inside the hole is eliminated. If a tool does happen to break, the only consequence is the tool. Replace it, requalify in the machine, and your back in business.
Single point carbide thread mill
As machinists we don’t get the luxury with taps. When a tap breaks it’s almost certain to try and become a permanent part of whatever hole it was being crammed into. That’s the first problem to solve. 2, once you get it out, you cannot just load up a new one and start over because the start point of the lead cutting edge of the tool is never going tobe in the same clock position as the first was was. You are stuck with having to do the remaining holes by hand or altering your program if using a CNC, to skip over the previously tapped holes. You might ask why doesn’t everyone use threadmilling? Cost. It requires a CNC milling center and it’s a large piece of intensive CNC programing that almost demands the use of a CAM (Computer Aided Manufacturing) system to program the routine virtually in a PC computer first. Fortunately, we crossed those boundaries on day 1 of opening our doors.
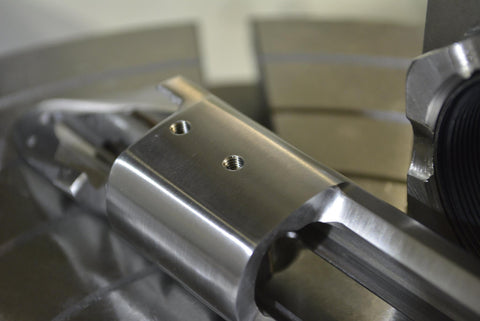
We align the receiver bore parallel to the machine’s work environment. This allows us to correct positional errors of existing holes already in the receiver. The traditional process chases the existing holes with a drill followed by tapping to the larger size. Drills however take the path of least resistance. For reasons already mentioned, it’s not the best practice to correct a location error.
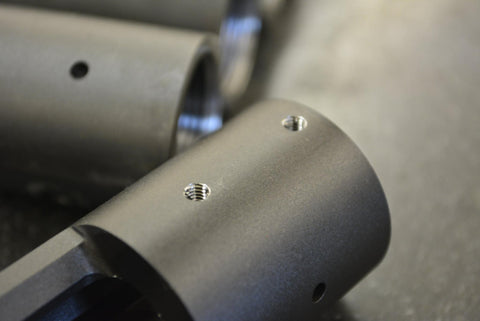
The end result are optic bases that are parallel to the receiver bore. This reduces windage errors, allows optics to remain closer to their mechanical center point, and ensures that bases clamp to the receiver correctly.
This service is offered in two ways. One is a stand-alone where this is all we do. The 2nd is as an elective to our accurizing service. The setup work is where the majority of the cost originates from. The same procedure for base hole work is used to accurize the action as it is the only way to ensure we get it right.
The two different price schedules reflect the setup work involved.
This video shows segments of the thread milling operation:
Related products
-
GUNSMITHING SERVICES: Dual ejector conversion for Remington M700, 721, 722, 40X (centerfire), M7, NXP bolts converted to M16 extractor
$110.00 Select options This product has multiple variants. The options may be chosen on the product page -
GUNSMITHING SERVICES: Receiver blueprinting
Price range: $250.00 through $400.00 Select options This product has multiple variants. The options may be chosen on the product page -
GUNSMITHING SERVICES: Barrel fluting
From $325.00 Configure -
GUNSMITHING SERVICES: Colt/1911 “Brass Check” for front slide
$125.00 Add to cart