GUNSMITHING SERVICES: Barrel fitting
From $375.00
Description
PLEASE READ:
Barrel fitting is a very detail-oriented process. This page is meant as much to inform as it is to offer the service. Please make it a point to contact us directly so that we can discuss your project in detail. As we progress with our new storefront, we will migrate towards more automation where you’ll be able to tailor your rifle completely through the site. It’s coming, but it won’t happen instantly as the background engine is fairly intensive. PLEASE CALL PRIOR TO ORDERING.
1.605.430.2200 is our barreling departments direct line. We are open for calls M-F 8am to 4pm MTN Time.
Thank you!
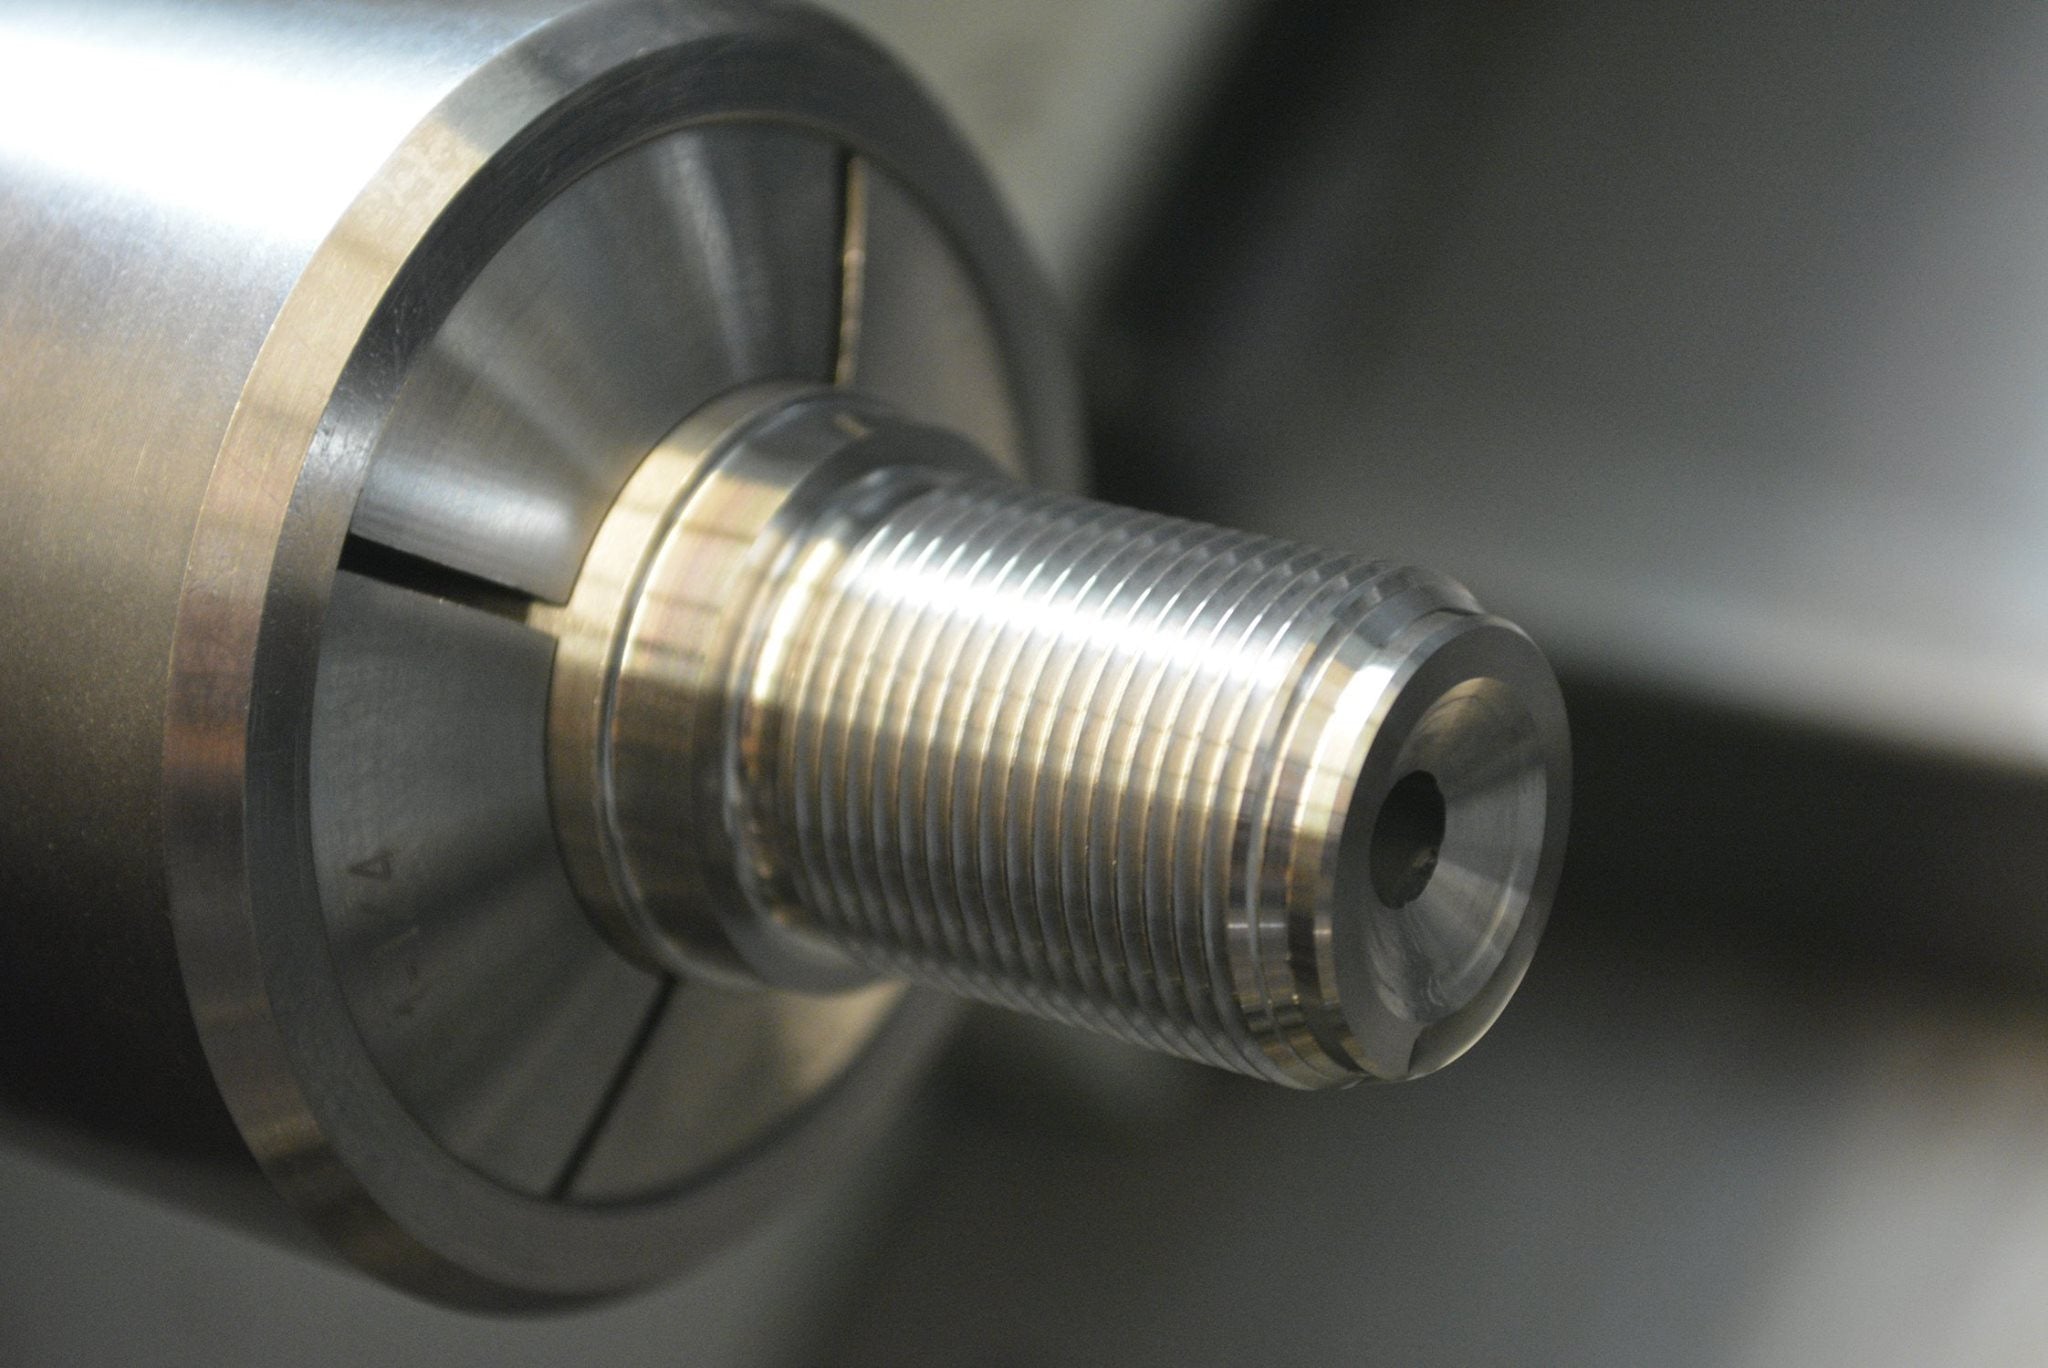
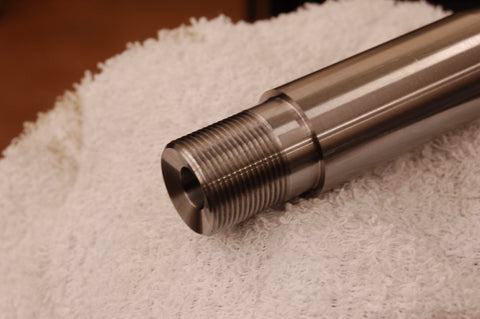
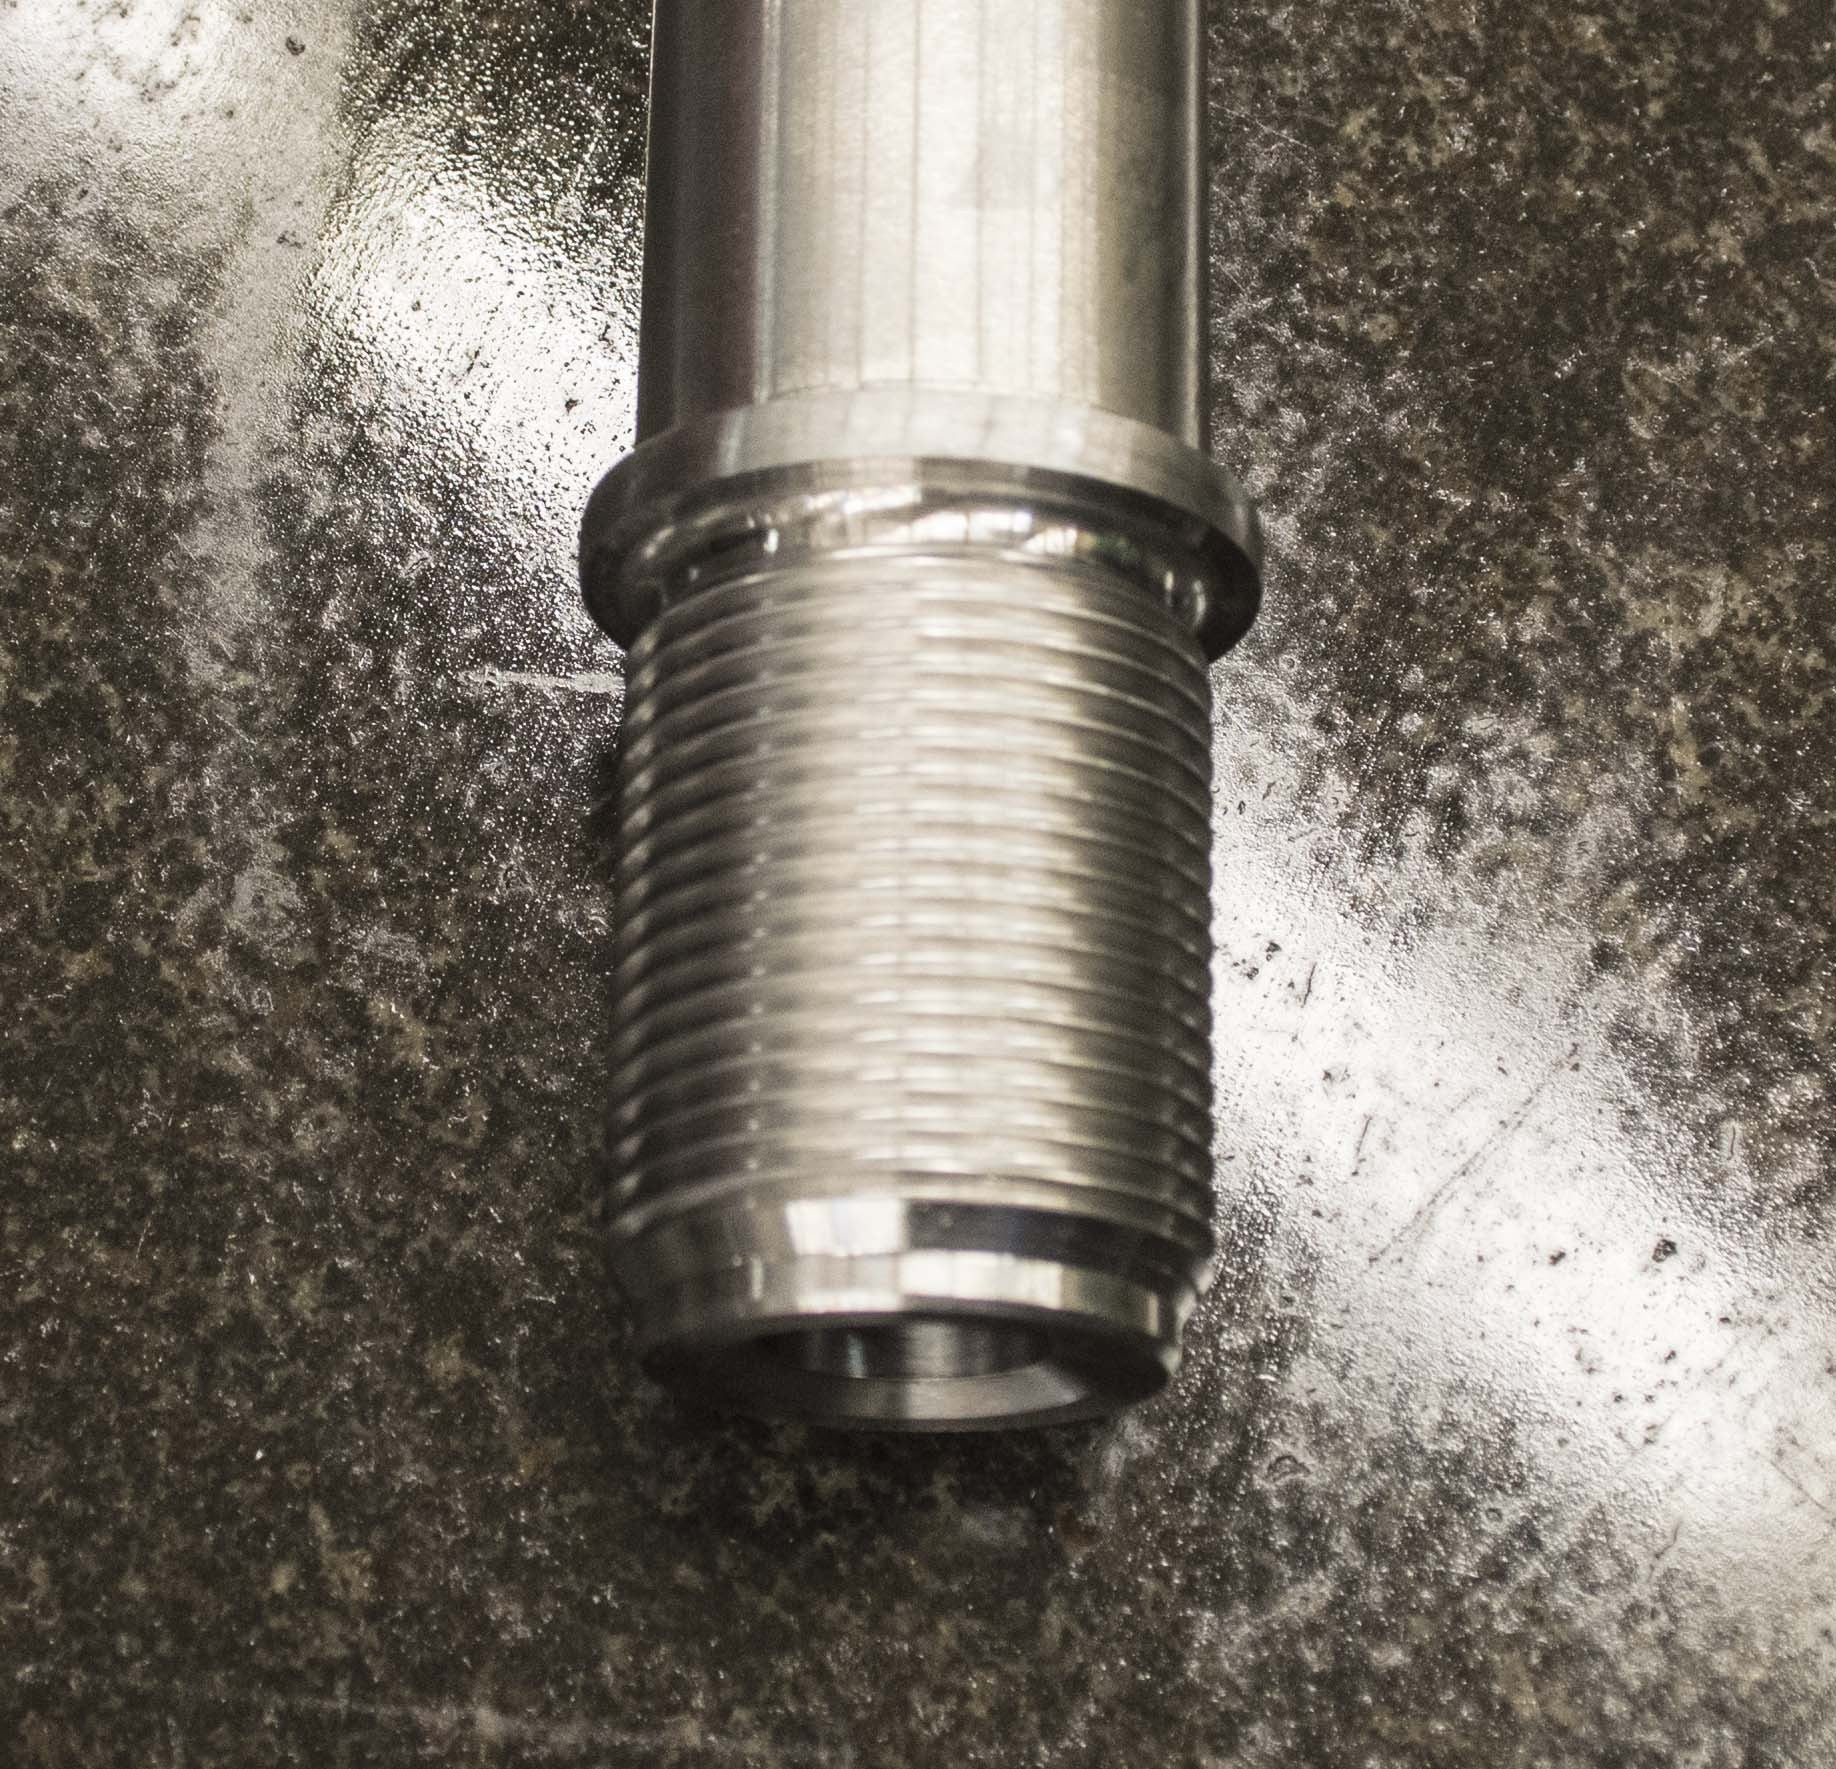
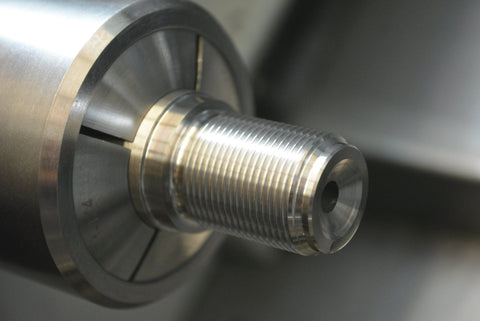
LRI is a pioneer in the use of Automated Computer Controlled Machining centers for precision barrel fitting. Our roots to develop this were planted in 2003. LRI’s process uses the best of what modern machining resources has to offer. Barrel tenons are machined to size with bright surface finish to deliver a silky-smooth fit when mated to the receiver. Threads are fitted to each receiver using a unique programming and tool package that allow for “whisker” passes that bring the pitch diameter to a near mirror image of the receiver ring threads. We have long felt that a minimal thread tolerance produces a more stable joint from the barrel whip created every time the gun is fired. We do confess this is largely opinion based, but it hurts nothing when performed correctly.
Important exceptions:
On OEM standard switch barrel applications such as Accuracy International products, all threads are qualified with certified/traceable hard chromed ring gauges of appropriate thread classification. We qualify the headspace gauge exposure with routinely calibrated instrumentation to ensure headspace meets the safe and appropriate tolerance specified by the Sporting Arms and Ammunition Manufacturers Institute (SAAMI)
“Wildcat” or hybrid cartridges that involve fire forming to alter the shoulder position/angle are often tailored specifically to the type of brass you plan to use. It has been our experience that domestically produced cartridge cases run to the smaller side of SAAMI specification and European manufactured brass leans towards the bigger end. None of this is bad so long as the barrel’s chamber is setup accordingly. To promote good brass life, it we will optimize the headspace dimension specific to the brass being used unless directed otherwise by the client. Our effort is to mitigate case stretch in the critical web area of the cartridge while also ensuring the rifle will safely chamber the cartridge.
Tikka actions:
Tikka T3 actions are narrower than most others and the heavy chamfer feature on the receiver ring limits the barrel cylinder diameter to 1.150″. This is no problem on conventional “all steel” barrels typically used. We simply contour the cylinder OD to the appropriate dimension.
Carbon fiber wrapped barrels cannot be contoured this way. They are designed to be “as is” when fitted. If you are planning to barrel your Tikka action with a carbon wrapped barrel ENSURE you order your barrel with the appropriate cylinder diameter from the manufacturer. LRI will not under any circumstance recontour a carbon wrapped barrel as it creates a serious safety concern and voids any manufacturer’s warranty.
LRI makes a conscious effort to test fire every barreled action assembled here. There have been exceptions, but not many.
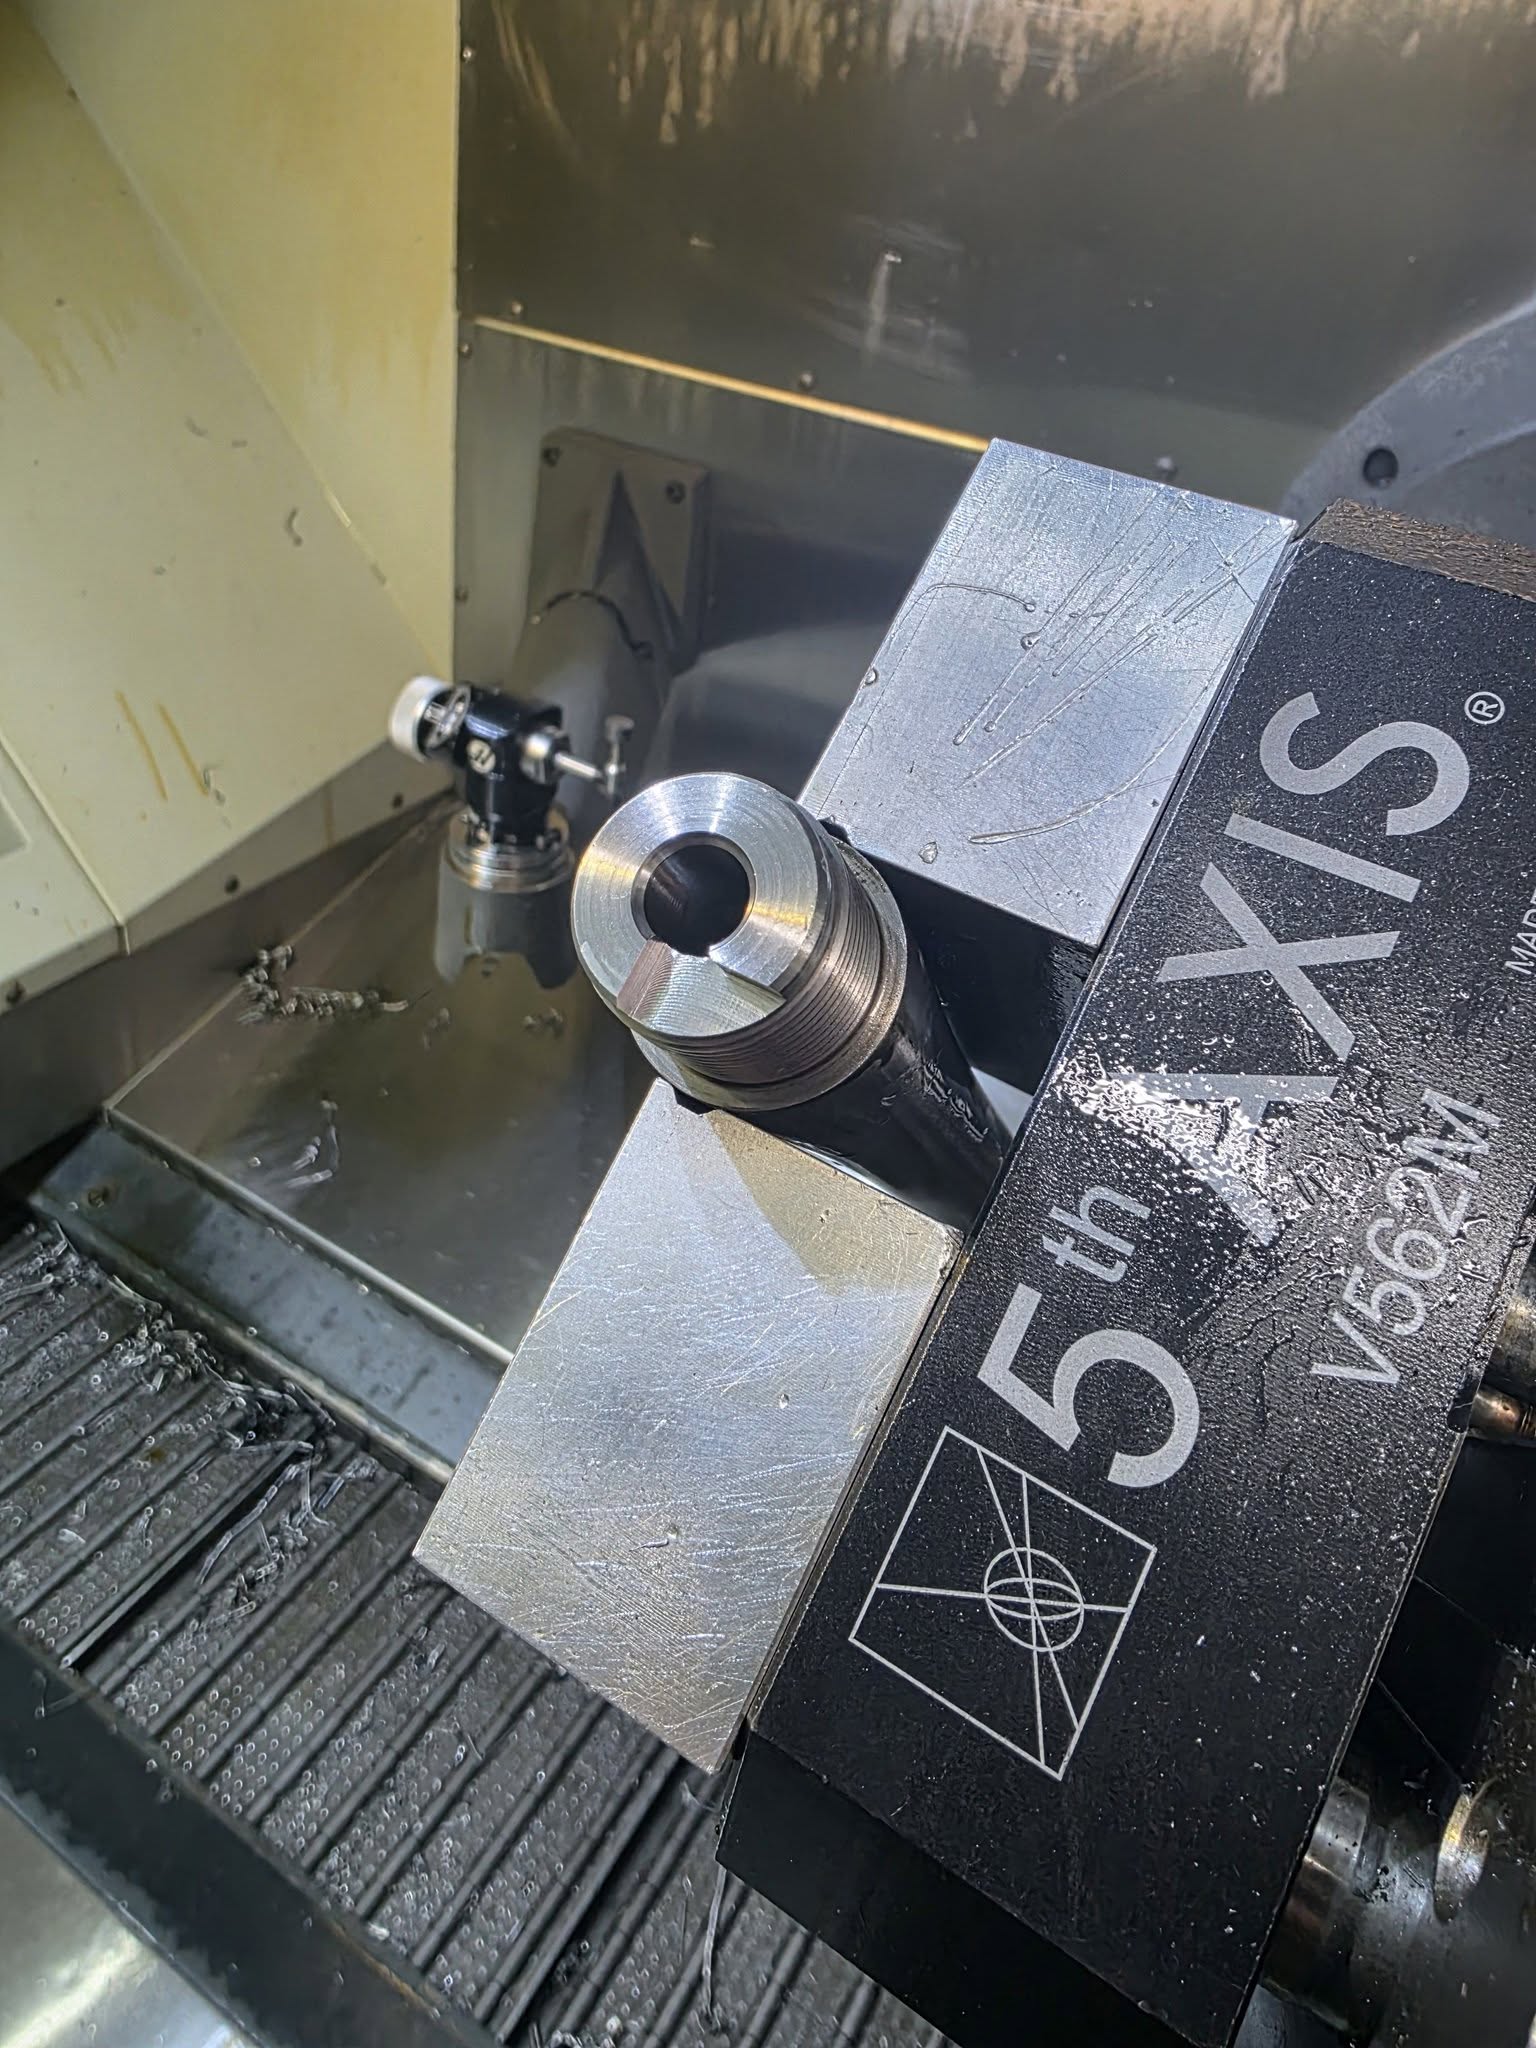
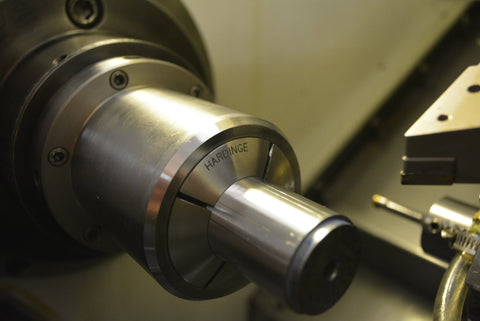
We rely on an indicatable, C-16, hydraulic collet chuck for barrel fitting. The flange hardware shown can be loosened, allowing the entire chuck assembly to float. The hydraulic draw bar is able to move with it. The opposite end of the barrel is supported by additional workholding positioned concentric to the bore center. We get asked about this often. It is a different process, but it has been proven since opening our doors in 2009. The use of a collet provides nearly 360* of radial clamp pressure to the barrel cylinder. Hydraulic draw bars are adjustable with near perfect repeatability. The end result are exceptional surface finish due to the added surface contact and clamping force. Cylinders are taper free and threads present with sterling surface finish along the flanks.
Our chambers are machined on size, concentric/tangent to the bore, and free of surface inclusions. We hone our chambers to a 320 grit finish. We’ve found this answers the need for a chamber to function smoothly and deliver the important “bite” on the brass minimize brass flow/case growth while not being so rough that it “frosts” the brass..
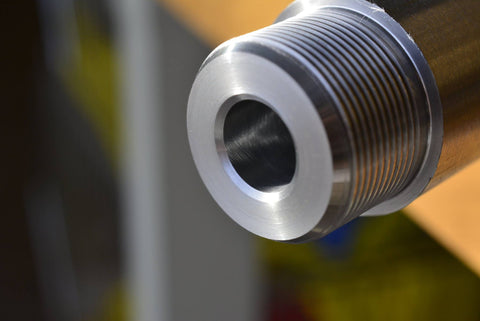
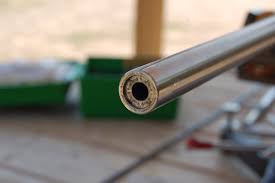
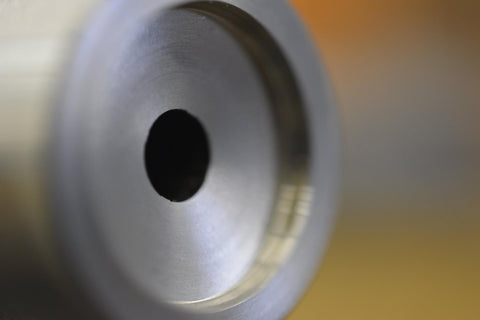
Barrel crowns are single point machined and come in a choice of a traditional 11* target crown, the 11* recessed “hunter” style shown here, or 90* used on legacy-type replica projects. It’s been our experience that none offer any performance advantage over the other.
Muzzle Threading:
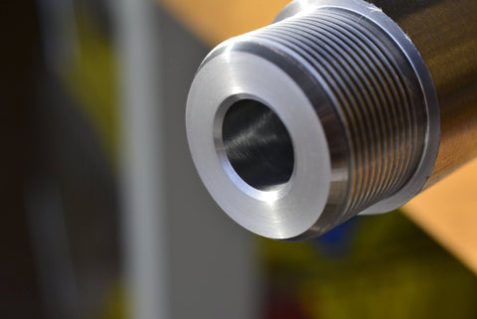
We offer an extensive lineup of muzzle threading options for your barreling project.
Barrel fluting and Finish work:
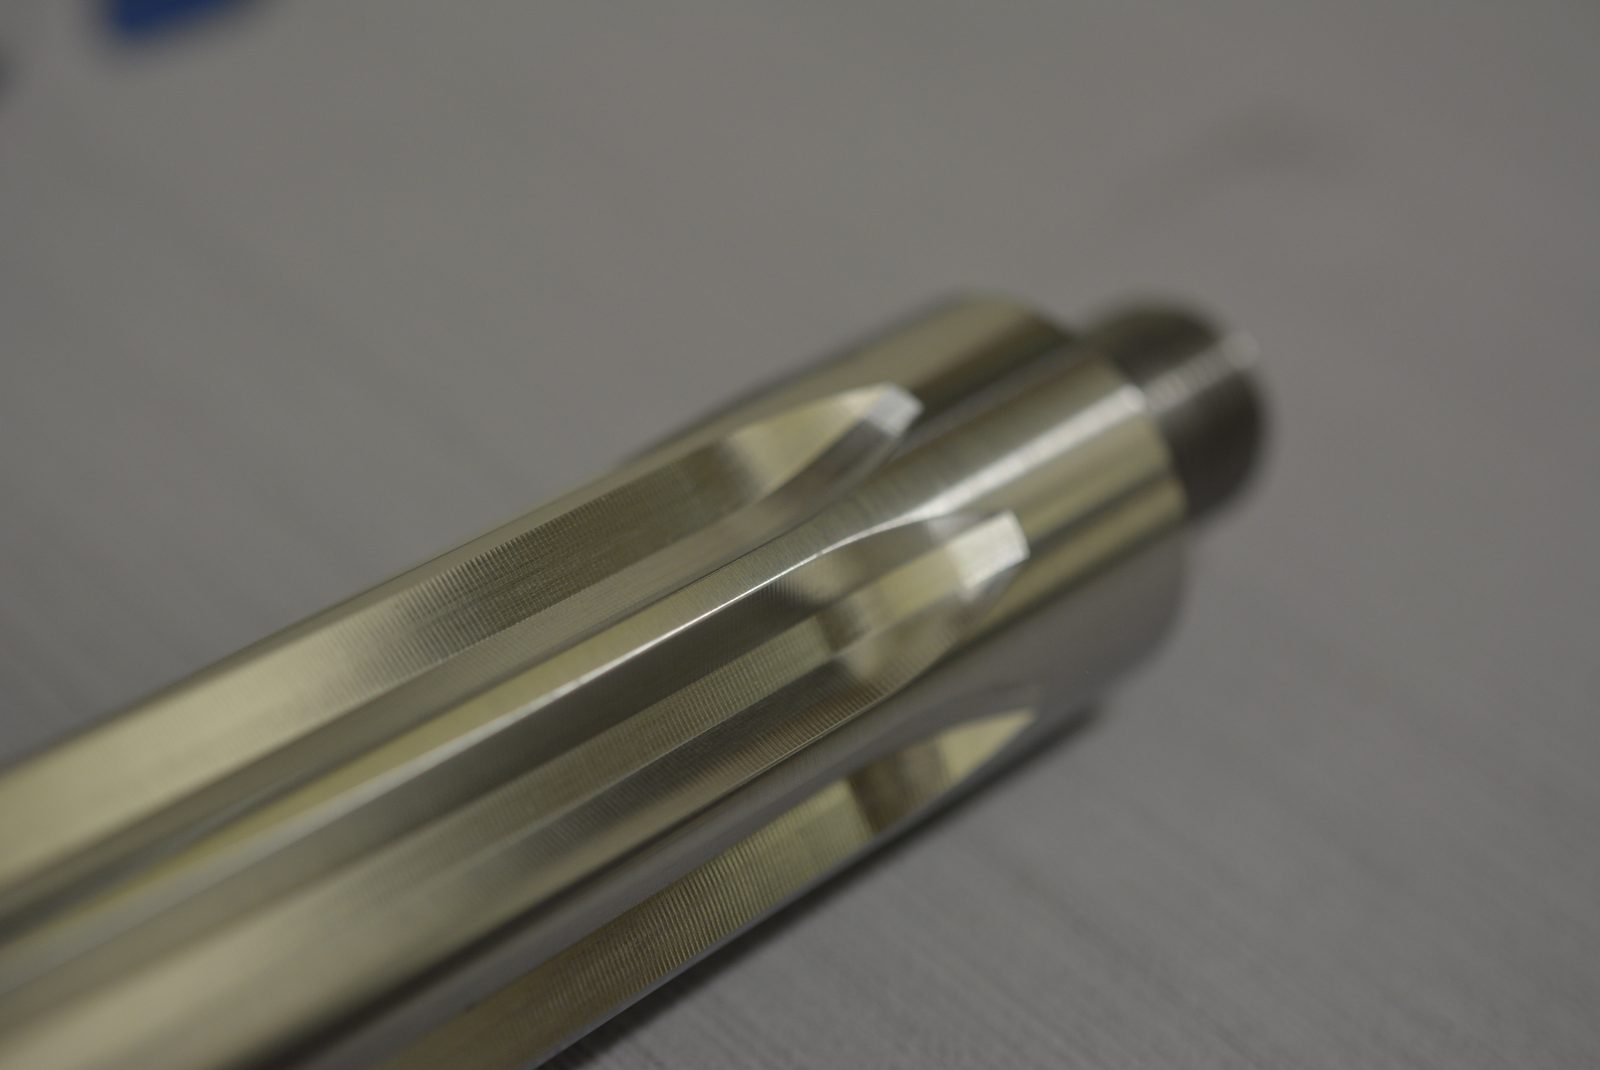
We offer a full line of finishing options for your new barrel.
- Standard 320 grit polish
- Full Mirror polish
- Glass bead blast
- Blast finish and Manganese Phosphate Parkerizing (carbon steel only)
- Hot blue, satin finish (carbon steel only)
- Hot blue, mirror polish
- Cerakote, visit “Cerakote Applications” page for barrel coating our 2nd color applied to flutes option.
Chambering the rifle barrel:
Every LRI reamer is custom made to our specifications. Our tooling is made to a very specific and unique format. For specialty cartridges where we do not have a tool in our library, we are more than happy to order it for you. Our standard practice is to offer our “reamer charge” where we will pay for 50% of the tool’s cost.
The tool and the gauge become the sole property of LRI.
If your project involves a wildcat or variation of a standardized cartridge, please contact LRI directly to discuss the details of what you’d like to do.
Additional information
| Receiver Style | Push Feed SA, Push Feed LA, Controlled Round Feed SA, Controlled Round Feed LA, Rimfire Barrel Fitting, Falling Block |
|---|
Related products
-
GUNSMITHING SERVICES: Receiver blueprinting
Price range: $250.00 through $400.00 Select options This product has multiple variants. The options may be chosen on the product page -
GUNSMITHING SERVICES: Time/TIG and Time advance_Install handle to M700
Price range: $150.00 through $250.00 Select options This product has multiple variants. The options may be chosen on the product page -
GUNSMITHING SERVICES: ARC Magazine well modification to Rem M700 Receiver/ARC Mausingfield
$55.00 Add to cart -
GUNSMITHING SERVICES: Bolt jeweling
Price range: $100.00 through $175.00 Select options This product has multiple variants. The options may be chosen on the product page