GUNSMITHING SERVICES: Blueprinted barreled action service packages
From $500.00
Description
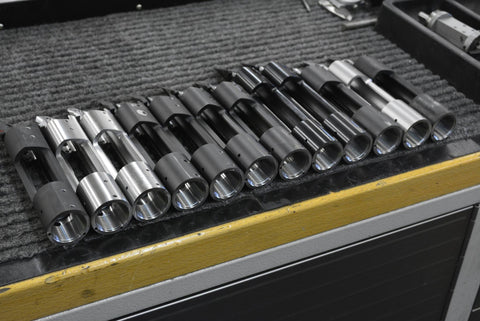
Shortly after opening the doors to our new facility in 2011, LRI started a Remington M700 bolt fluting Group Buy on the Sniper’s Hide web forum. It really opened our eyes on what is possible with work ethic and modern assets. TWO people processed OVER 600 bolts in a 5-week period! Most were received, fluted, coated, and shipped the same day.
In 2013 we began a new venture. Blueprinting, barrel fitting, fluting, and cerakote application. It grew into the largest, longest duration Group Buy in the history of the Sniper’s Hide site. (over a decade) In 2018 we brought home to our website.
Present day:
We now call these our “Barreled Action Service Packages.” With the launch of our new website, we have expanded from Remington to also include Winchester, Mauser, and Bergara actions. It covers short, long, left, and right-handed actions with any appropriate bolt face and extractor configuration. Our rates are no longer based on “mass consumer participation numbers” as the price filter. Instead, it is now a collection of elective services you decide on. Rates are based on the number of services your project requires. The more services you choose, the greater the per service discount becomes.
The new work environment of the website allows us to consolidate parts and services. You’re no longer required to jump back and forth. When ordering a barrel blank, it’s important to know that these are made to order. Our lead times are typically between 6 and 8 weeks for a barrel blank.
Once we have parts in hand, we typically have the entire job processed in about 3 to 6 weeks. Our more “fringe” barrel fluting options, Pattern X and Murder Hornet, factor into this due to high demand and increased cycle times.
Services:
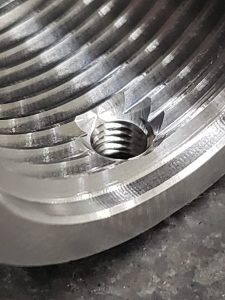
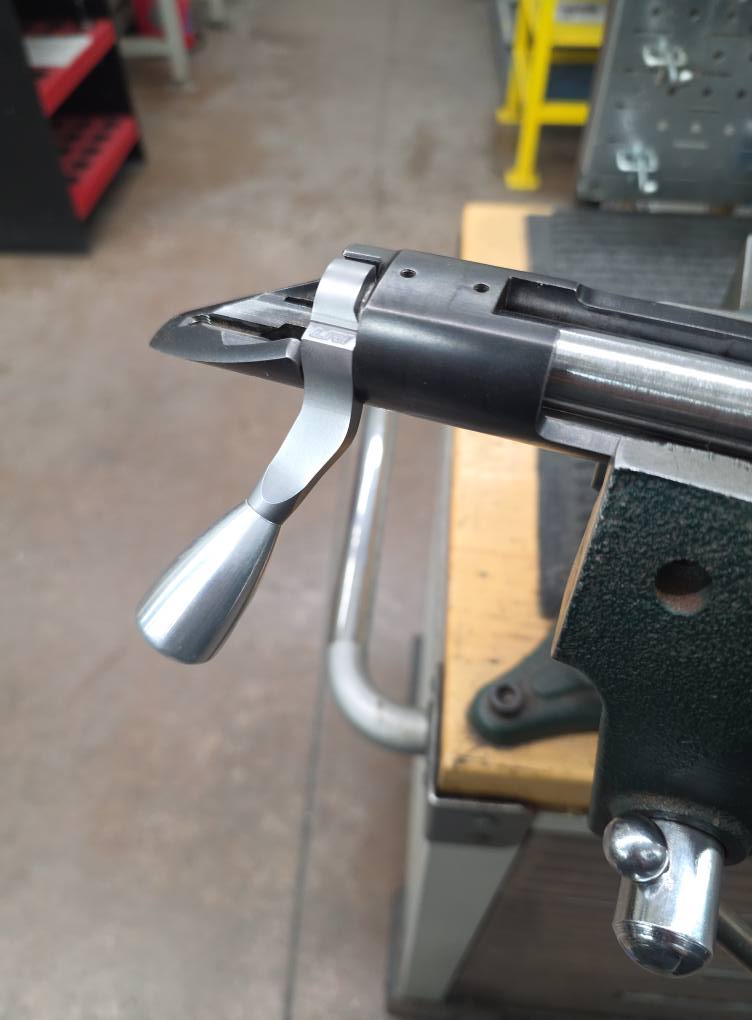
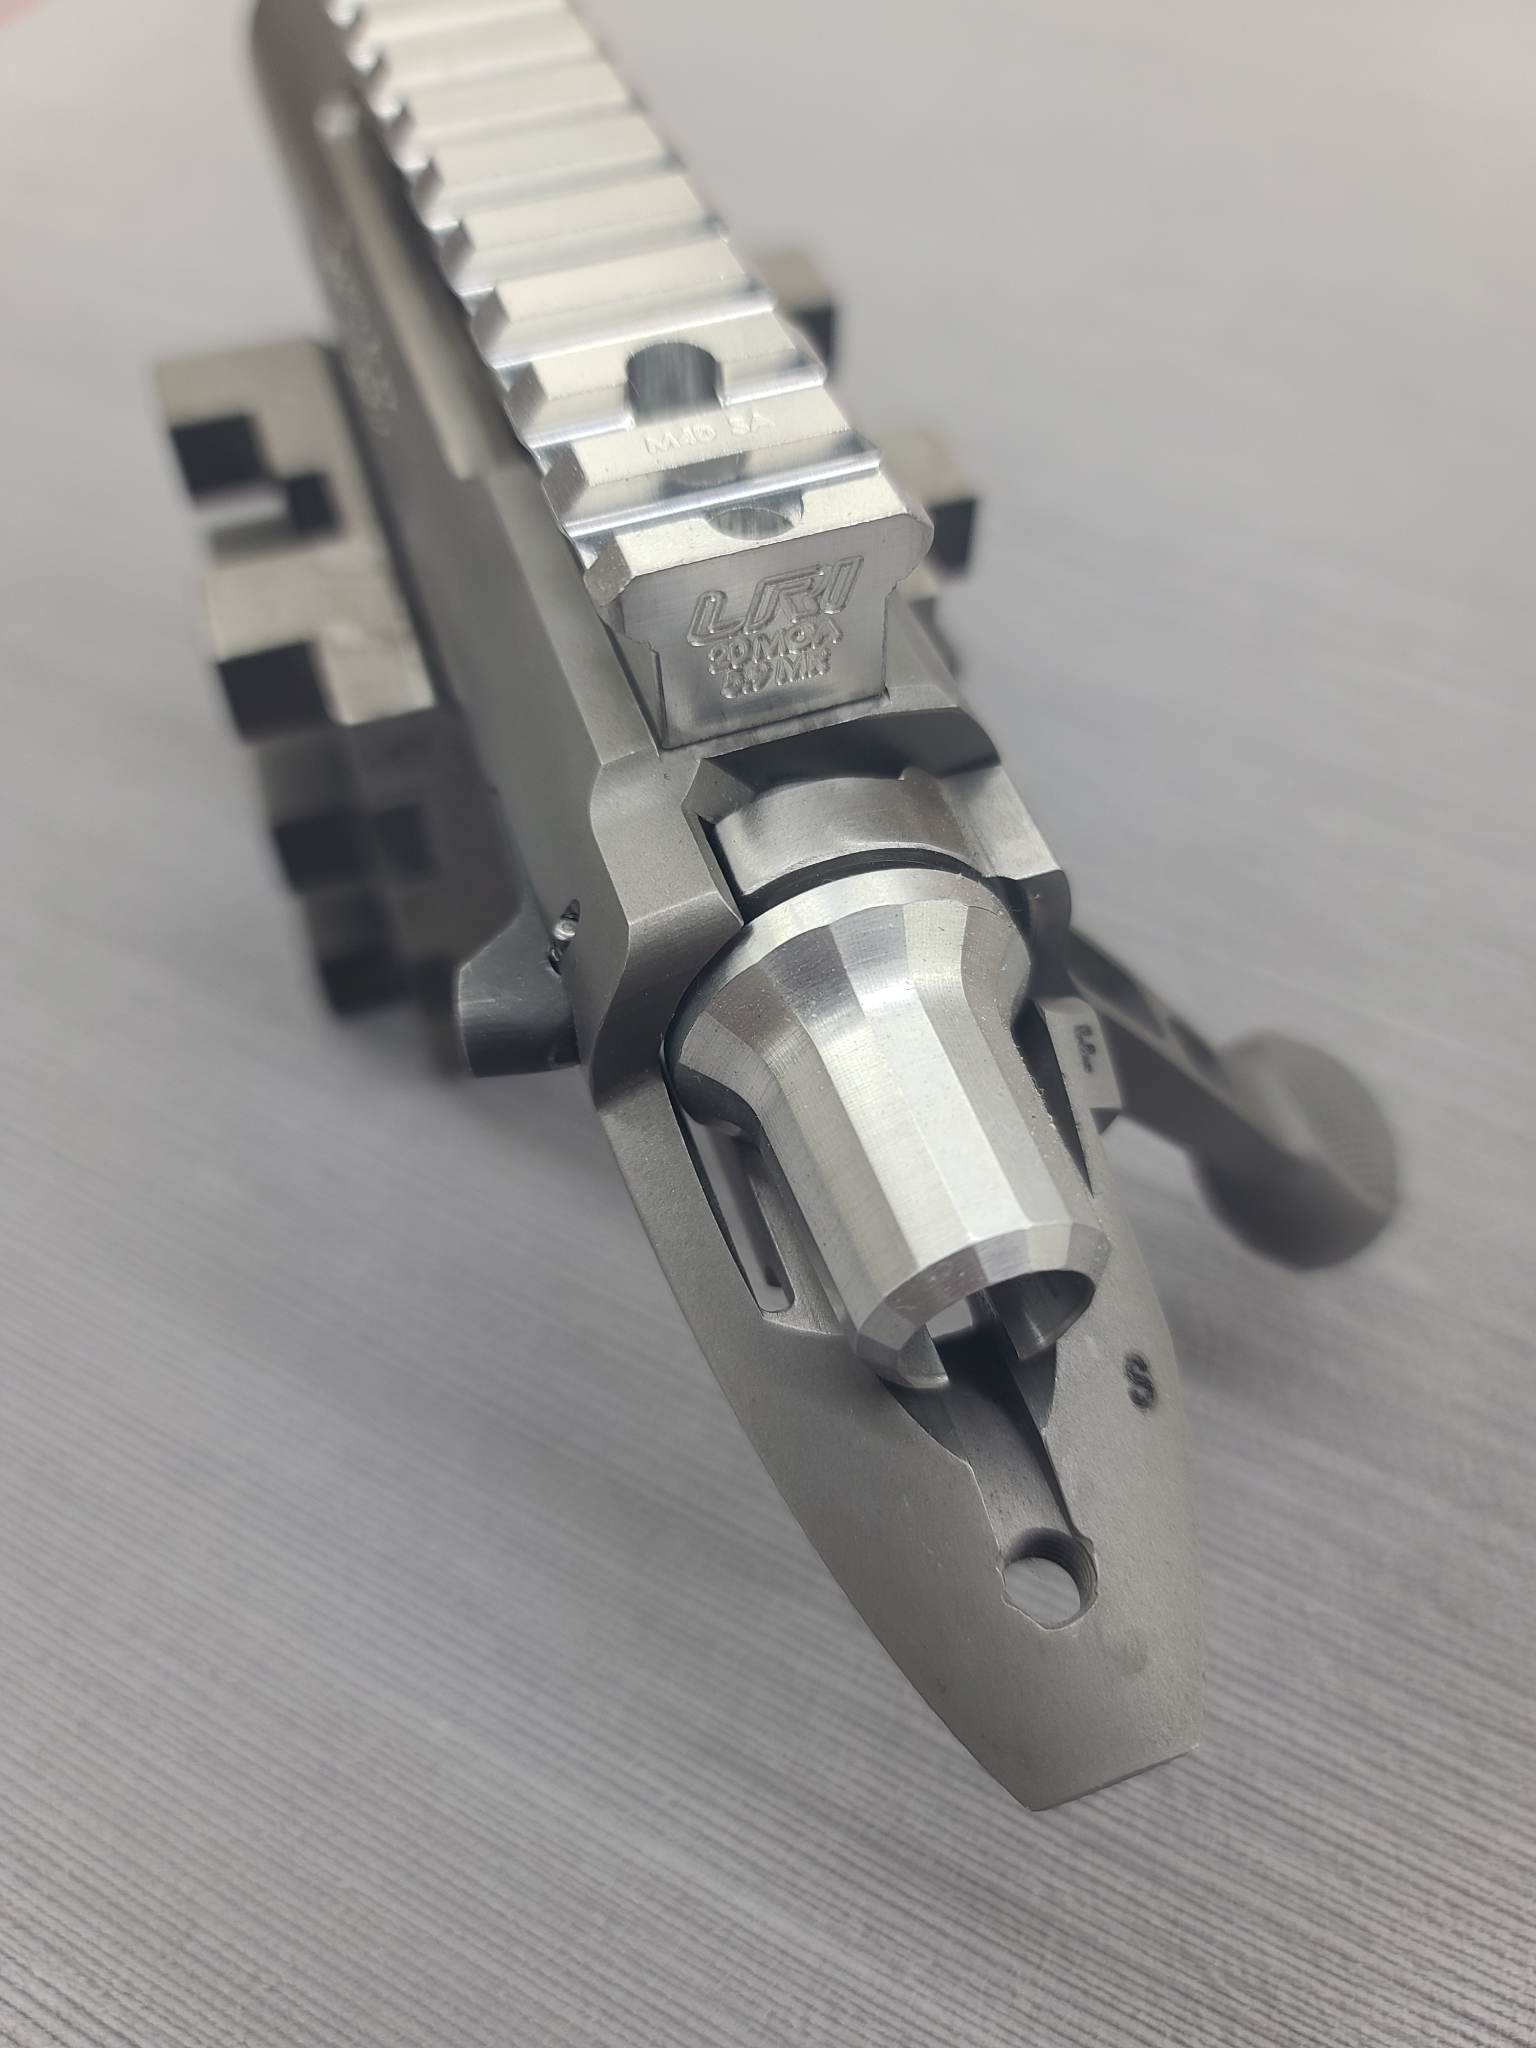
5-Axis Receiver and Bolt Blueprinting:
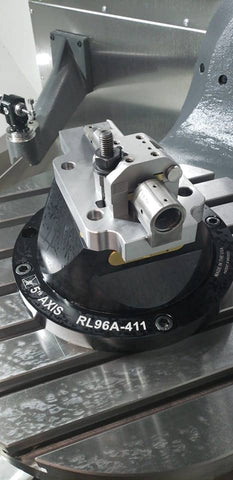
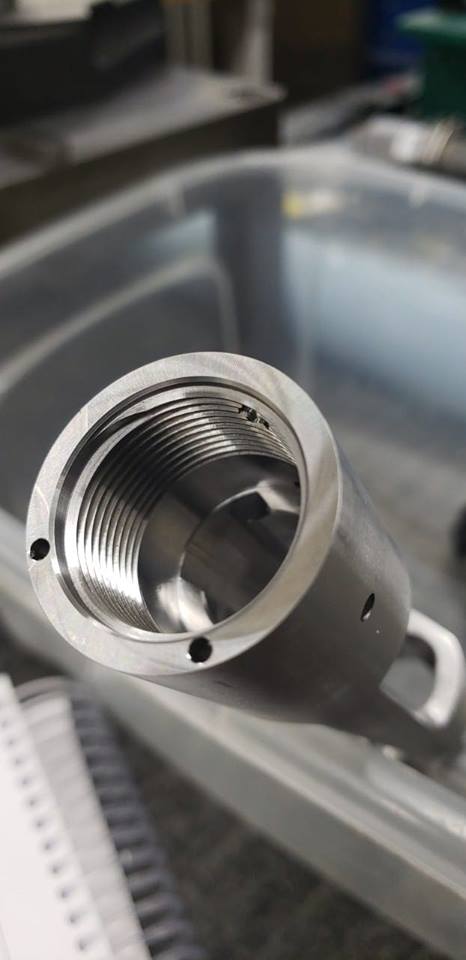
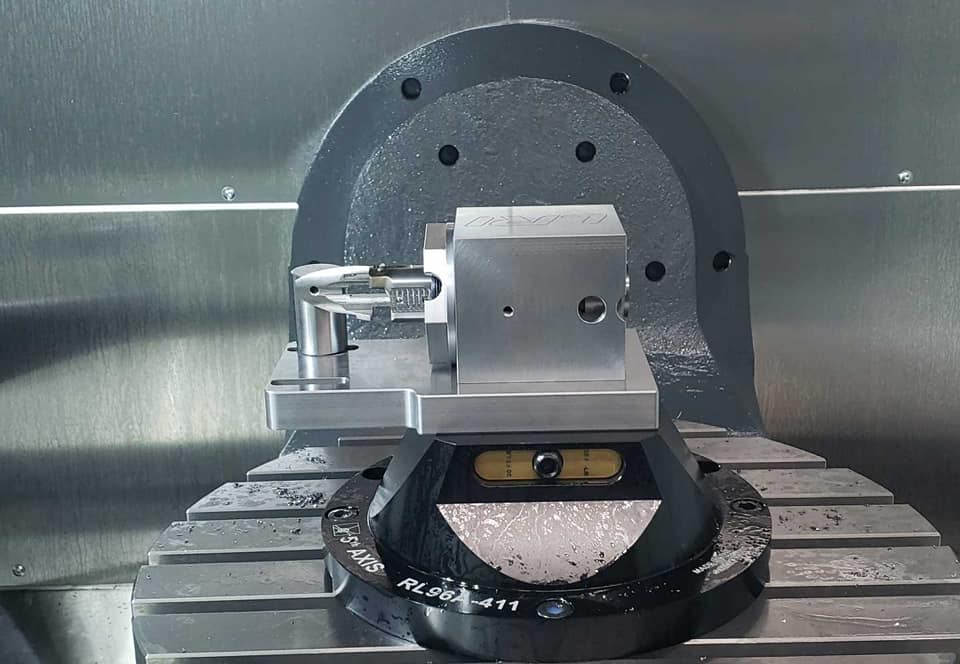
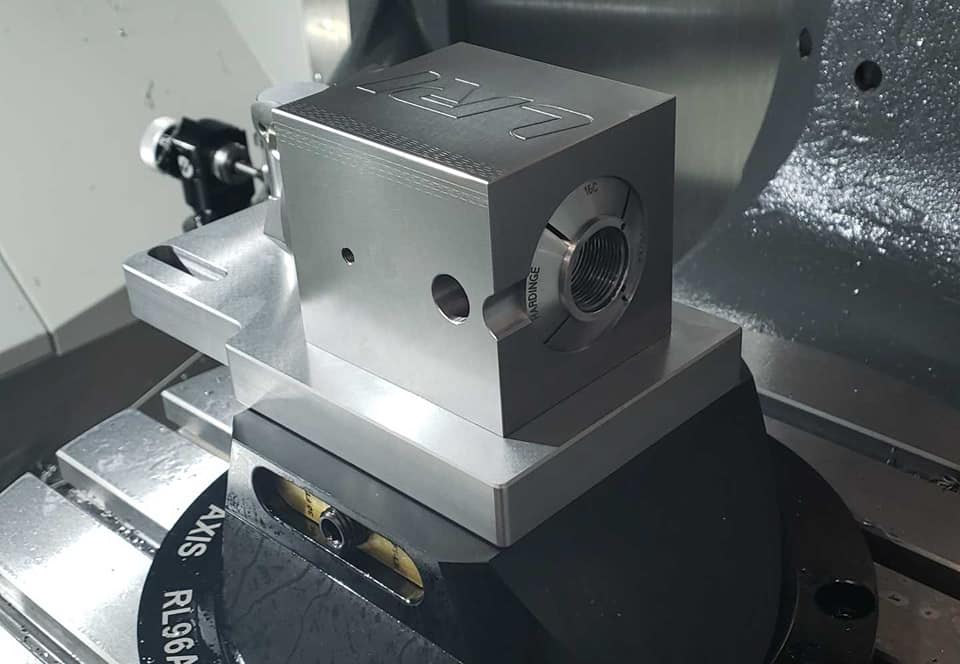
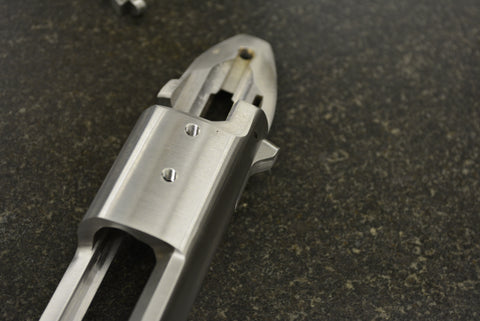
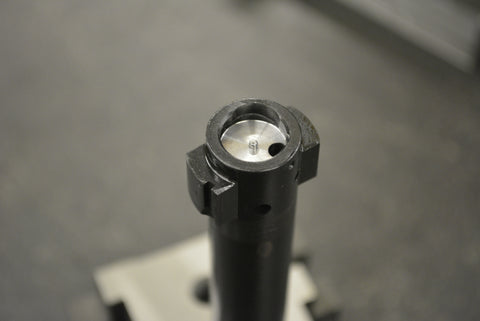
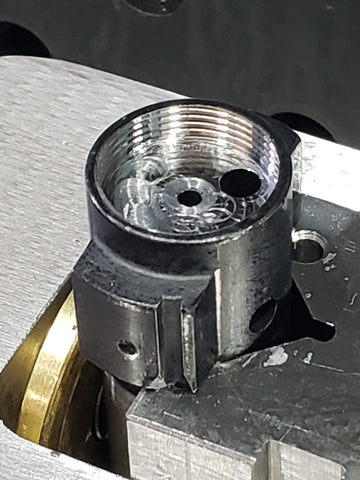
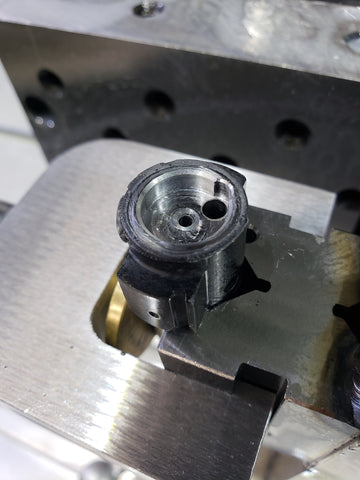
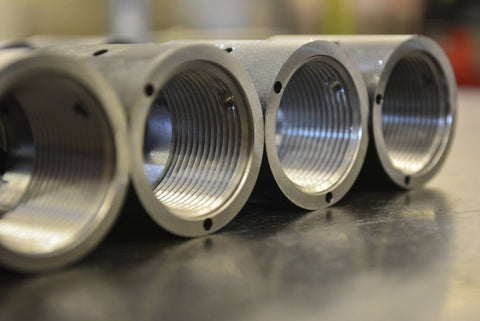
Blueprinting is also referred to as “truing” or “accurizing”. It is a machining operation aimed at improving the accuracy potential of a factory bolt action receiver by correcting small errors from mass production. LRI’s roots ushered the modern era by migrating the work from a manual lathe to CNC milling centers beginning as far back as 2003. (Before LRI was a business, this process was experimented with at Nesika Bay Precision) From those early days, it’s evolved onto 5-axis machining centers. A process we are proud to say is an industry exclusive and developed entirely in house.
Advantages of our Blueprinting process:
- Diamond honed receiver bore for a uniform, inclusion free surface
- Reduction in tool library mitigates the risk of tolerance stacking (One tool can now face the receiver, ID bore the thread ring and surface the lug abutments)
- Consolidated machining operations improve dimensional accuracy by eliminating multiple setups in multiple fixtures
- Exceptional parallelism between bolt and receiver lug surfaces
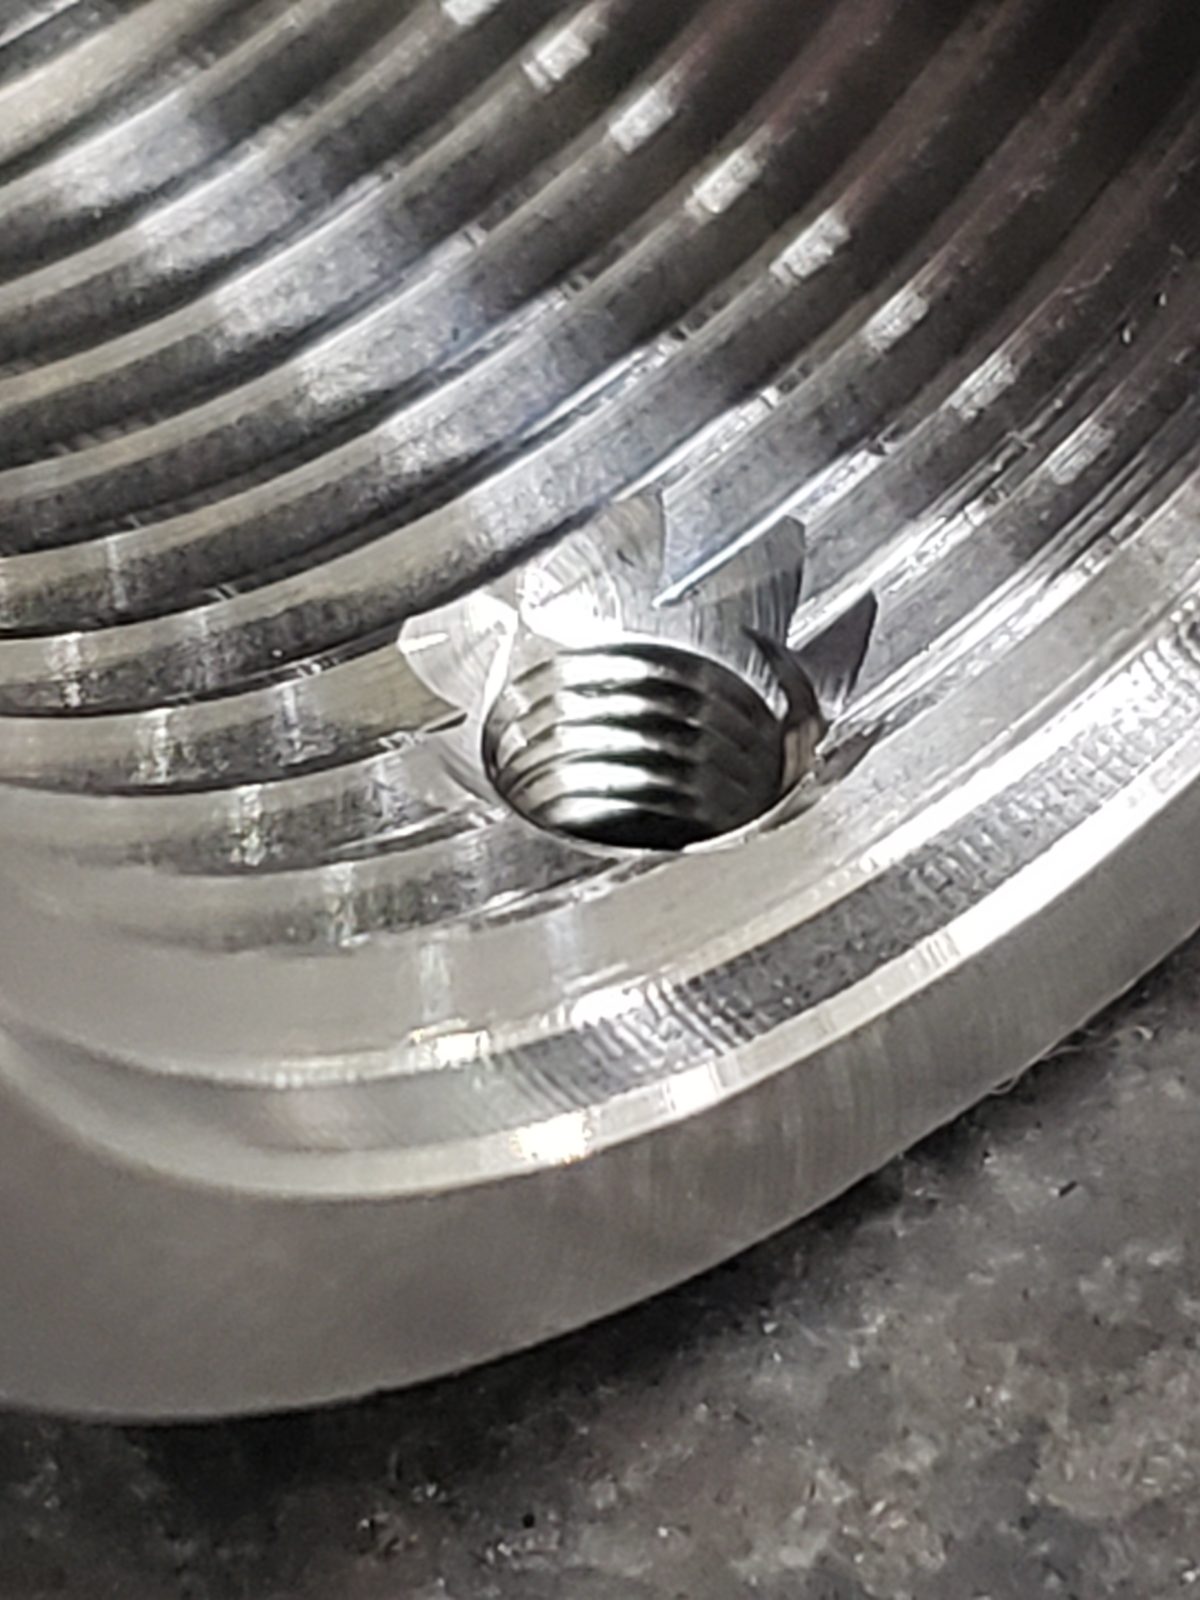
- Addition of a “Higbee” lead thread to eliminate the risk of a torn or galled thread start
- Avoidance of part distortion from work holding
- Pinned recoil lug to ensure repeatable clocking in bedded stocks when changing barrels (Offered only with LRI recoil lugs)
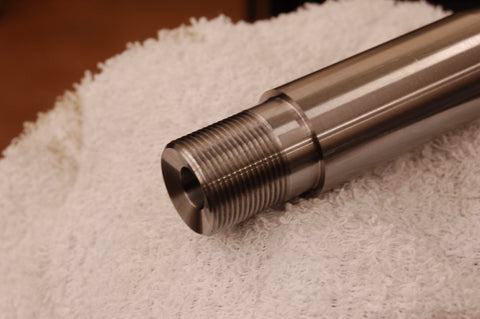
- Taper free receiver ring threads with the use of single-point thread milling
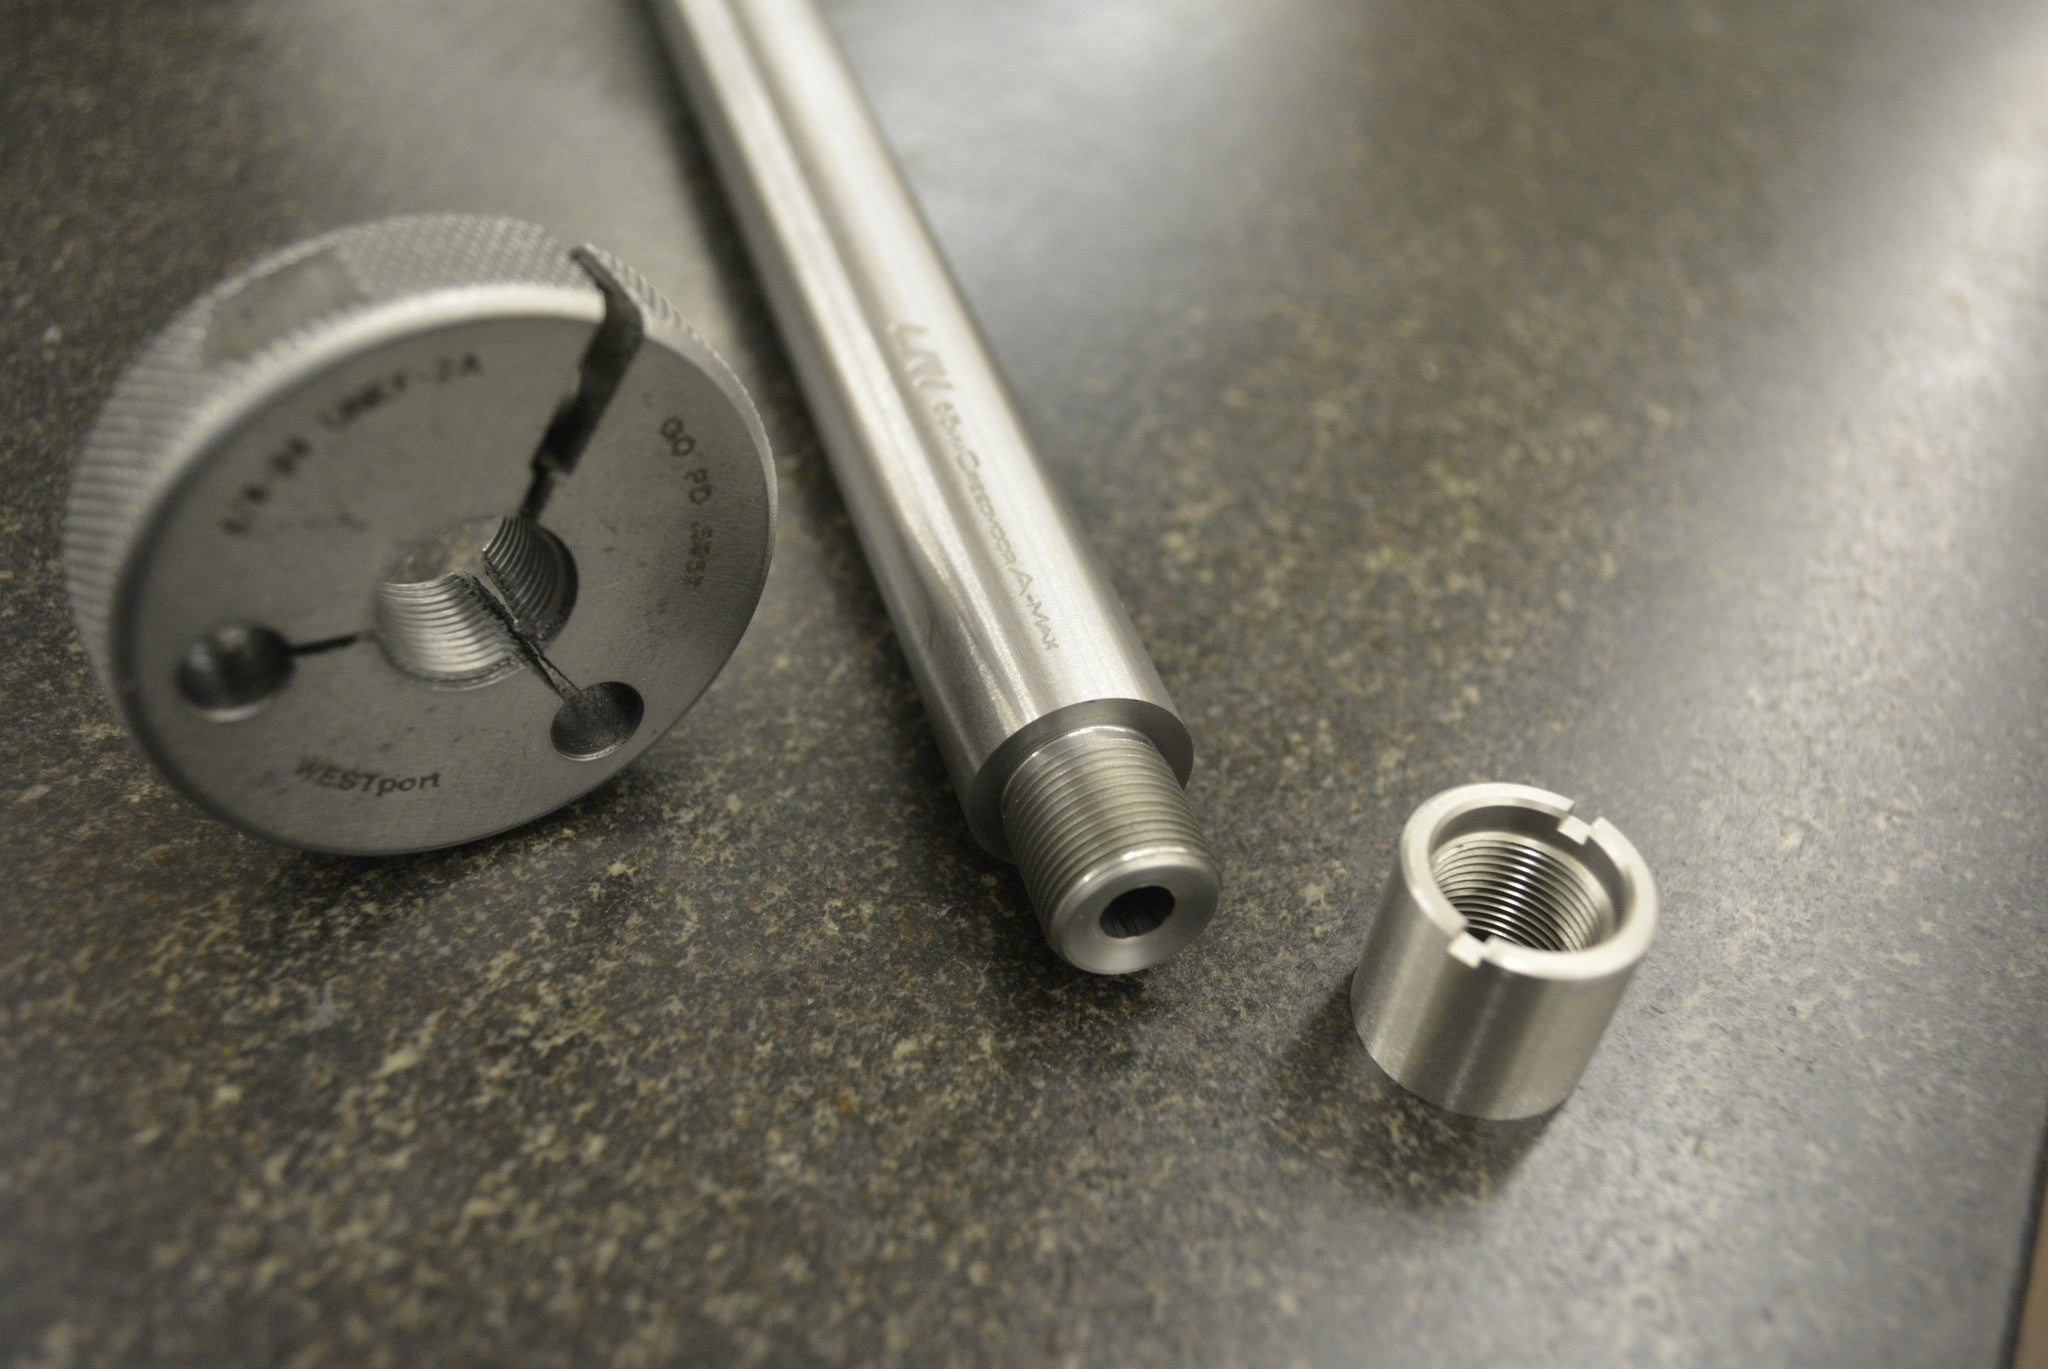
- Standardization of thread size qualified with in-house metrology and gauging
- Misaligned optic base hole correction
- Exceptional surface finishes with the use of shrink fit tooling and dedicated work holding
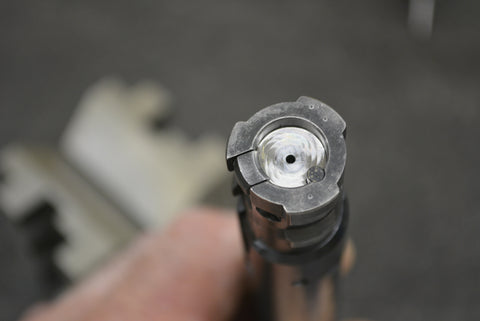
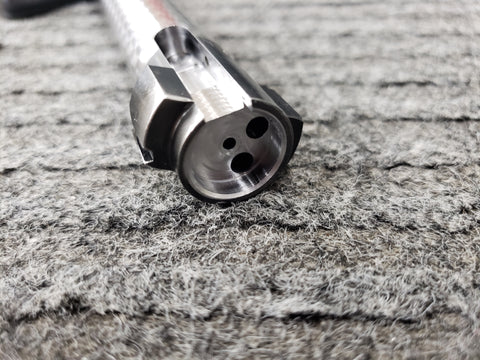
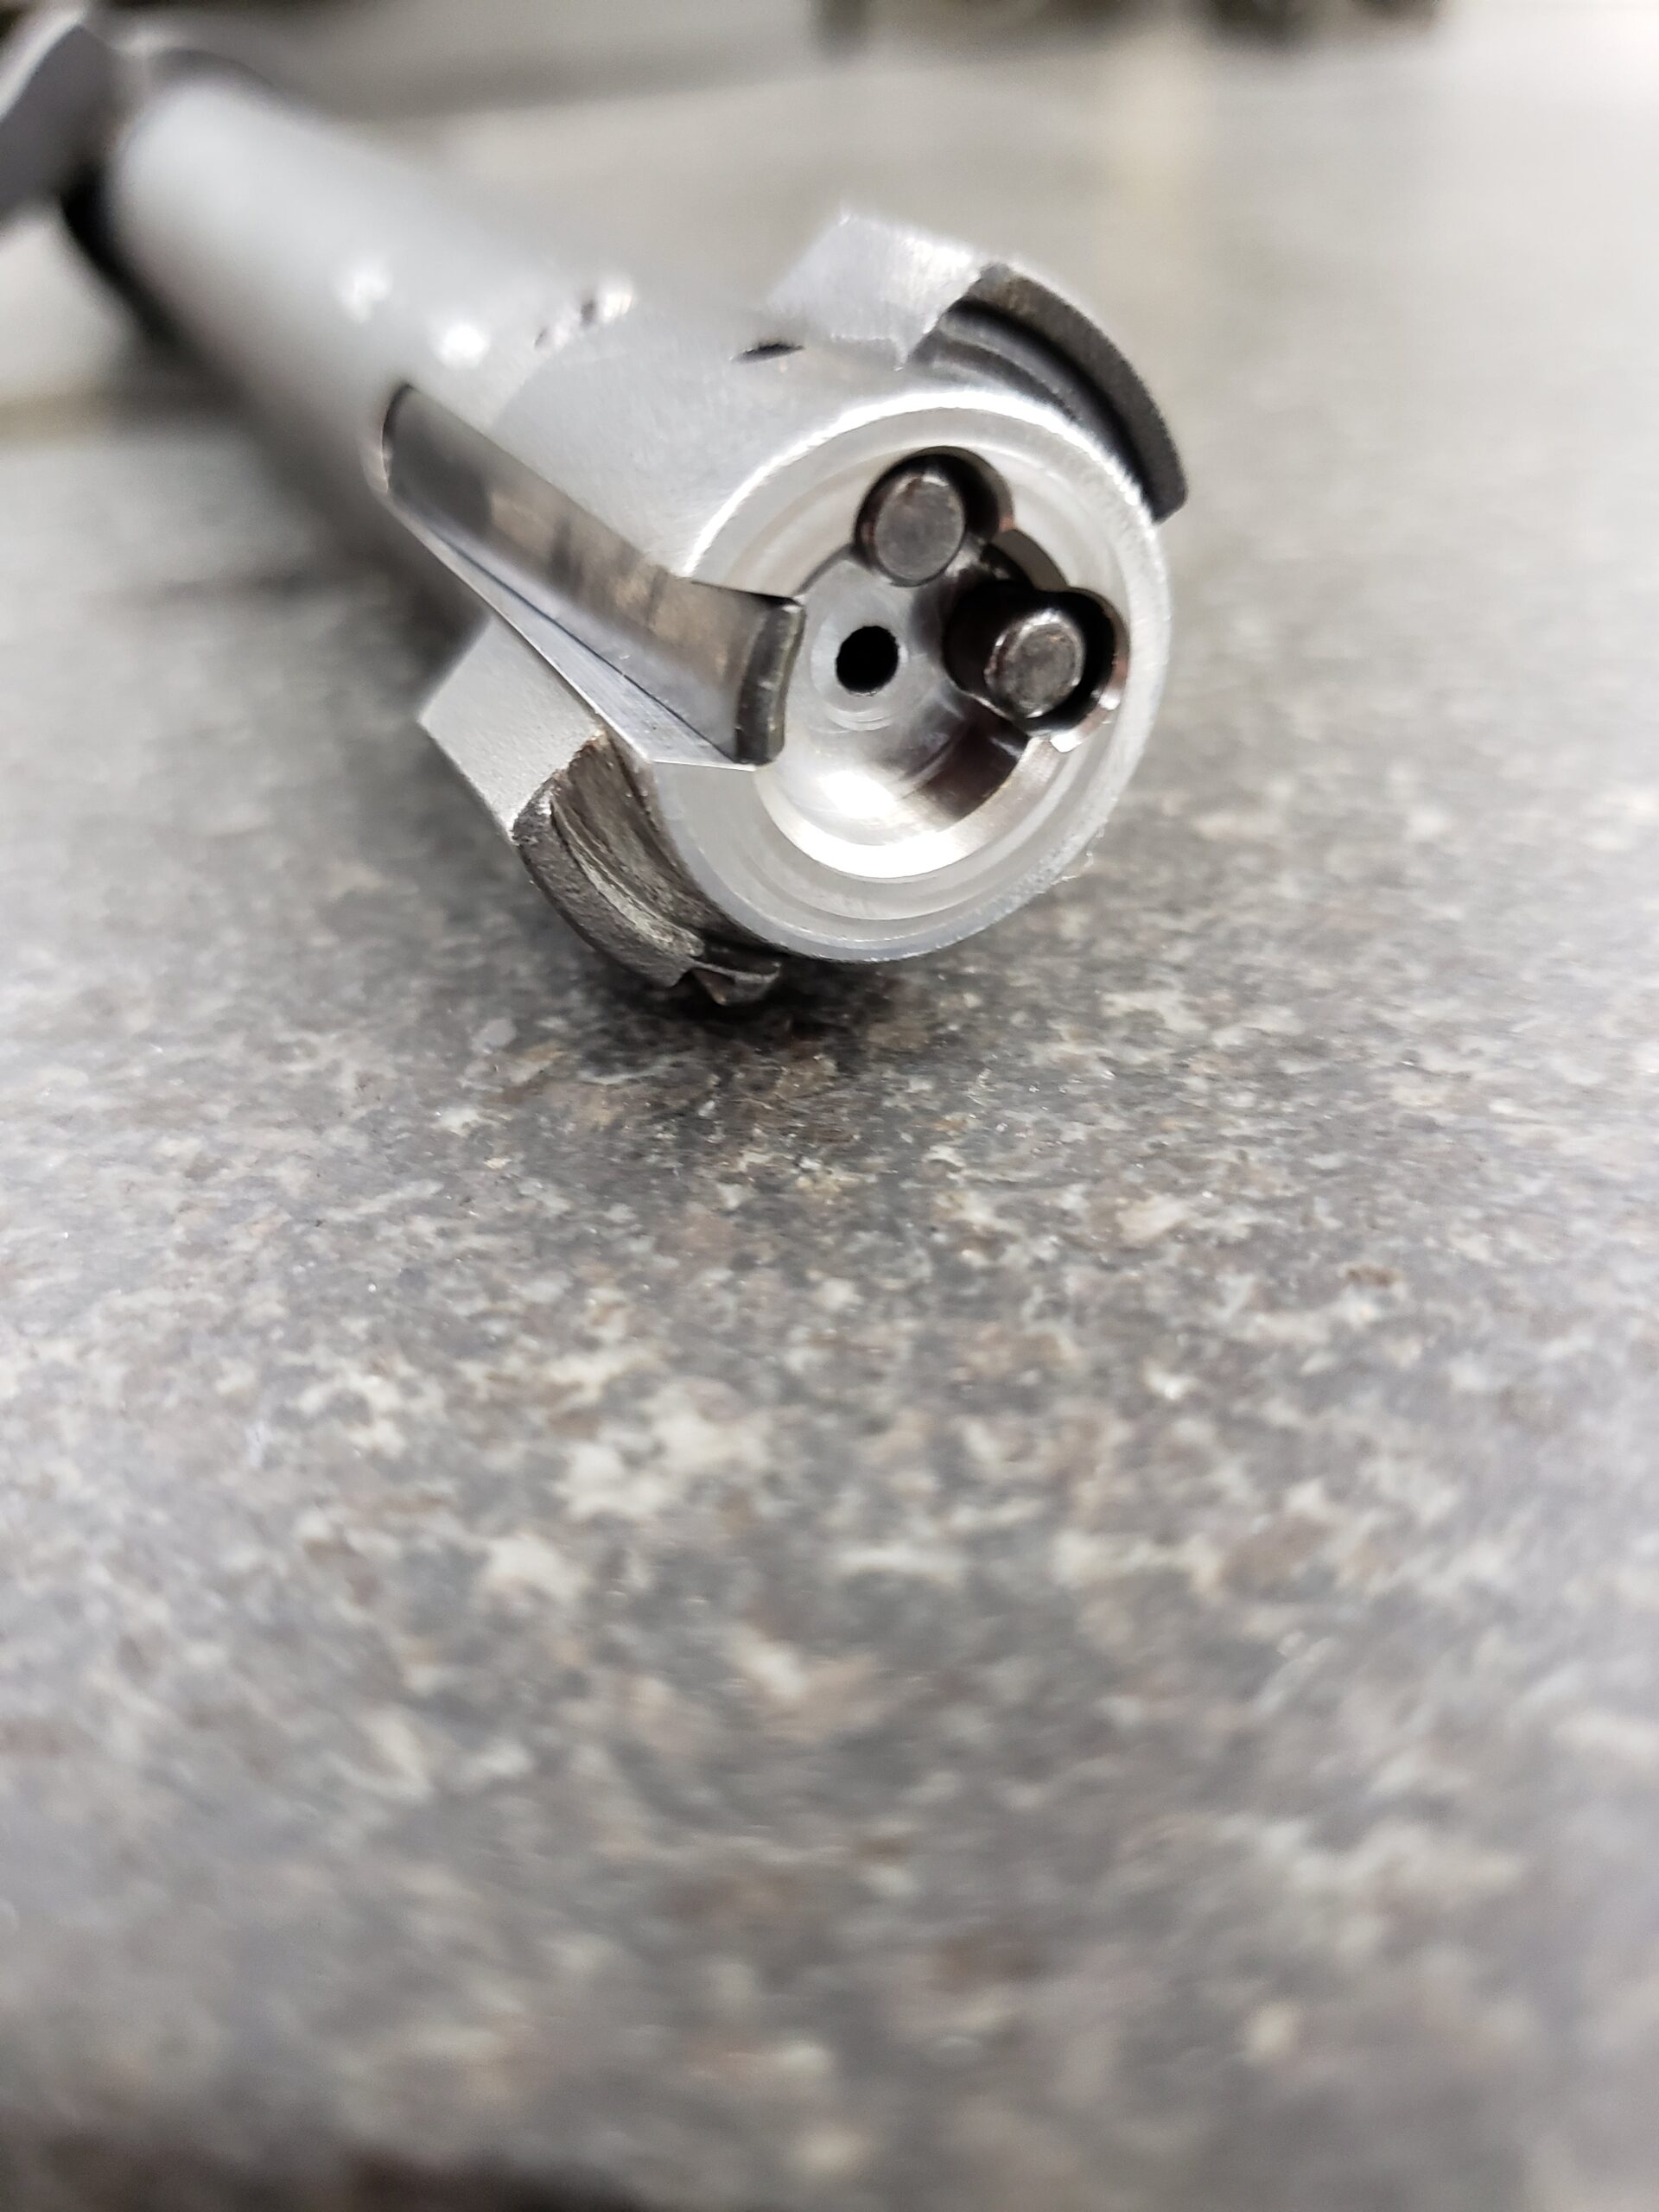
- M16 style extractor upgrade to bolts
- Dual ejector upgrade to bolts fitted with M16 type extractor
- Extractors and Ejectors made in house to ensure compatibility
- Tactical bolt knob installation presents the bolt handle to the spindle at the exact centerline for better presentation
- Tactical bolt knobs installed with a tool steel thread insert instead of threading castings notorious for porosity issues
- M16 extractor bushings threaded to the bolt nose using thread milling and soldered to the bolt face with magnetic induction to create a mechanical bond while avoiding potential damage from an open flame
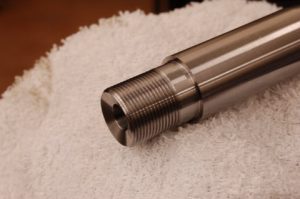
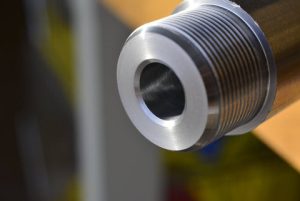
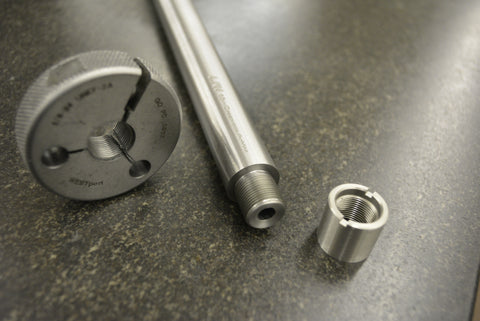
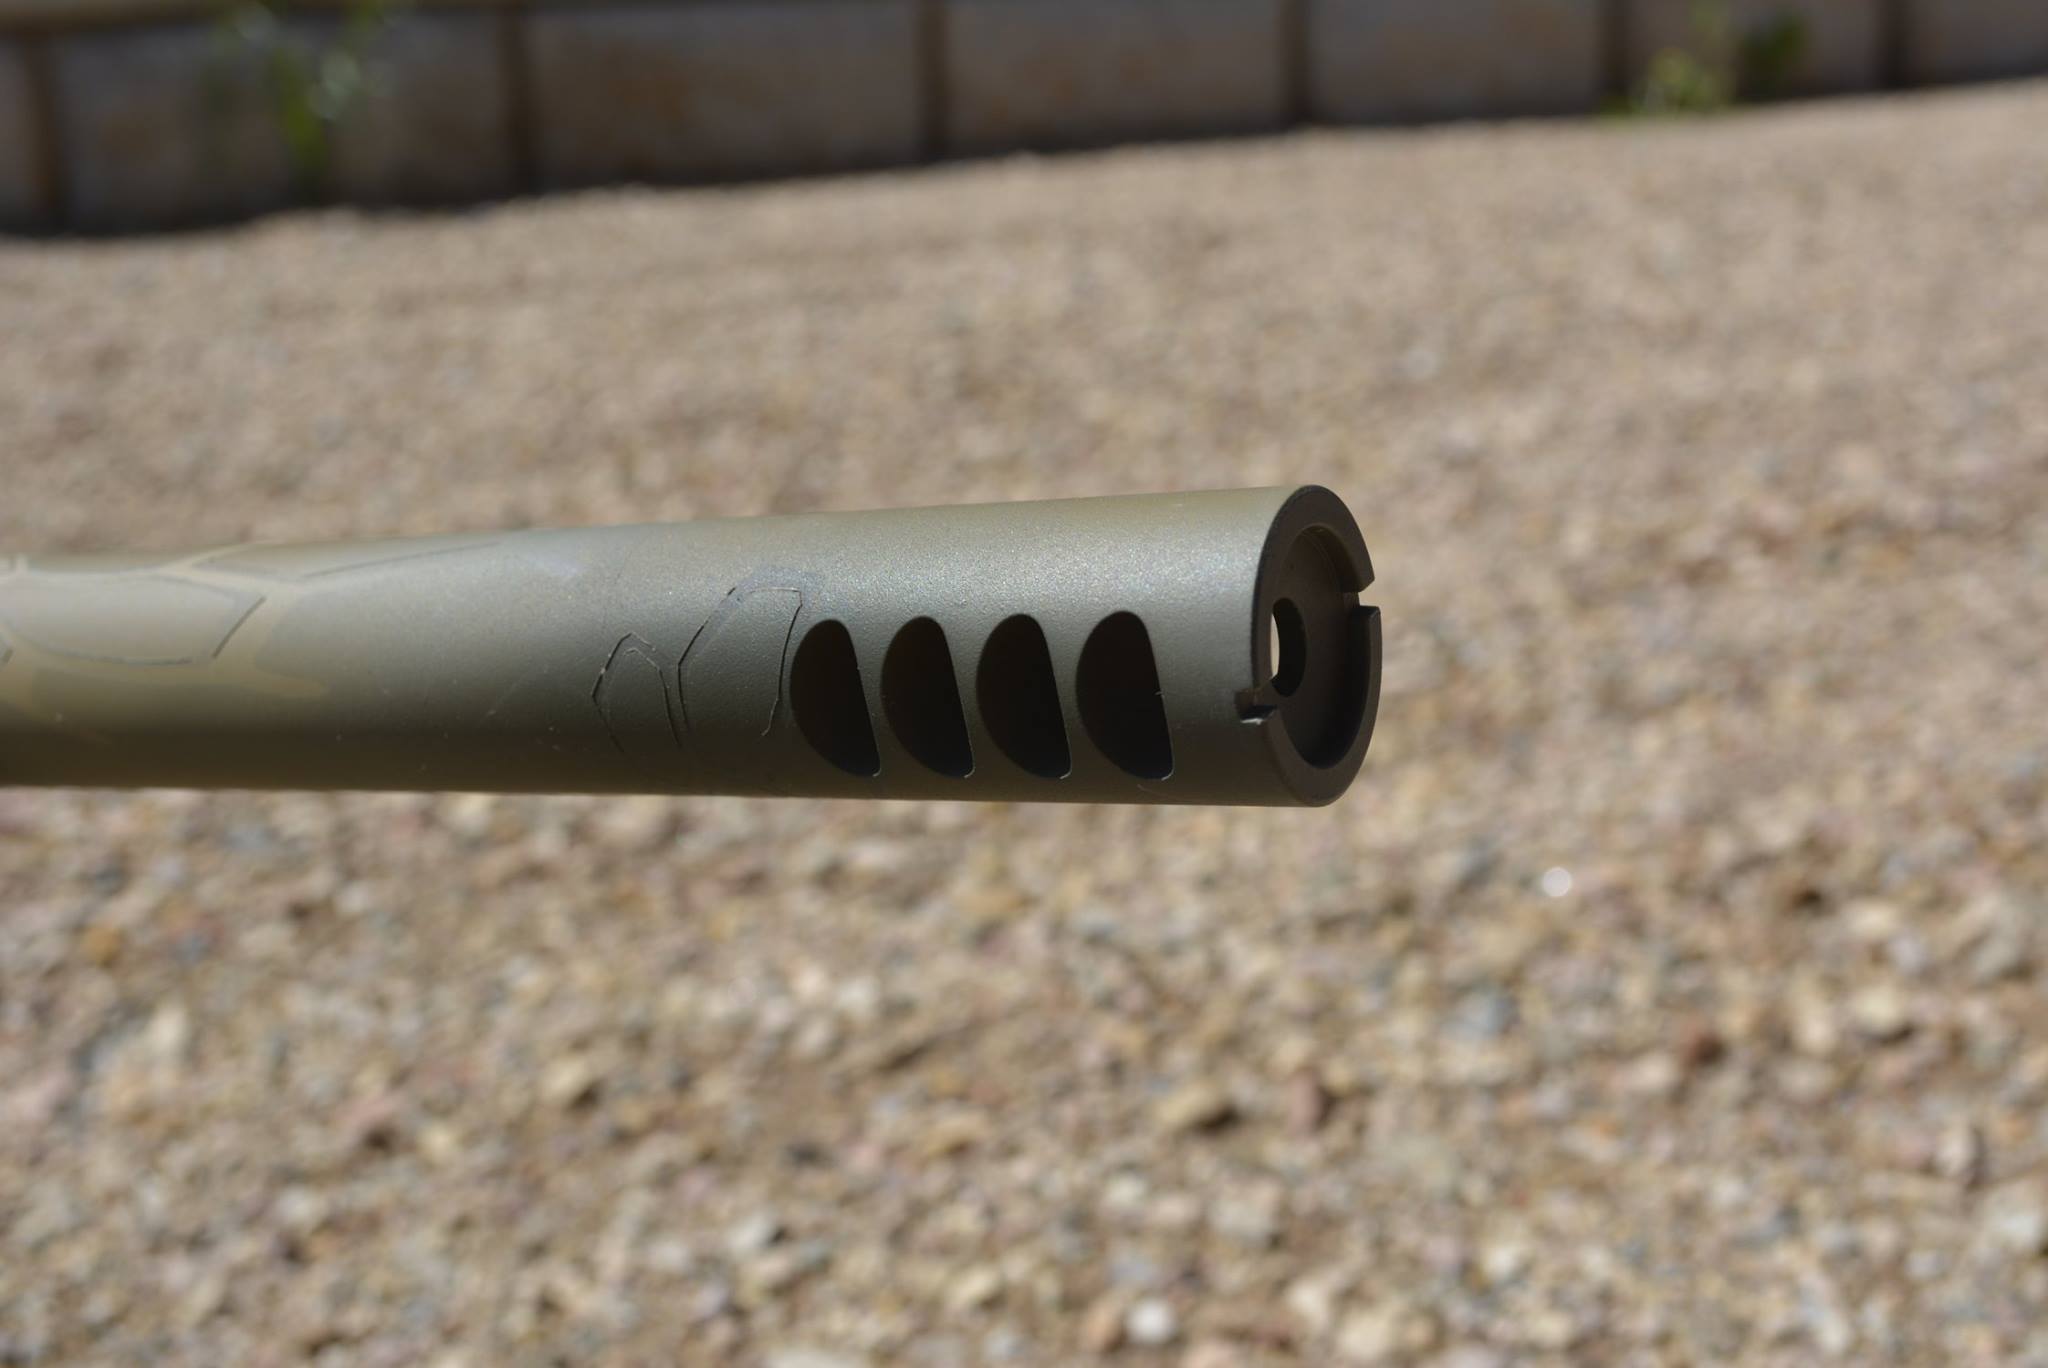
CNC Barrel fitting:
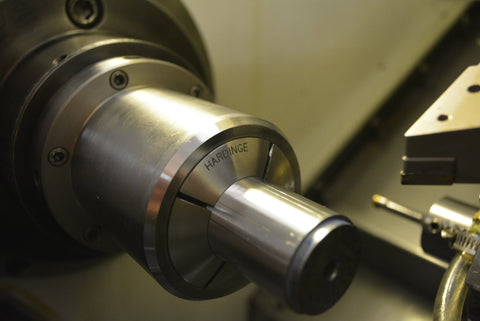
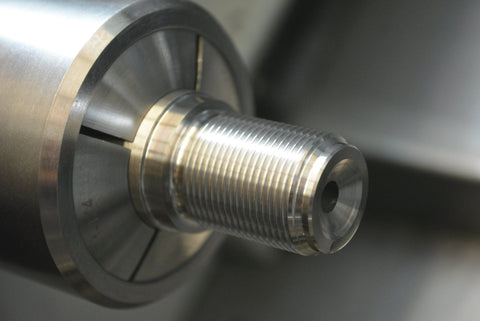
From day one, LRI has fitted barreled actions with the use of a slant bed, CNC turning center. We were one of very few pioneering this process as far back as 2003. A turning center allows for multiple tools to be accessible and presented to the part almost instantly with spindle speed and feedrate calibrated from the tool and material being processed. It all comes together as a barreled action fitted with a higher degree of care.
We have a broad and ever-growing inventory of chamber reamers to fit your needs. As extensive as this is, there will be requests for wildcats outside of our current lineup. We welcome the desire to experiment and improve upon an idea. Just be mindful that it does affect the timeline and cost.
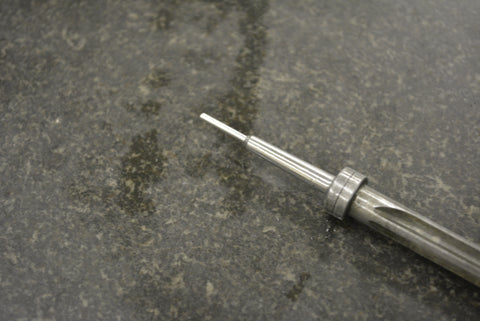
Our chambering reamers are fitted with removable, floating pilots ranging from 17 to 50 caliber. Pilots are made specific to individual manufacturers, tooling material, and pilot styles. Example: A 22-caliber helical flute pilot for a JGS brand carbide reamer has no guarantee to work on the same type of tool made by someone else. If ordering/supplying your own tool, we strongly encourage you to order a set of pilots for your supplied reamer. Bore dimensions on barrels do vary. We have no problem chambering your rifle in a cartridge outside of our inventory. If LRI is ordering you a tool, you are welcome to it afterward, but you will be billed for the cost. LRI will also split the cost of a tool (on a case-by-case basis) with the understanding that the tool/gauging/pilots become the sole property of LRI.
Please note if we are ordering your tool: LRI does not engage in any commerce with Pacific Tool and Gauge (PTG).
Bolt fluting:
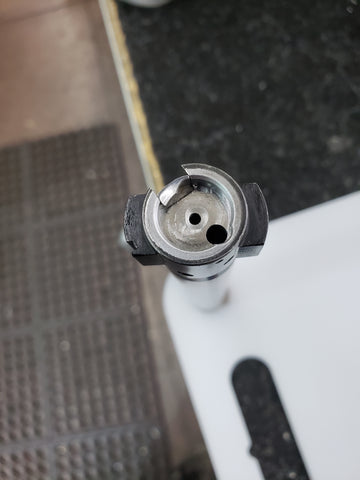
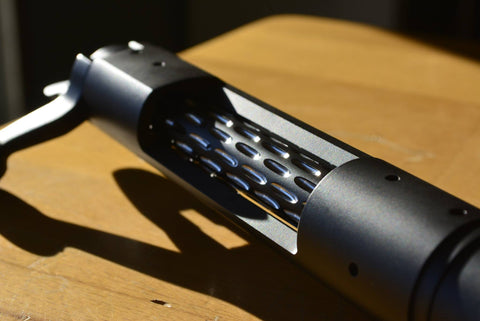
Our full menu of fluting options is available. The purpose for fluting can be summarized into two categories: A slight (very!) reduction in overall weight and cosmetic appeal. Some have argued that fluting a bolt helps as it acts as a sump for dust and grime while in the field. Others say it helps when the rifle is exposed to heavy snow that later turns into ice. LRI does not have any personal experience with either argument.
- Pattern “A” or “B” in Standard or High Helix
- Pattern “A” or “B” in Straight (no helix)
- Pattern “B” Interrupted
- Wrought Iron
- Pattern “A” or “B” Diamond
- Murder Hornet
- Pattern-X
Cerakote application:
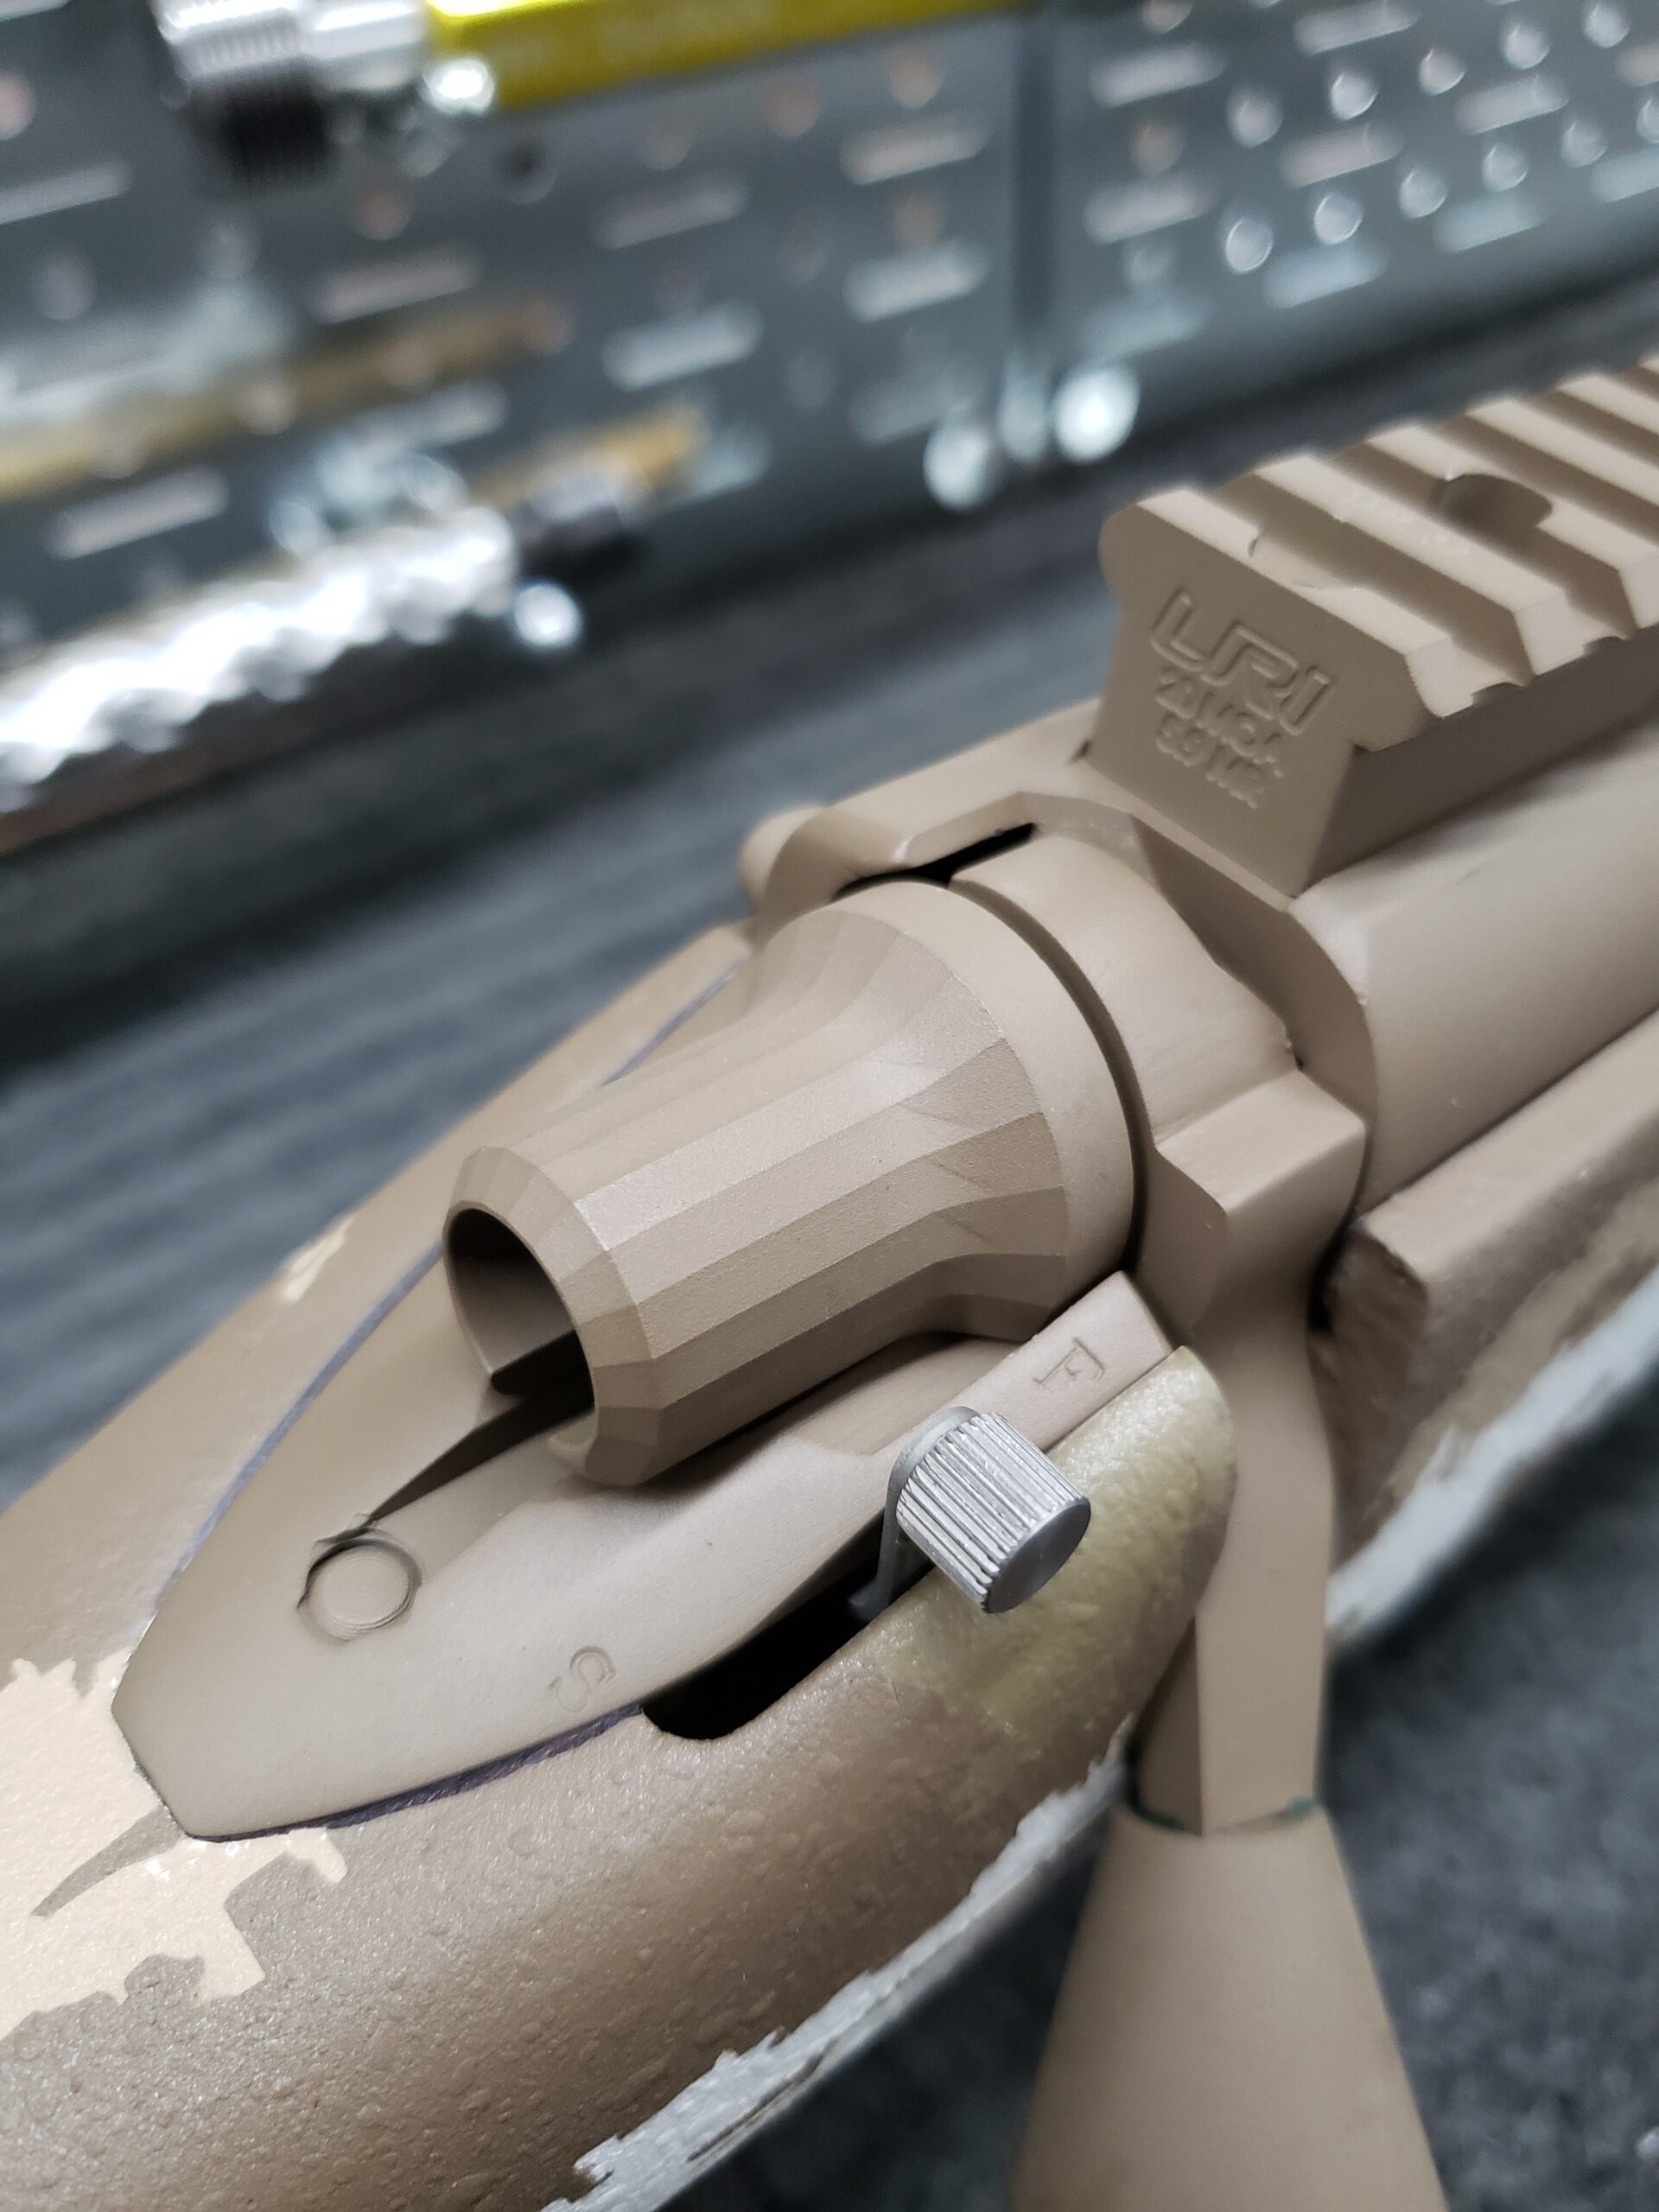
We offer the full line of Oven-Cure (H and E Series) NIC Industries color options for Cerakote. We have a dedicated finish and paint department on site featuring a large envelope oven, walk in paint booth, forced media blasting cabinets, and an extensive library of color options in stock. NIC does an exceptional job of delivering product in a timely manner, so if we do need to order something, it’s here within a couple days.
It’s important to understand that a functional Cerakote job relies on some tribal knowledge. NIC advertises the application at a 1 mil film thickness. While this does work for darker pigments, it’s our experience that the lighter earth tones require a heavier application. This has been a historical problem for many as it is the fertile soil for a gun that just stops working due to parts no longer fitting together. Bolt body and receiver bores being the most commonly problematic. The usual practice is to mask off the receiver’s interior so that the bolt can still function. We chose a different path. A Sunnen precision horizontal honing machine allows us to precisely size and prequalify a bolt action receiver so that the bolt will fit the bore with coating applied to both parts. To the best of our knowledge, we are the only company who does this.
DLC and Salt Bath Nitride:
LRI does not offer DLC or Salt Bath Nitride. These are out to service items that you will have to navigate.
A word of caution regarding Salt Bath Nitride:
OEM Remington bolt bodies are an assembly of 4 components. The head, cross pin, body, and handle are individual pieces assembled by brazing and soldering. Salt Bath Nitride (SBN) is a high temperature process where the part is submerged into a nitrogen/ammonia salt at over 1,000*F. It is very possible (count on it!) for soldered joints to become weakened or damaged by this process. Because SBN is done at a high temperature, it’s also very likely that it will alter the heat treatment of the bolt head. The Remington M700 bolt heads we have tested here on our hardness tester, “dink” at around 48-52 Rockwell C scale. A bolt that has been SBN treated will likely have a surface hardness approaching or exceeding 60 Rockwell. This is great for lubricity and corrosion resistance, but it is a false security because the core material will suffer some annealment as a consequence of the process. It may have the desired hard/slick exterior, but the working part of the bolt (tensile strength) may no longer be what it was originally.
As a policy, LRI does not send Factory bolts or receivers for SBN treatment.
SBN (aka Melonite) treatment on barrels:
This process has been proven to extend the service life of a rifle barrel. The cost benefit is an individual choice as the “all in” price do this correctly is not trivial. For it to work, the barrel must be thoroughly broken in prior to SBN. Failure to do almost always results in a new barrel that copper fouls extensively. This is due to the necessary initial erosion in of the throat on a freshly chambered barrel. SBN increases the surface hardness significantly. This makes the barrel steel much more tolerant to the heat, pressure, and friction that a rifle barrel is exposed to every time its fired. Here, this tolerance works against you because the throat takes longer to wear in so that it’s not peeling away some of the bullet’s jacket material.
We are happy to break the barrel in for you, but you will be billed for the ammunition cost and time involved. It’s a case-by-case basis as ammunition cost varies. Break in is not an accuracy evaluation. We are going to shoot the barreled action into a clearing barrel to wear in the throat.
How all of this works:
Once you have selected your product and service options, simply gather your parts (you may purchase components from us as well) and ship them to us. PLEASE! don’t be afraid to use the notes section, or to call us and ask questions before you send your parts! Once you complete the sale, print a copy of your sales receipt and include it with your parts. If you don’t have convenient access to a printer, all that is required is a brief cover letter with your return address, email, a textable phone number, and the sales receipt number from your order. Once completed, your job will immediately enter our LRI Status Tracker software where you’ll receive routine updates throughout the entire process.
If you are unfamiliar with shipping firearms, please review our “How to ship to LRI” info page for details and pay extra attention to the “cheat codes” for shipping a rifle legally, safely, and securely.
Related products
-
GUNSMITHING SERVICES: Bolt handle skeletonizing for the M700
$150.00 Add to cart -
GUNSMITHING SERVICES: Receiver guard screw restoration/alteration
Price range: $125.00 through $215.00 Select options This product has multiple variants. The options may be chosen on the product page -
GUNSMITHING SERVICES: Pillar bedding on pre-inletted rifle stock
$375.00 Add to cart -
GUNSMITHING SERVICES: 3.9 ULTACH cheek hardware installation
Price range: $175.00 through $375.00 Select options This product has multiple variants. The options may be chosen on the product page